DrSharpe Health
The global landscape of occupational safety and sanitary protection has evolved from a reactive protocol into a foundational element of enterprise risk mitigation. At the center of this transformation lies the deployment of medical-grade barrier technologies, notably Guantes Desechables (disposable gloves) and high-filtration surgical face masks. Global organizations are actively restructuring their sourcing models, moving away from single-source dependencies and prioritizing manufacturers with strong regulatory certifications, production automation, and vertical integration.
Modern sanitary requirements command materials that offer high puncture resistance, chemical inertness, and tactile sensitivity. The market for guantes desechables de nitrilo (disposable nitrile gloves) has experienced exponential growth due to their latex-free composition, which prevents Type I allergic reactions. Parallel to this, advancements in non-woven fabrics have revolutionized mask manufacturing. High-filtration masks depend on electrostatic-charged melt-blown polymers that trap sub-micron viruses and dust particles while maintaining low inhalation resistance.
"Sourcing top-tier protective equipment requires understanding the chemical resistance ratings, thickness metrics, and compliance certificates like EN 455 or ASTM F2100. By integrating both hand protection (guantes desechables) and respiratory protection into a single supply framework, international buyers achieve optimal logistics cost control and consistent regulatory compliance."
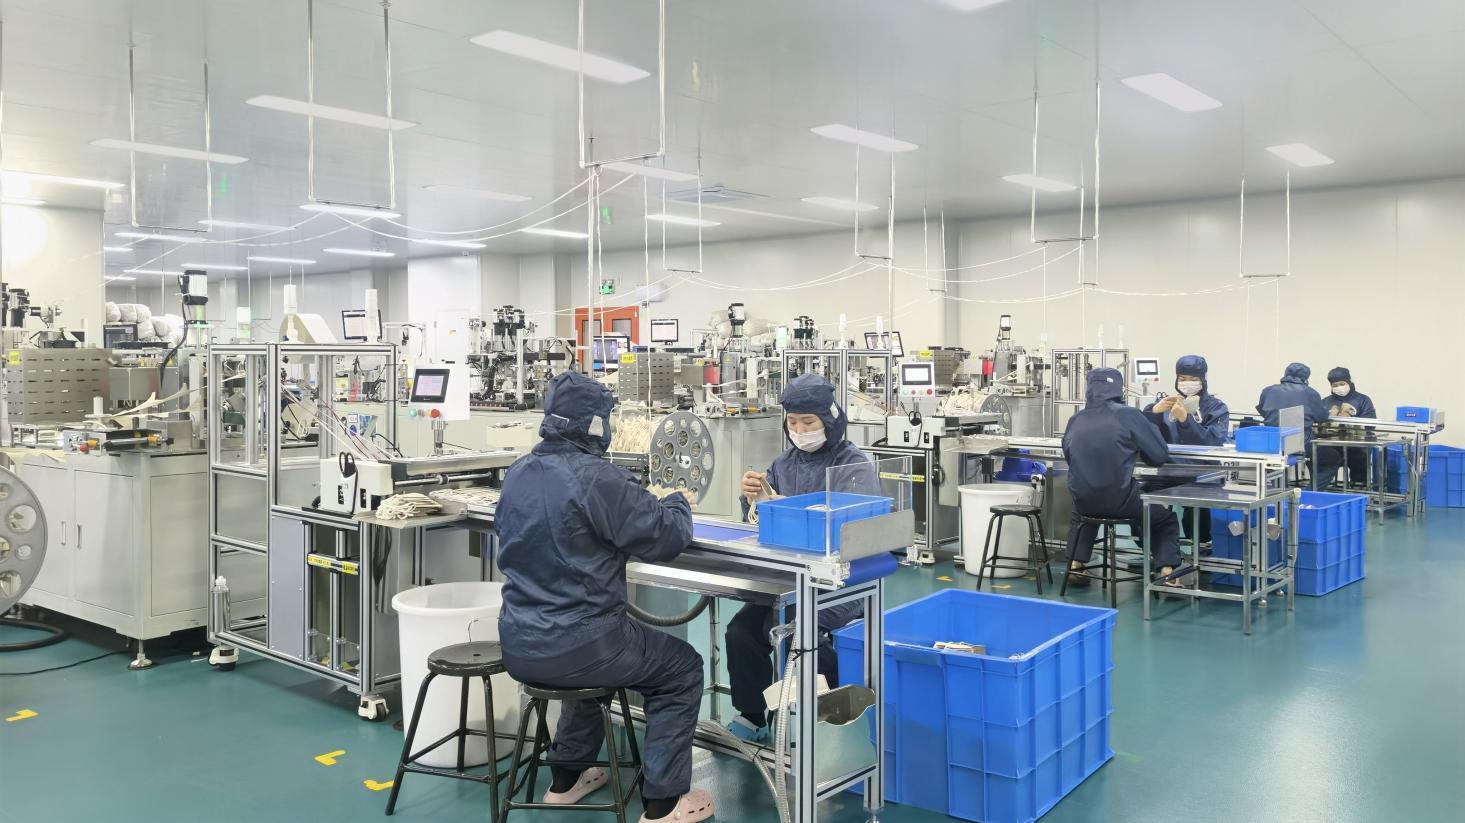
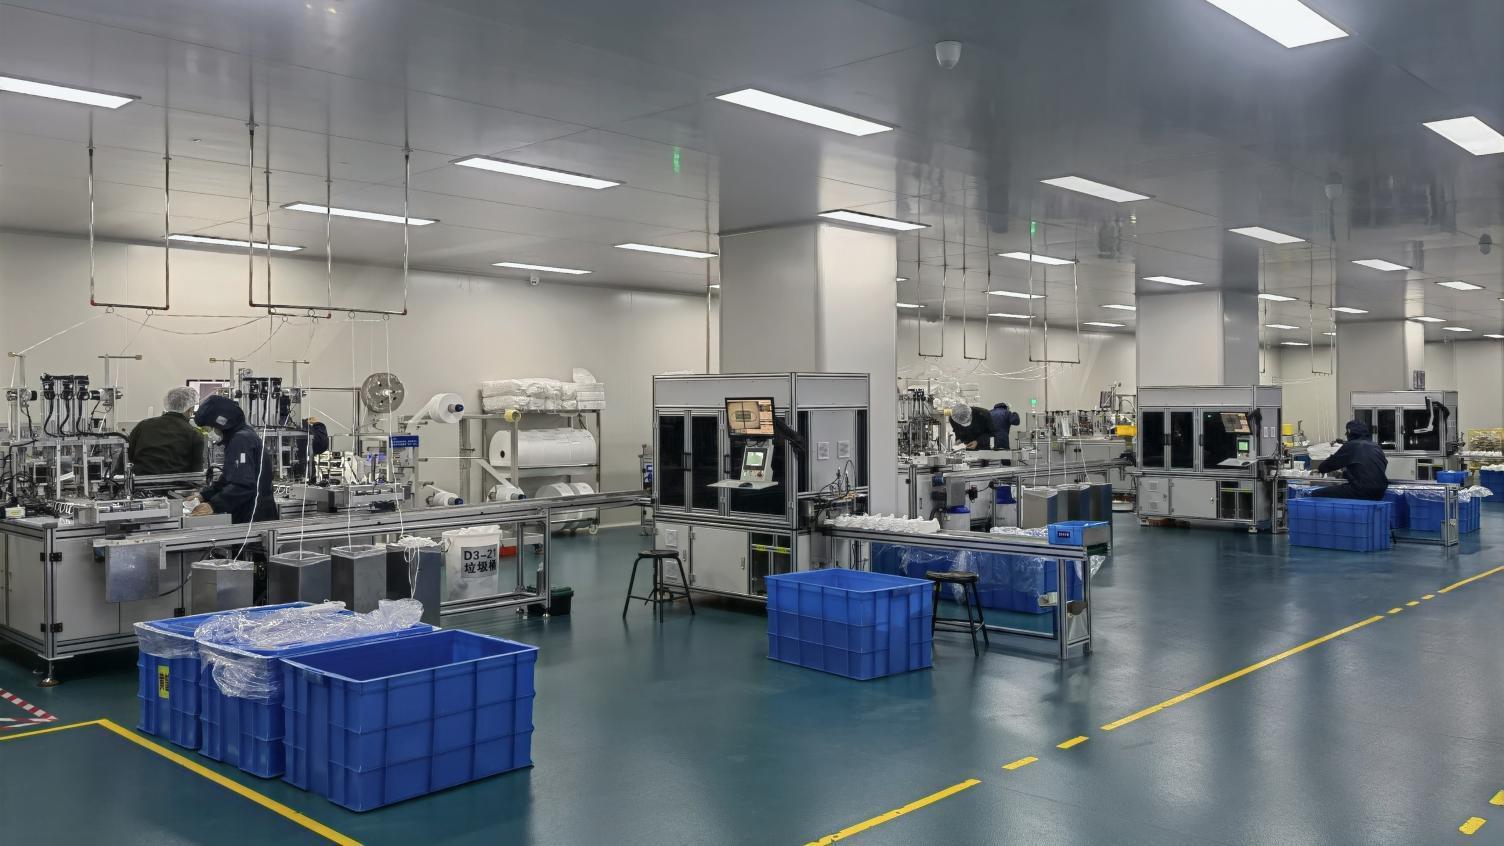
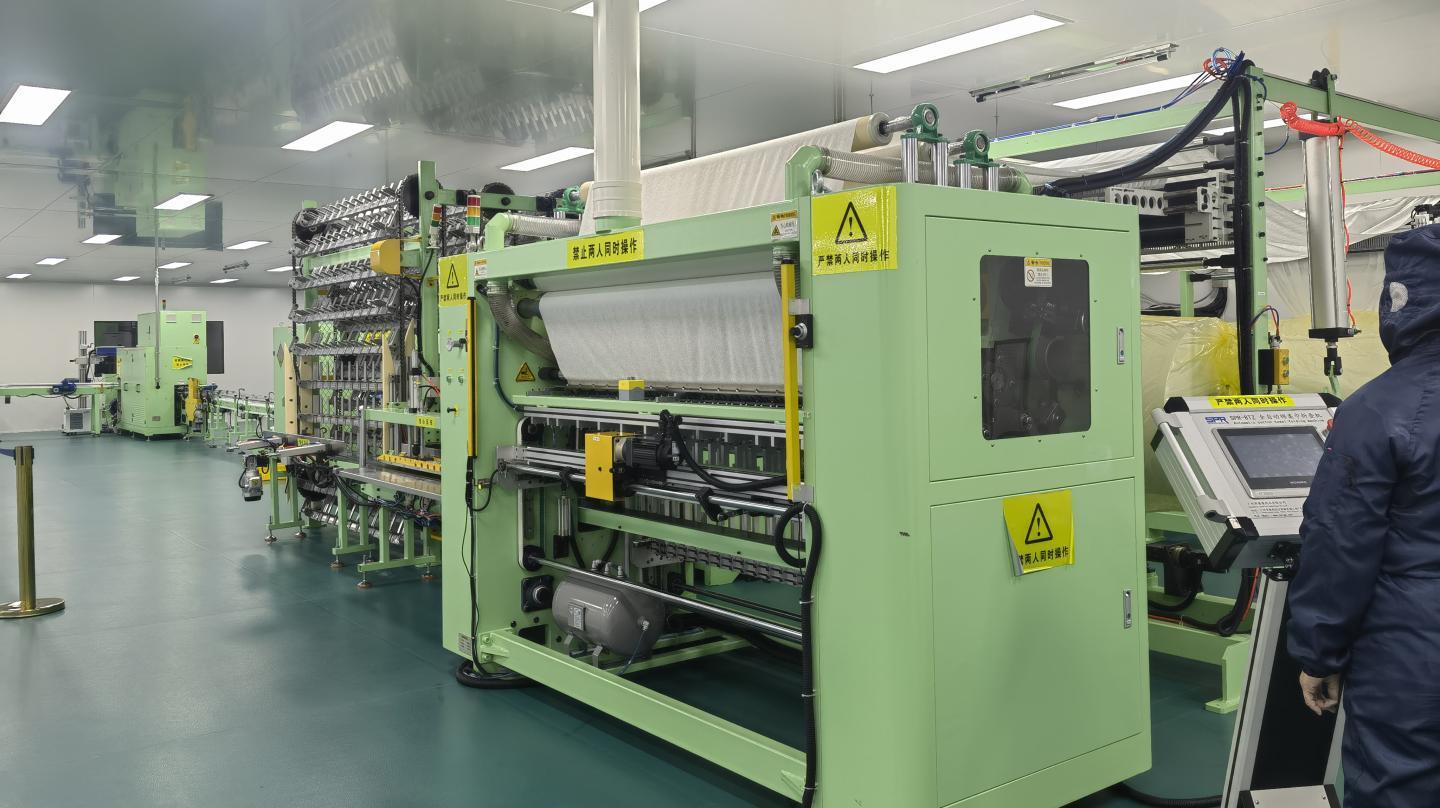
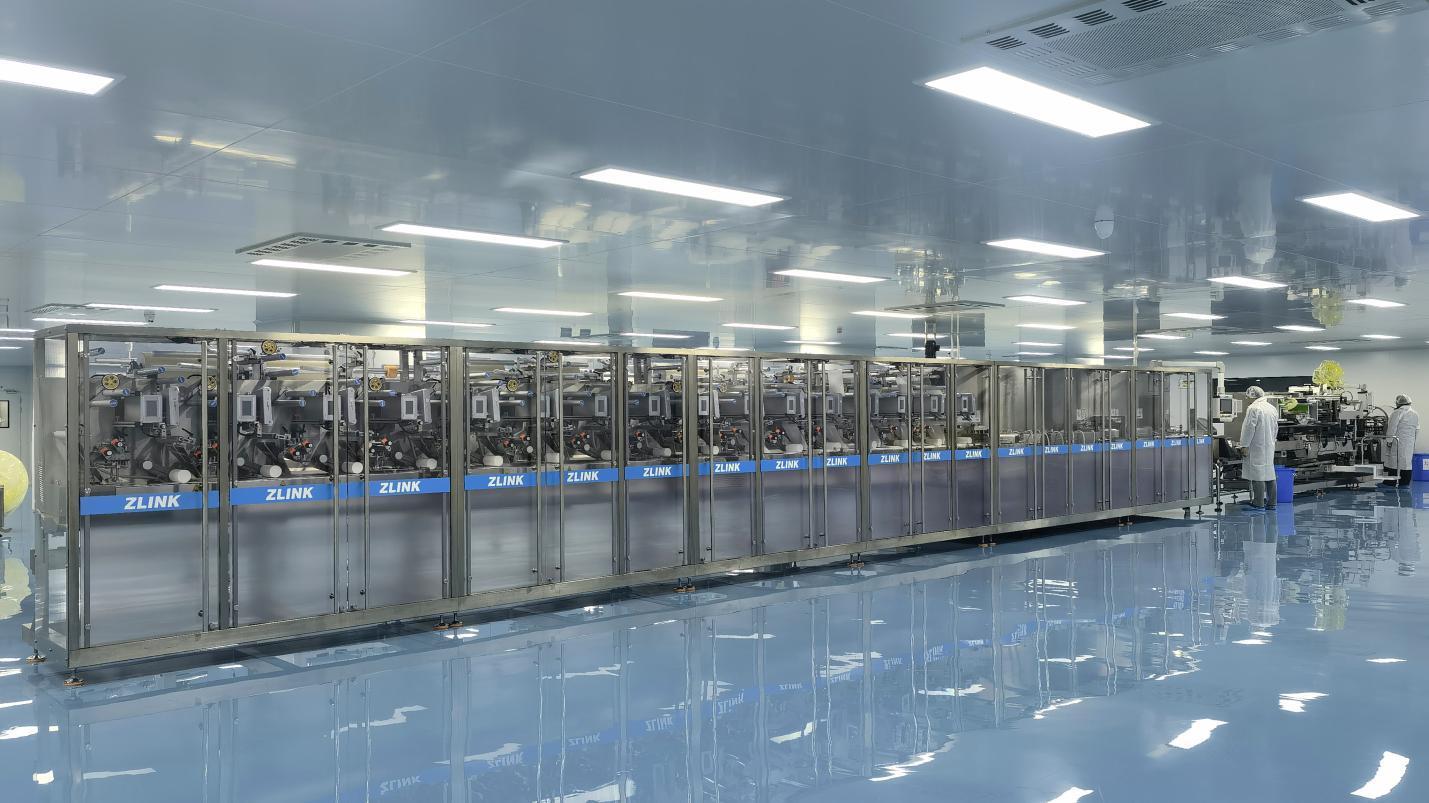
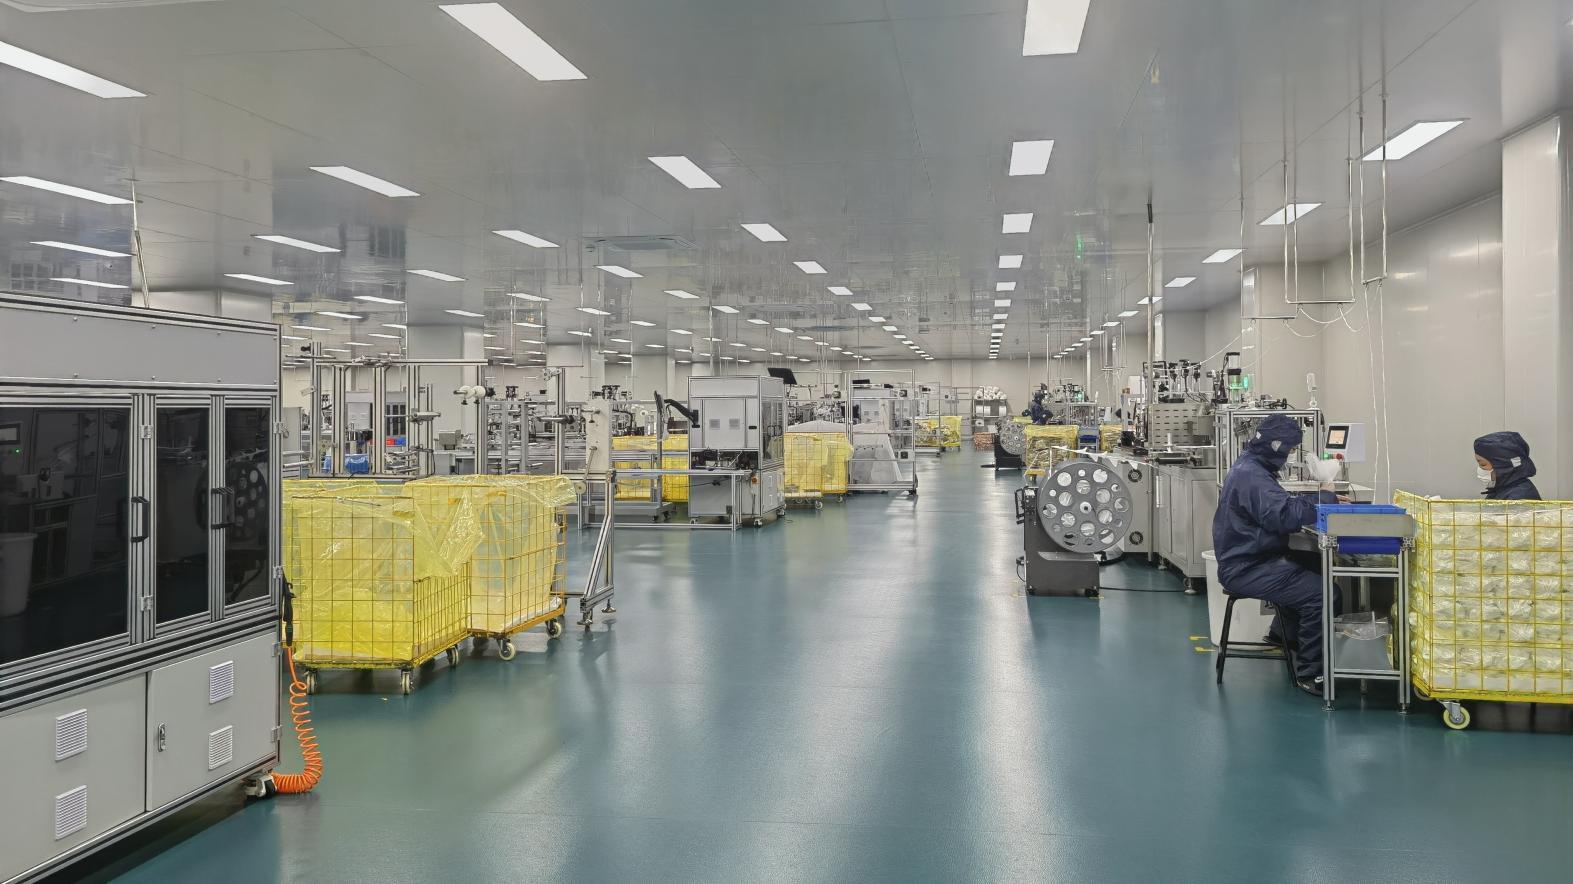
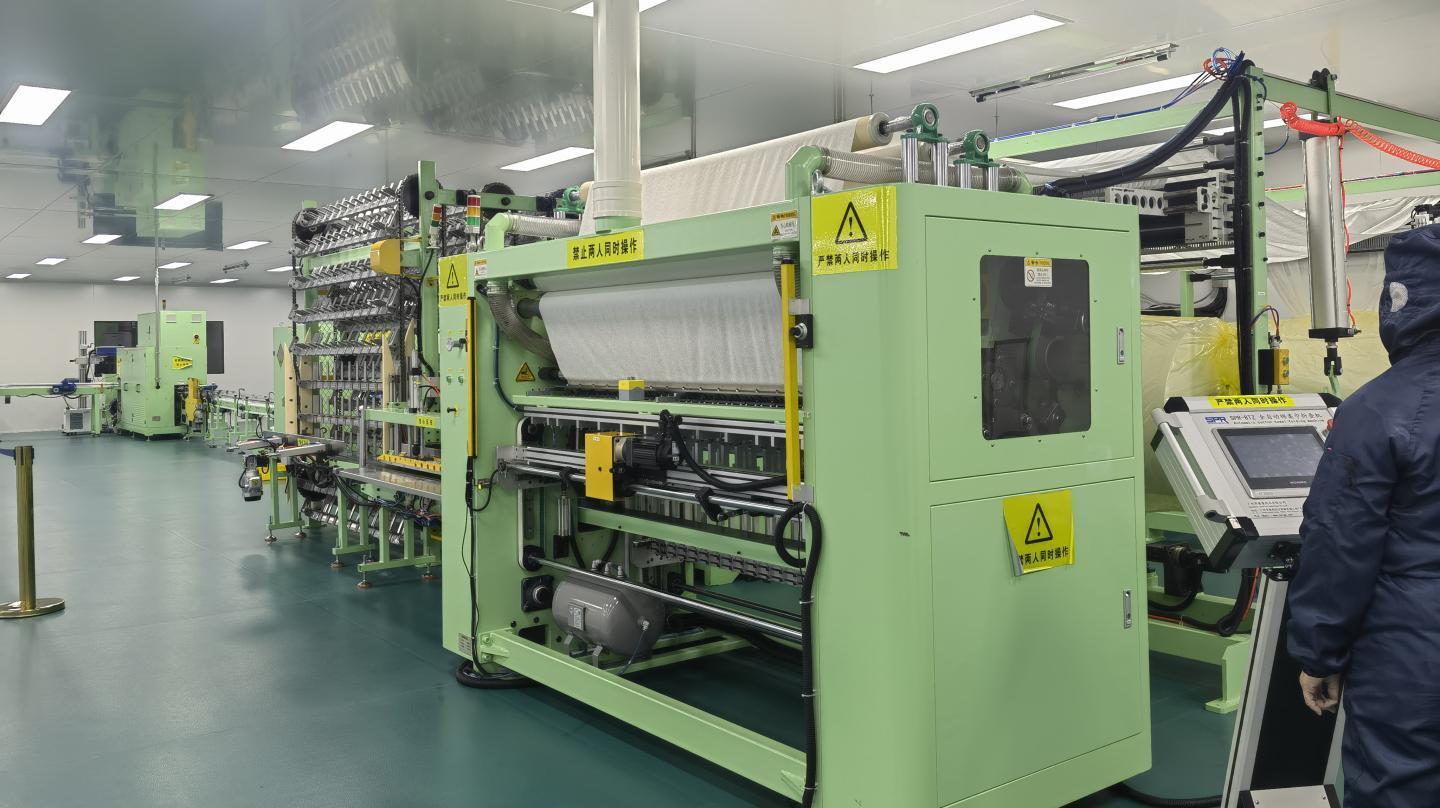
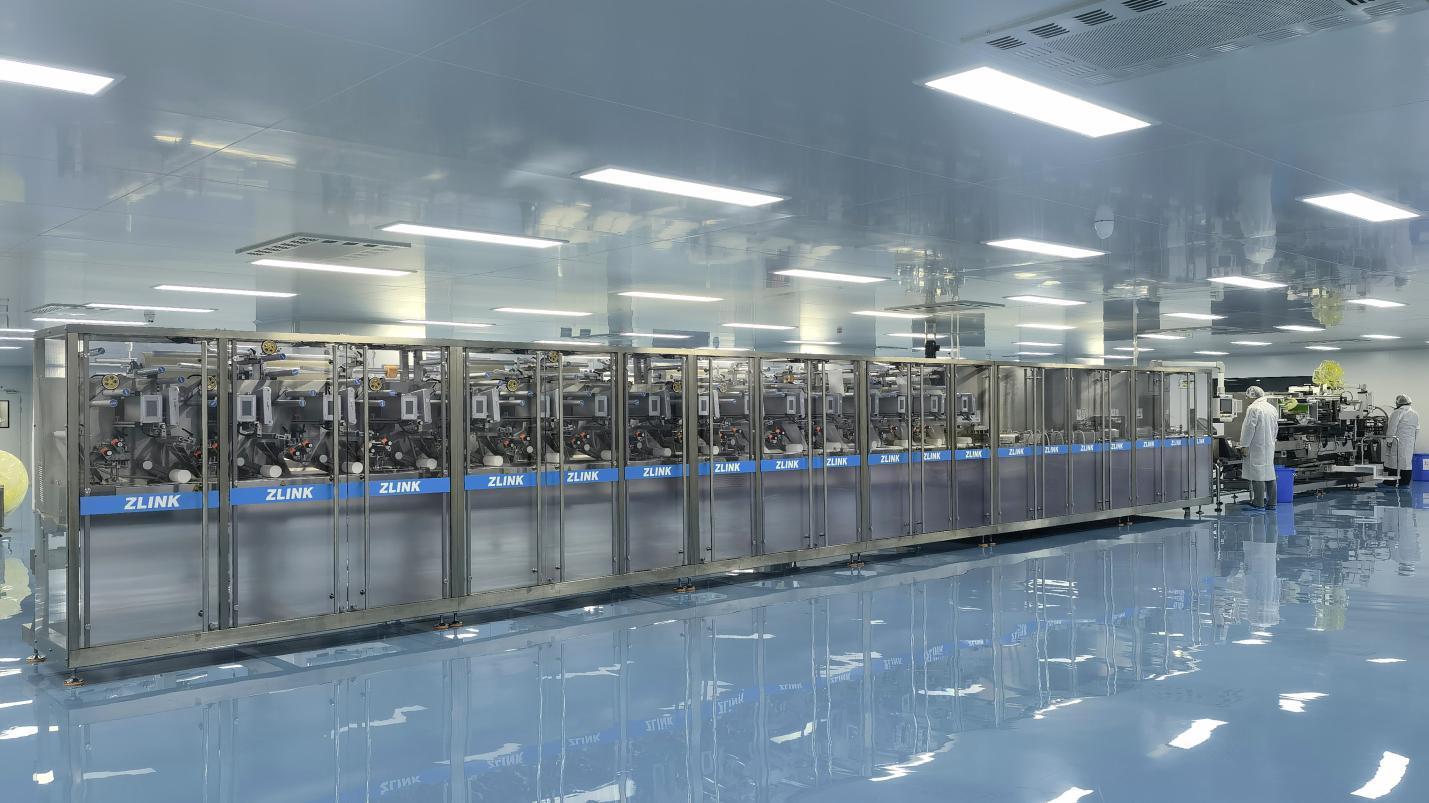
The Chinese manufacturing sector has moved beyond basic cost efficiency. Today, leading facilities like Zhejiang DrSharpe Health Co., Ltd. represent the implementation of Factory 4.0 principles: combining advanced automation, machine learning quality inspection, and structured supply pipelines. With a facility hosting 5 fully automatic mask production lines and 12 semi-automatic production lines, the integration of automation ensures that human contact is minimized, lowering contamination risks and maintaining stable product yields.
This high level of supply control is crucial for global enterprises managing supply fluctuations. In countries like Mexico, Germany, Spain, and the US, where inventory shortages can halt operations, a resilient supplier that guarantees consistent output is a valuable asset.
Zhejiang DrSharpe Health Co., Ltd. is a professional manufacturer and global supplier specializing in disposable medical and healthcare products, especially high-quality face masks and protective solutions. With strong manufacturing capabilities, advanced production technology, and strict quality management, DrSharpe is committed to providing safe, reliable, and comfortable healthcare products for customers worldwide.
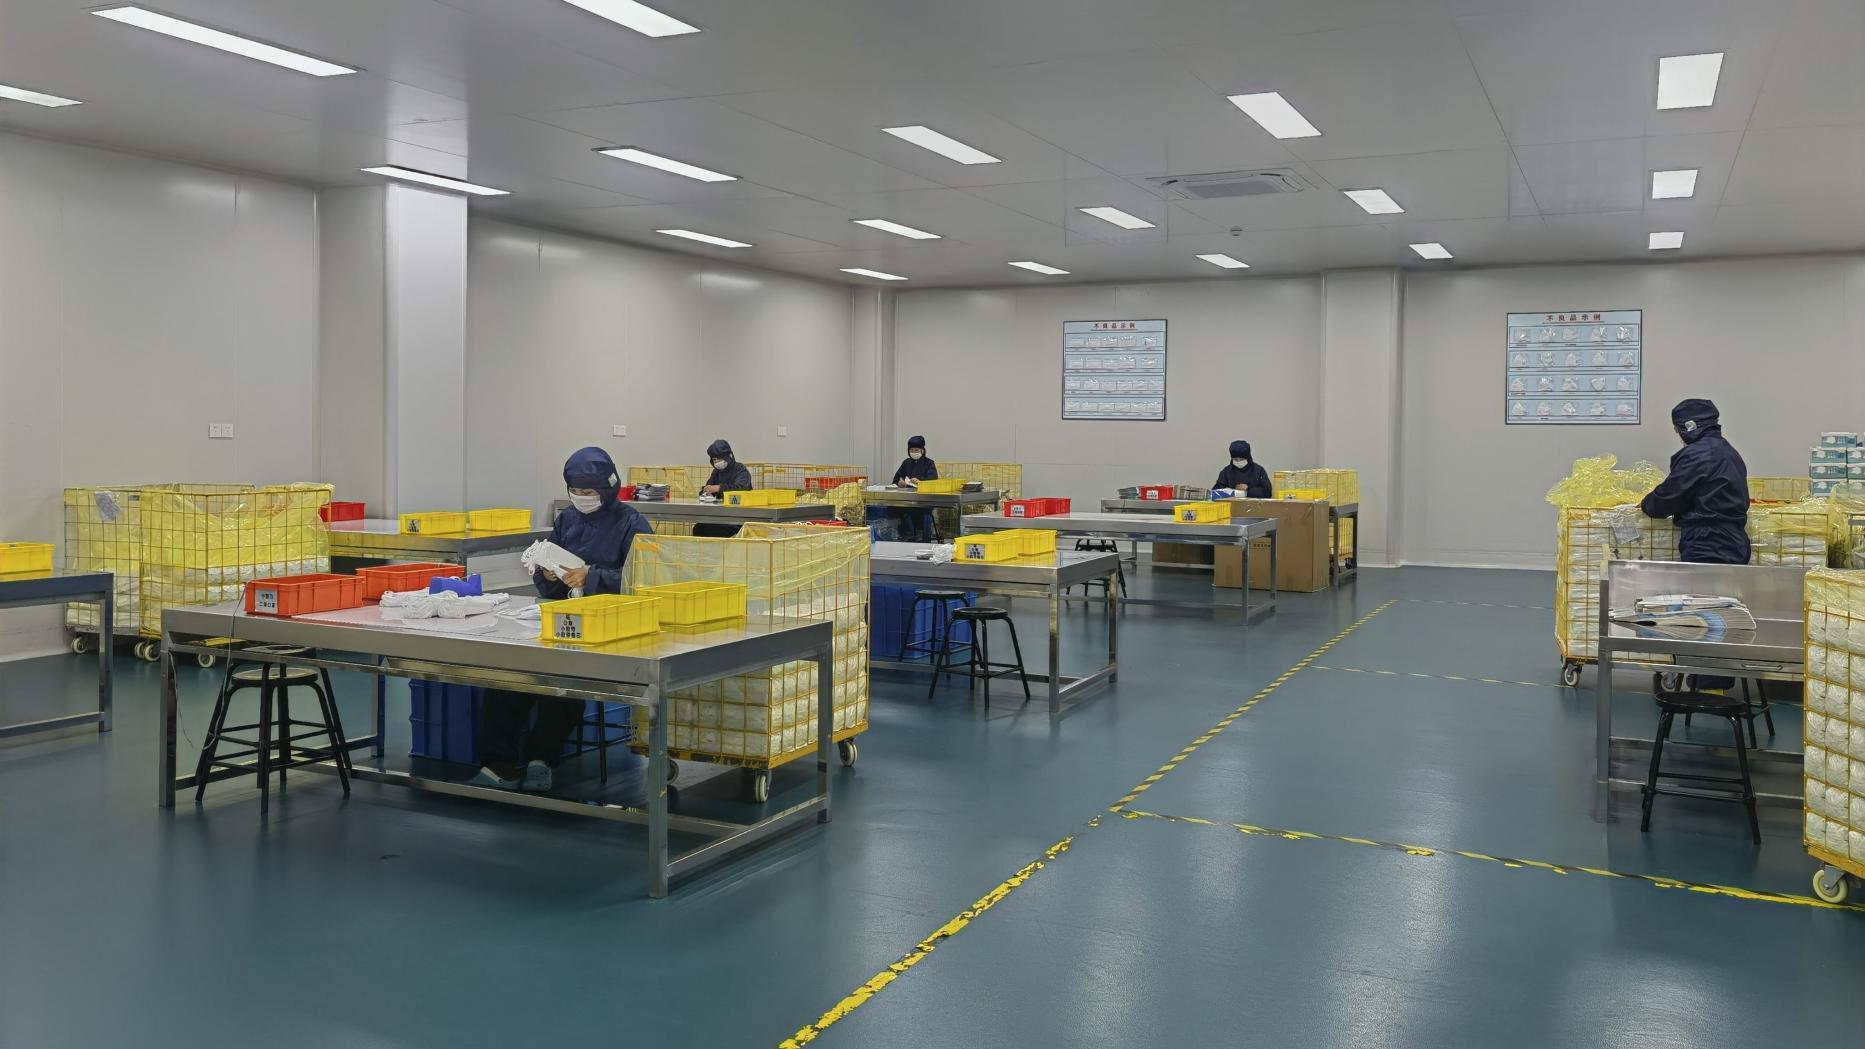
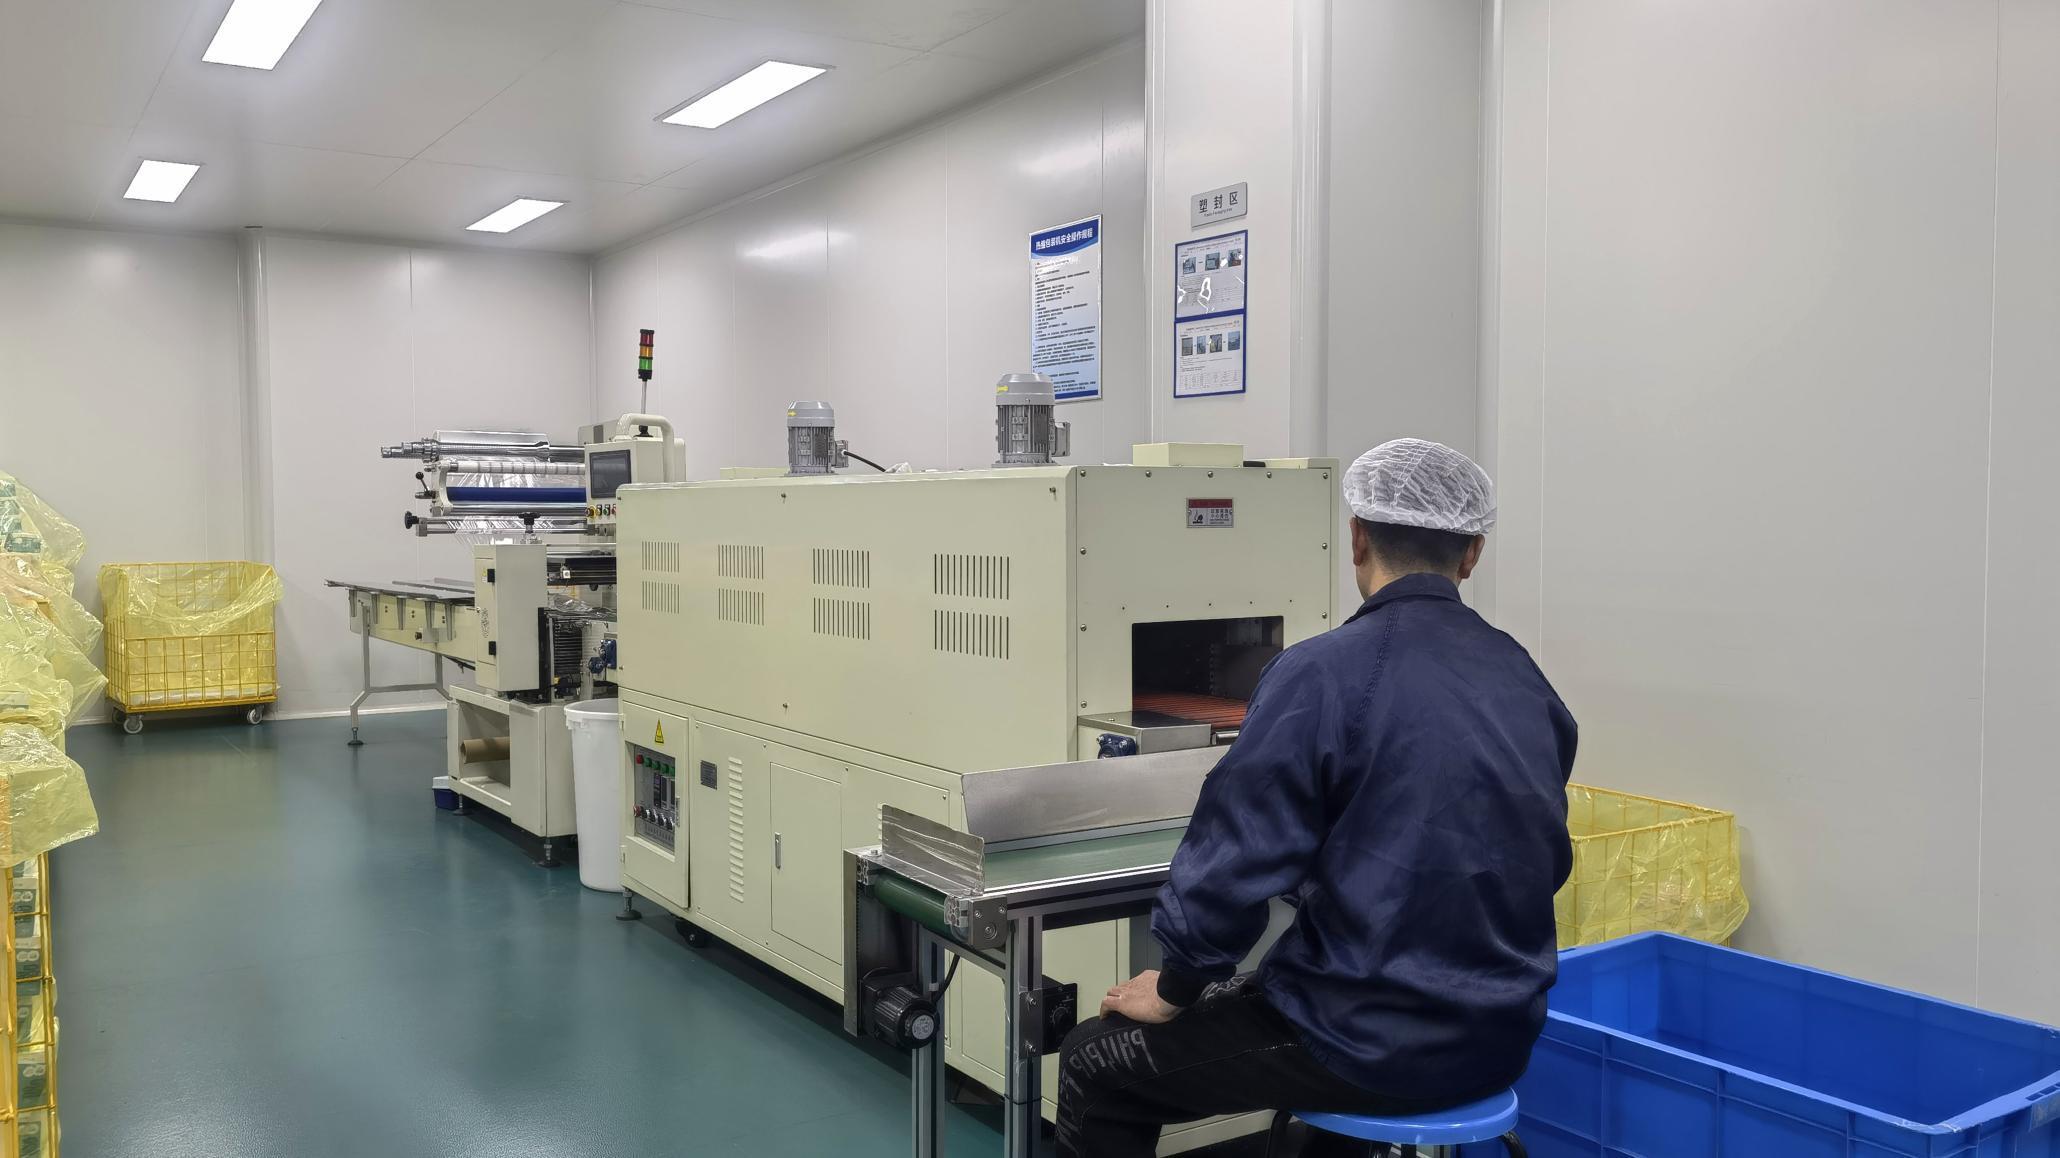
Our factory is equipped with 5 fully automatic mask production machines and 12 semi-automatic mask production machines, supported by an experienced production and service team. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to markets including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
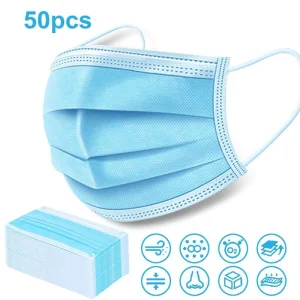
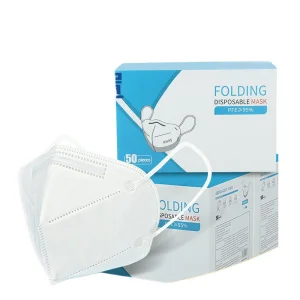
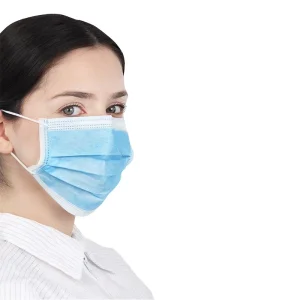
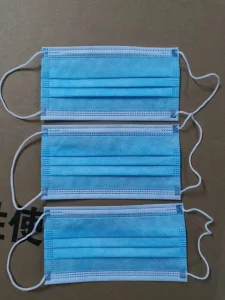
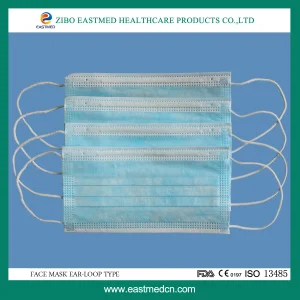
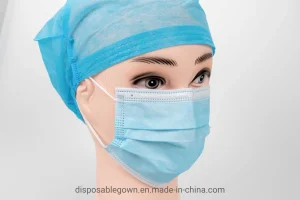
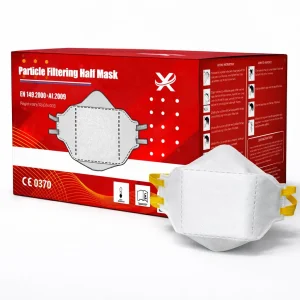
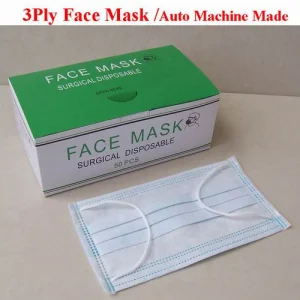
DrSharpe mainly provides disposable face masks and related healthcare products for medical, personal protection, and daily use applications. Using advanced filtration materials, our masks achieve up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE), offering excellent protection and wearing comfort. Our products comply with international standards and have obtained certifications including CE, US FDA, and US EUA.
Driven by innovation, quality, and customer satisfaction, Zhejiang DrSharpe Health Co., Ltd. continues to deliver trusted healthcare solutions and build long-term partnerships with customers around the world.
Industrial buyers must look past base price points and analyze the Total Cost of Ownership (TCO). In industries like food processing, semiconductor packaging, clinical healthcare, and chemicals, product failures lead to contamination, shut-downs, or health liabilities.
Require CE / FDA validated barriers with a high BFE (99%) and skin-safe, powder-free attributes for patient care.
Demands FDA-approved food contact materials, high chemical resistance, and high tensile strength to prevent tears during operation.
Demands low-dust and anti-static surfaces to protect sensitive components during assembly processes.
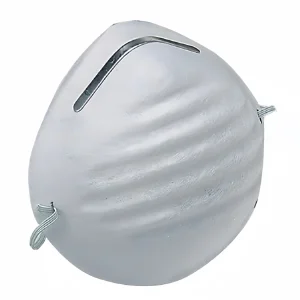
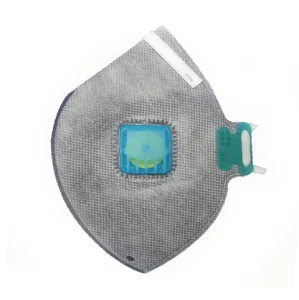
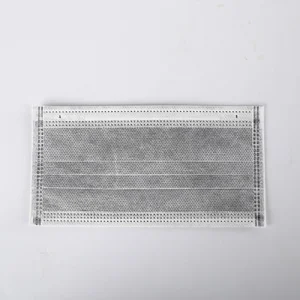
Prioritizes multi-ply active carbon filters (like N95 active carbon masks) and durable barrier materials to protect against chemical exposure.
Our customized OEM solutions are engineered to meet these demands, offering tailormade thickness levels, packaging counts, and material weights to fit specific localized application scenarios.
For the US market, products need FDA registration, 510(k) approval for medical-grade items, or EUA list adherence. For Europe, CE certification (EN 14683 for surgical masks and EN 455 / EN 374 for disposable gloves/guantes desechables) is required. Our facilities carry verified CE and US FDA registrations, ensuring smooth customs processing.
BFE (Bacterial Filtration Efficiency) measures the percentage of bacteria (typically sized around 3.0 microns) filtered out by the mask. PFE (Particle Filtration Efficiency) measures the filtration of smaller sub-micron particles (often around 0.1 microns). Our premium masks offer 99% ratings for both BFE and PFE, meeting the standards for surgical and critical care environments.
Yes. We provide complete OEM support, covering custom packaging, inner box designs, and print specifications on the outer carton. This allows clients in medical, retail, or industrial sectors to maintain consistent branding.
Automation reduces assembly variation, minimizes contaminant exposure, and increases throughput. With 5 fully automatic and 12 semi-automatic lines, we can process large volume orders on tight schedules while maintaining a stable defect rate close to zero.
When stored in a dry environment between 15°C and 30°C, away from direct sunlight and dust, high-quality non-woven products and medical-grade protective gloves maintain their filtration and physical barrier properties for up to 3 to 5 years.