 DrSharpe Health
Direct from certified manufacturing facilities, integrating multi-layer non-woven barrier materials.
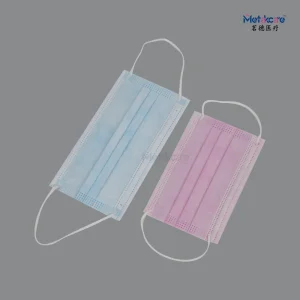
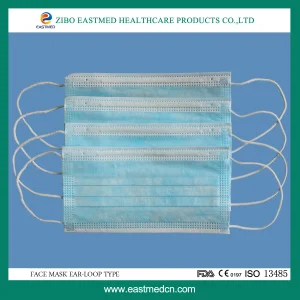
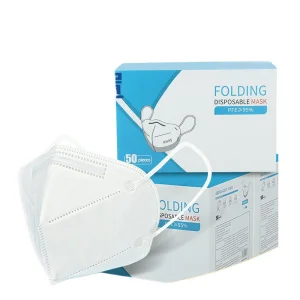
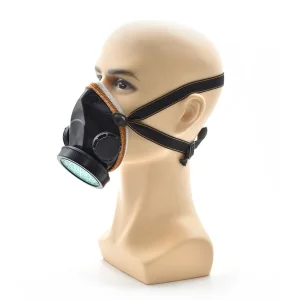
Across the globe, safety standards for workers in hazard-prone environments have risen significantly over the past decade. The demand for overoles de protección (protective coveralls) has shifted from basic general-purpose wear to high-performance, specialized, multi-barrier protection garments. Rapid industrialization, chemical refining expansions, strict biological safety requirements, and stringent environmental regulations have driven safety procurement managers to prioritize compliance and quality above all.
In Latin America, particularly in nations like Mexico, Chile, Peru, and Colombia, key industrial sectors such as mining, petrochemicals, automotive spray painting, and agriculture rely heavily on high-quality PPE. These environments expose workers to volatile chemical splashes, harmful fine particulates, and infectious bio-aerosols. Consequently, the sourcing of protective wear has expanded from domestic distributors directly to high-capacity Chinese manufacturing plants capable of producing under strict European Standard (EN) classes and American (ANSI) regulations.
Designed for strong jet liquid chemical protection. Crucial for petrochemical cleaning and industrial solvent handling.
Resistant to dry hazardous dust and minor chemical splashes. Perfect for paint booths, fiberglass handling, and construction.
Conforming to EN 1149 for electrostatic dissipation and EN 14126 for biological infectious agents defense.
China’s dominance in the non-woven textiles and protective apparel sector is backed by unmatched vertical supply chain integration. From petrochemical derivatives to advanced spunbond-meltblown-spunbond (SMS) composite fabrics, every step of the raw material pipeline is located within close geographic proximity. This reduces domestic transport costs and speeds up turnaround times.
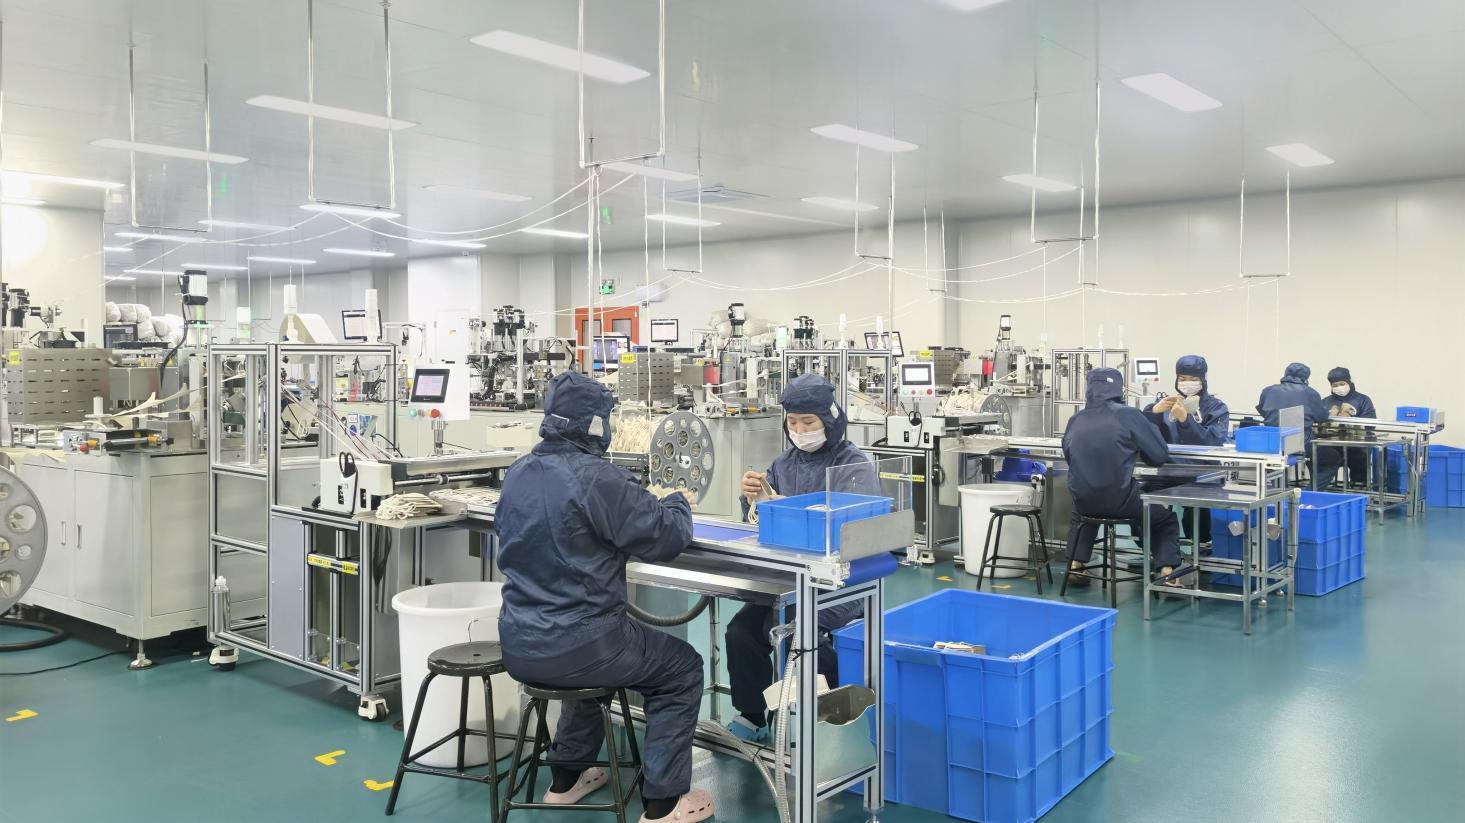
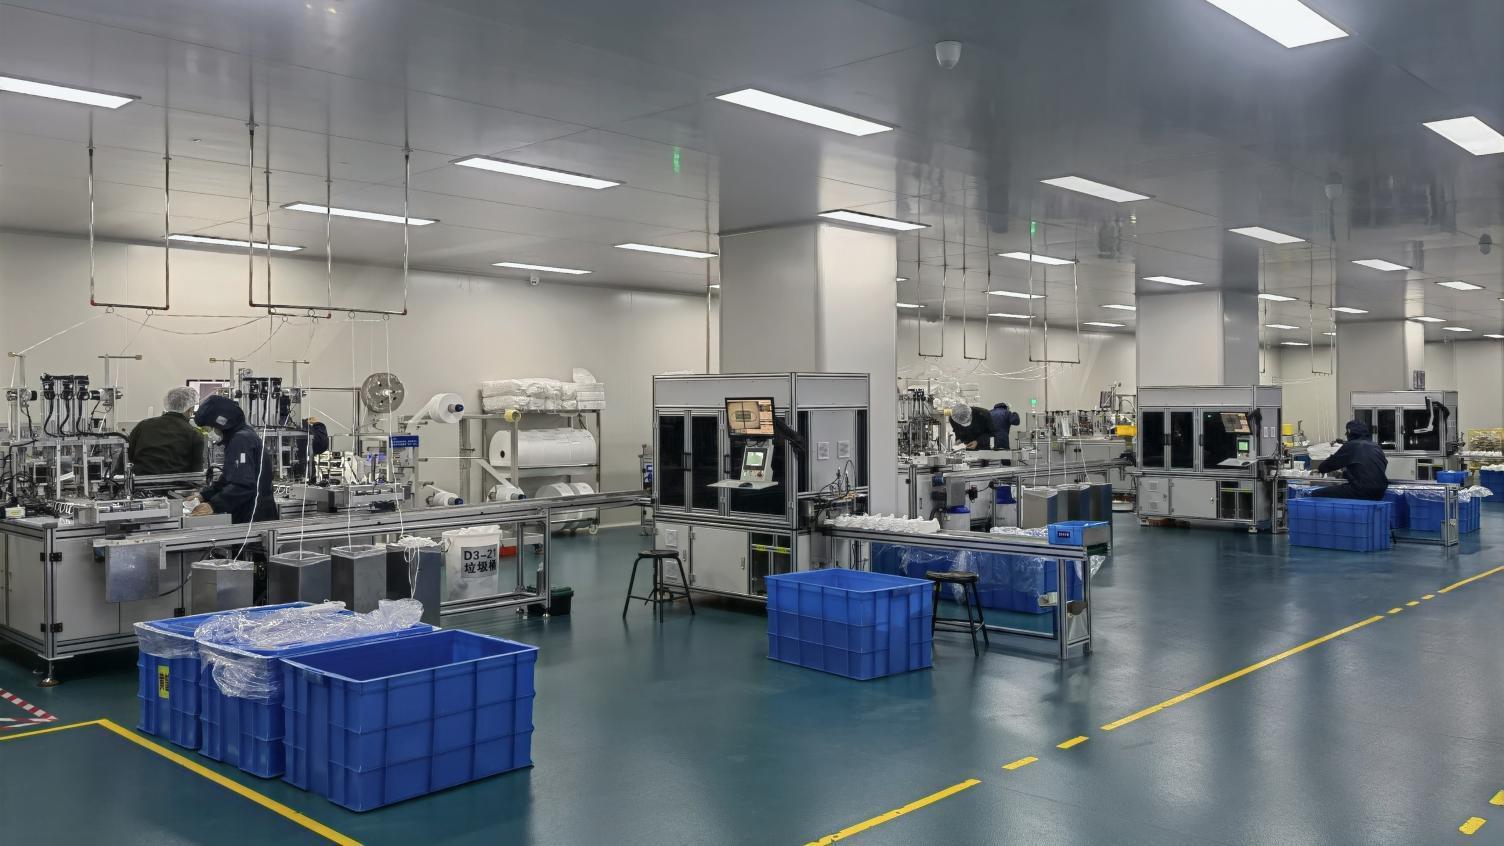
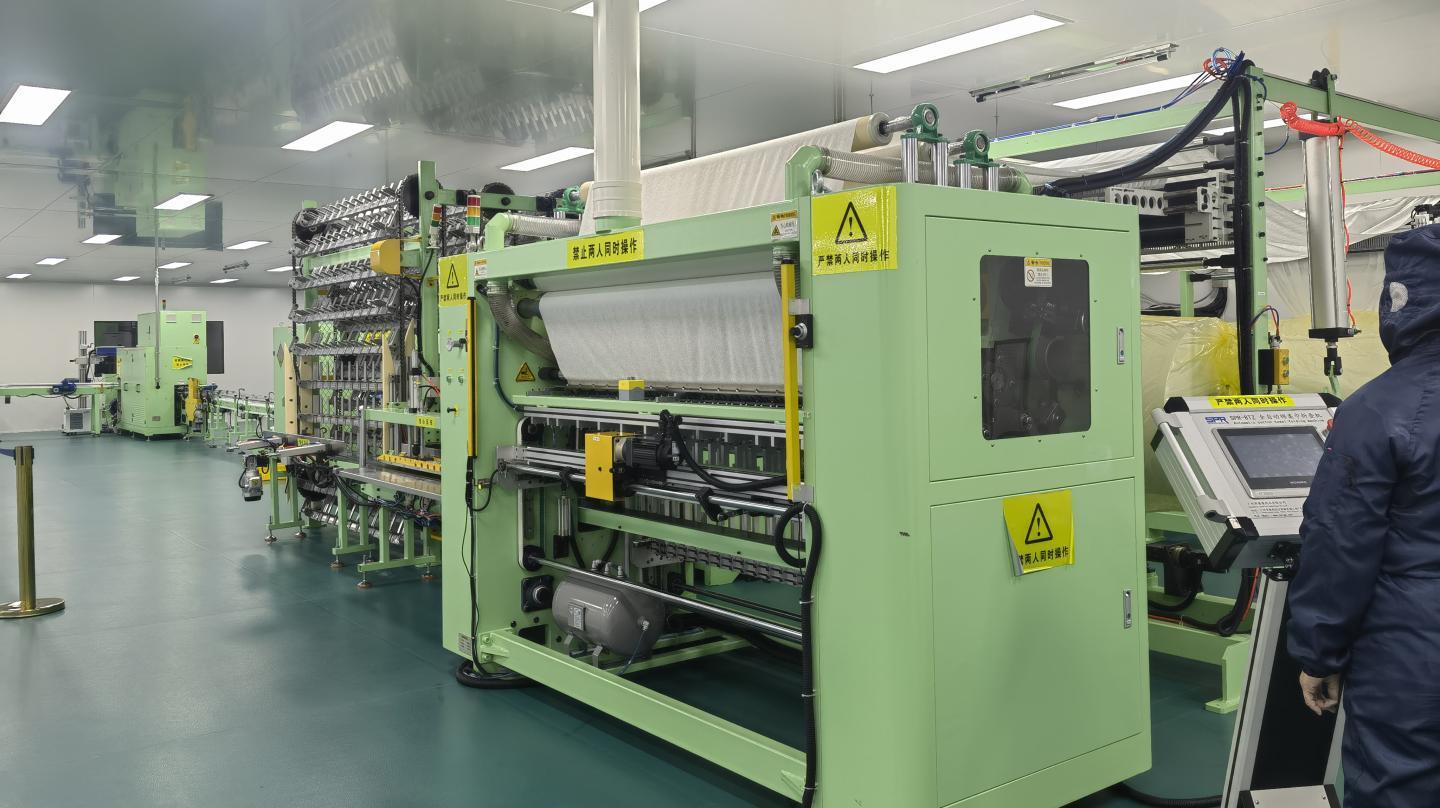
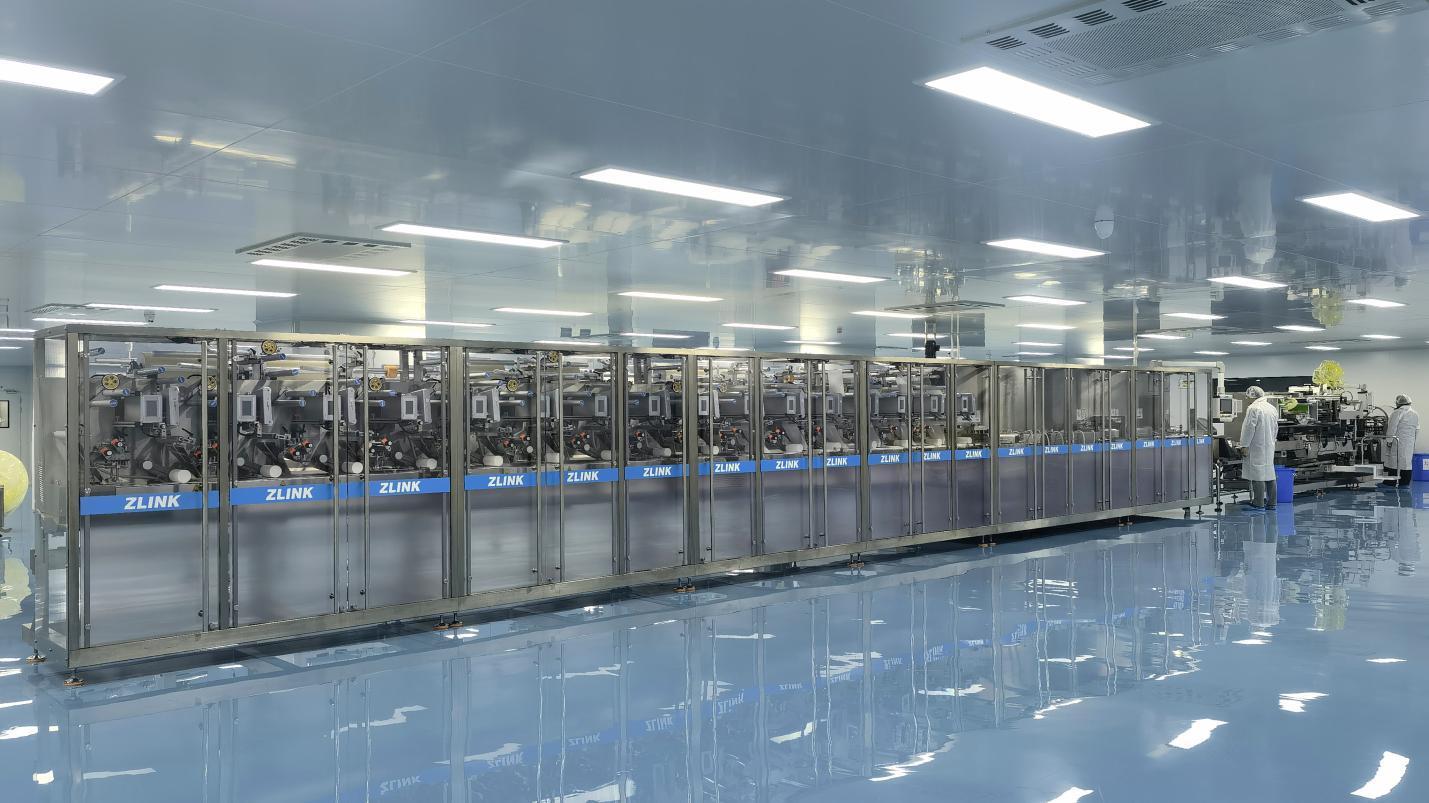
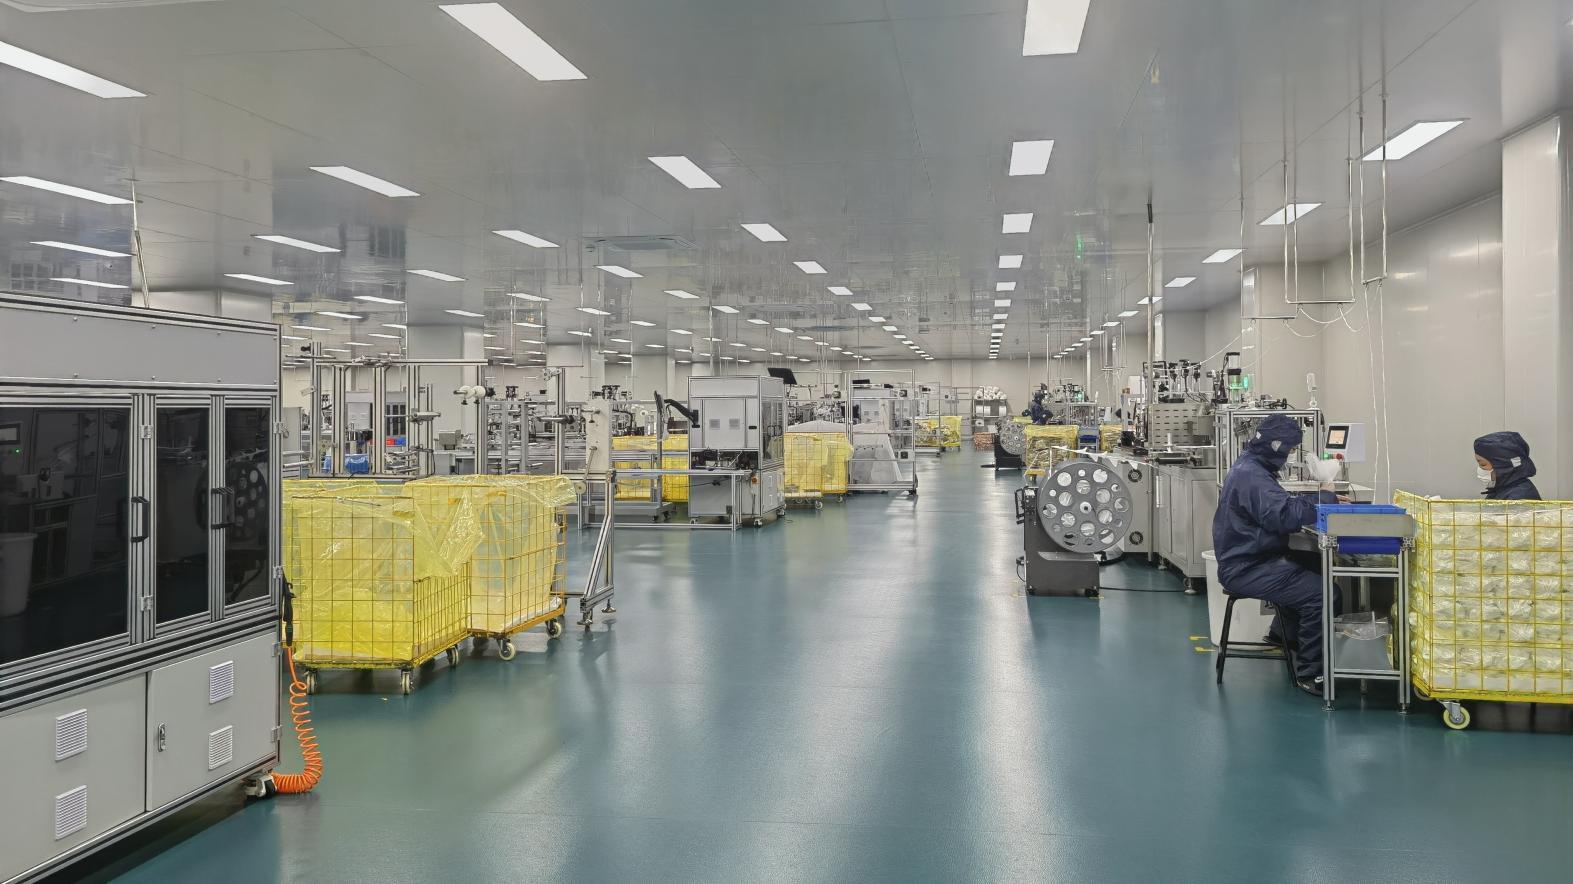
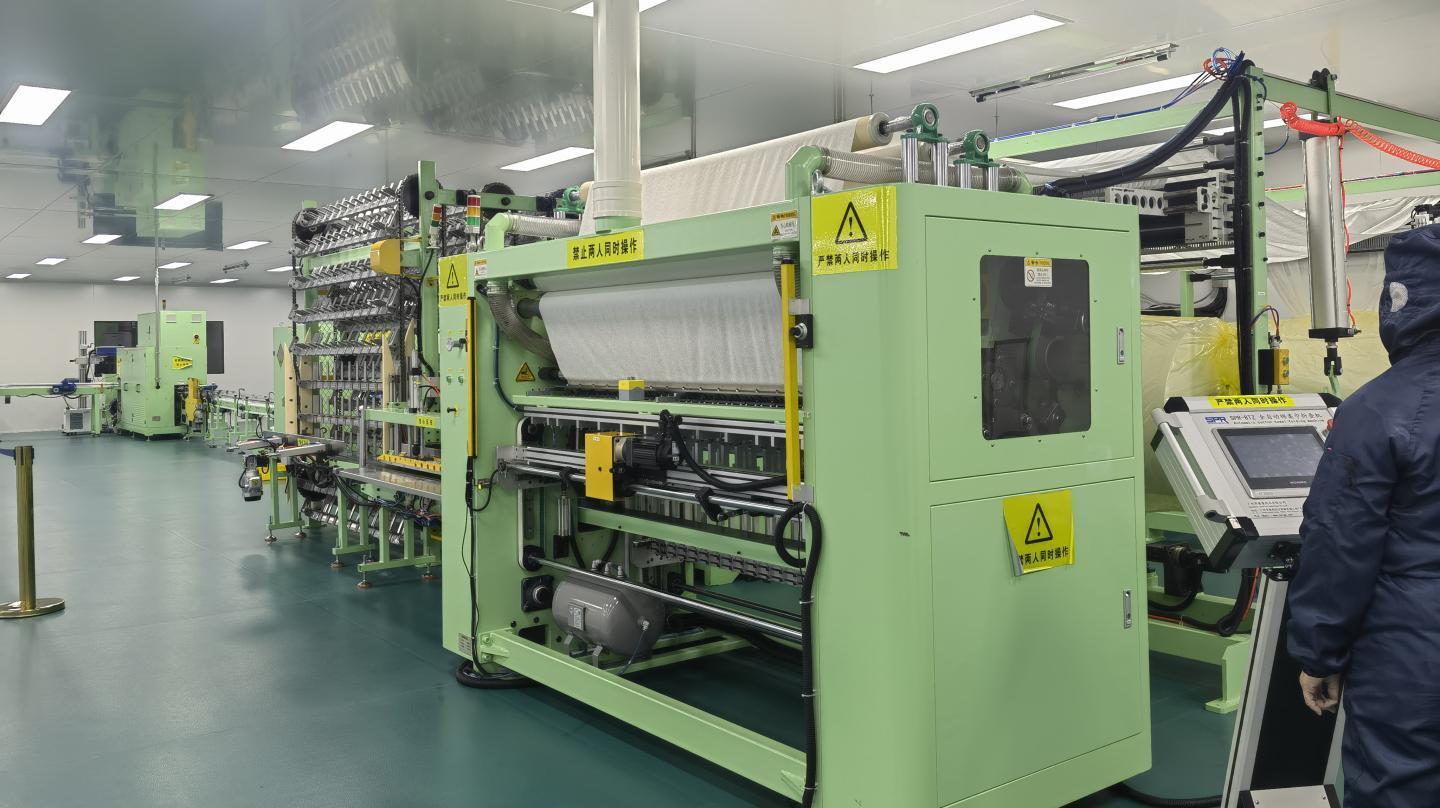
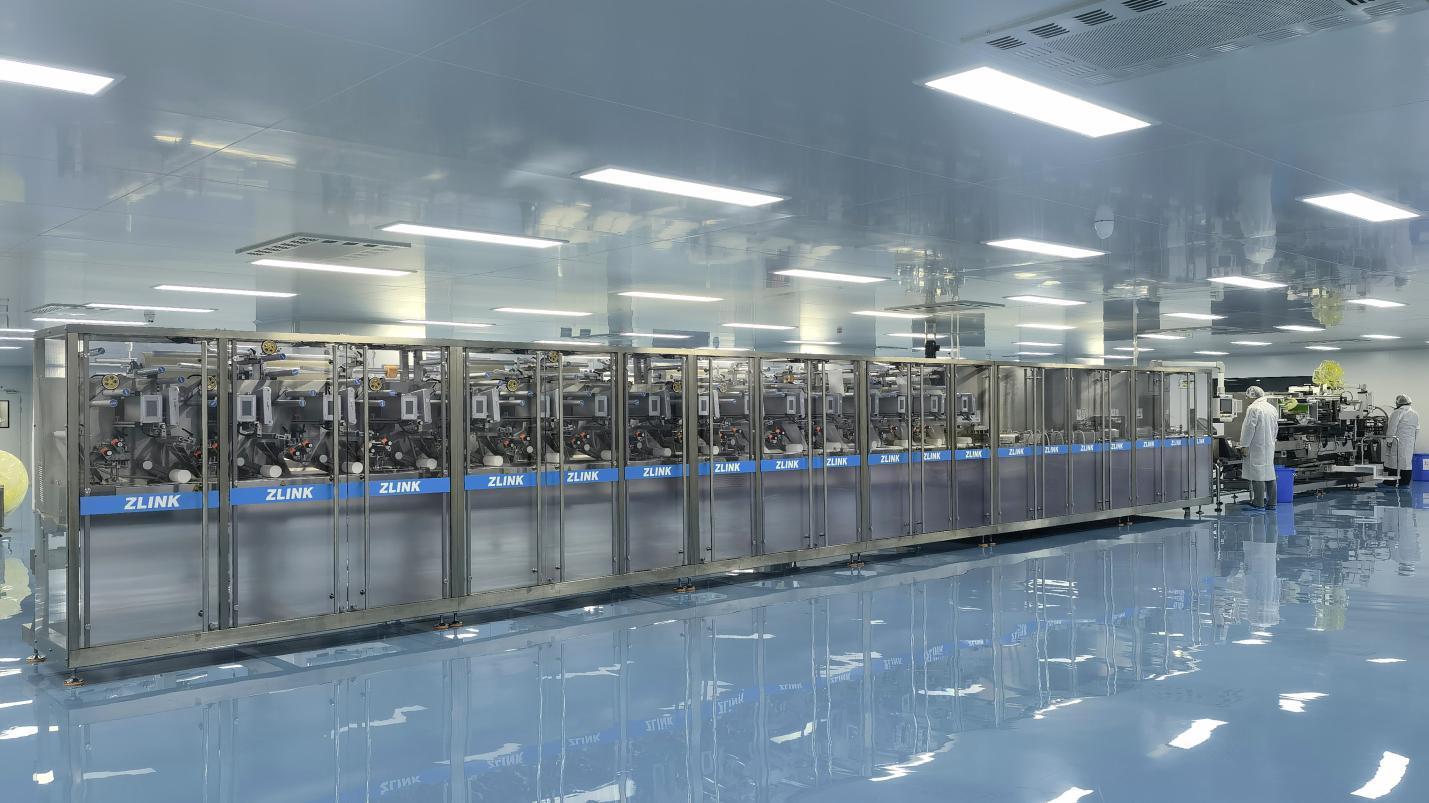
Moreover, advanced factories like Zhejiang DrSharpe Health Co., Ltd. integrate modern automation systems. Automation ensures consistent stitch sealing, seam reinforcement, and high-precision sizing. When manufacturing high-barrier apparel, consistency is not just a preference—it is a life-saving necessity. Any micro-fissure or poor stitch line can render a coverall ineffective against hazardous exposures.
| Sourcing Metrics | China Direct Procurement | Localized Assembly Lines |
|---|---|---|
| Material Sourcing | Direct raw-material integration (SMS, PP+PE) | Heavy reliance on imported raw materials |
| Customization (OEM/ODM) | High flexibility in size, design, logo & packaging | Limited due to specialized equipment costs |
| Production Capacity | Scales to millions of units weekly | Subject to local labor supply constraints |
| Quality Certificates | Strict CE, US FDA, EN 14126, ISO 13485 | Often fragmented across regions |
Protective apparel is only as good as its contextual performance. Different industries require specific polymer structures and protective properties.
Workers dealing with hydrocarbon extraction require anti-static (EN 1149-5) coveralls combined with high chemical liquid splash barriers. Microporous laminated film technology provides both vapor permeability and dynamic fluid resistance, keeping the operator safe and comfortable during long shifts in tropical refining environments.
In pharmaceutical compounding and high-end semiconductor cleanrooms, the focus is two-fold: protecting the operator from chemicals and protecting the product from human contamination. Low-linting, heavy-duty SMS fabrics ensure zero particulate emission while maintaining highly efficient airflow for thermal regulation.
Spraying pesticides and handling chemical fertilizers exposes agricultural laborers to aerosolized chemical compounds. A Type 6 certified chemical splash coverall prevents skin absorption, which is key to avoiding chronic occupational illnesses in Latin American agri-businesses.
The future of protective wear focuses on two goals: superior barrier properties and breathability. Traditional non-breathable protective gear often causes heat stress, leading to worker exhaustion and decreased compliance. Modern research from leading Chinese manufacturers integrates breathability directly into the polymer matrix.
Furthermore, environmental sustainability is now a major factor in international supply chain selection. Global enterprises are seeking recyclable non-woven materials, bioplastic composite films, and biodegradable protection wear that do not compromise on filtration efficiency or mechanical tensile strength. Advanced melt-blowing processes are being refined to produce microfibers that decompose safely in industrial composting environments.
Zhejiang DrSharpe Health Co., Ltd. is a professional manufacturer and global supplier specializing in disposable medical and healthcare products, especially high-quality face masks and protective solutions. With strong manufacturing capabilities, advanced production technology, and strict quality management, DrSharpe is committed to providing safe, reliable, and comfortable healthcare products for customers worldwide.
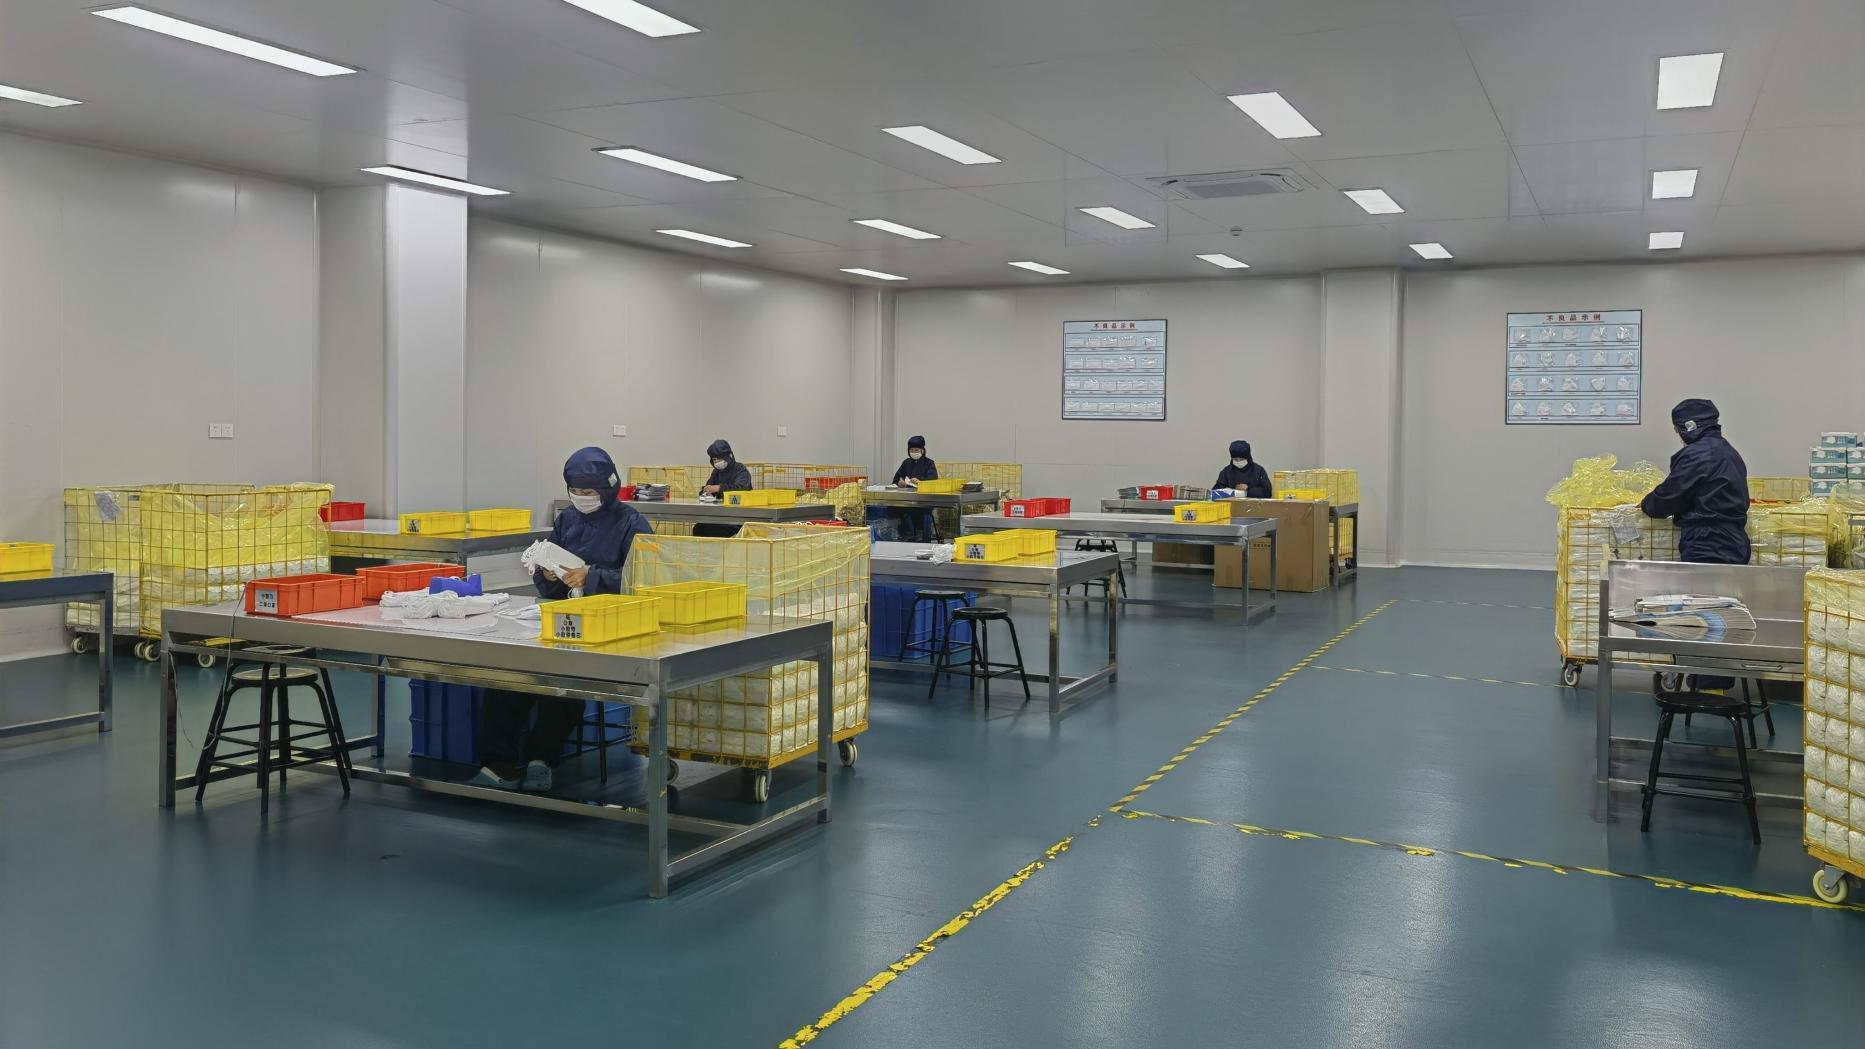
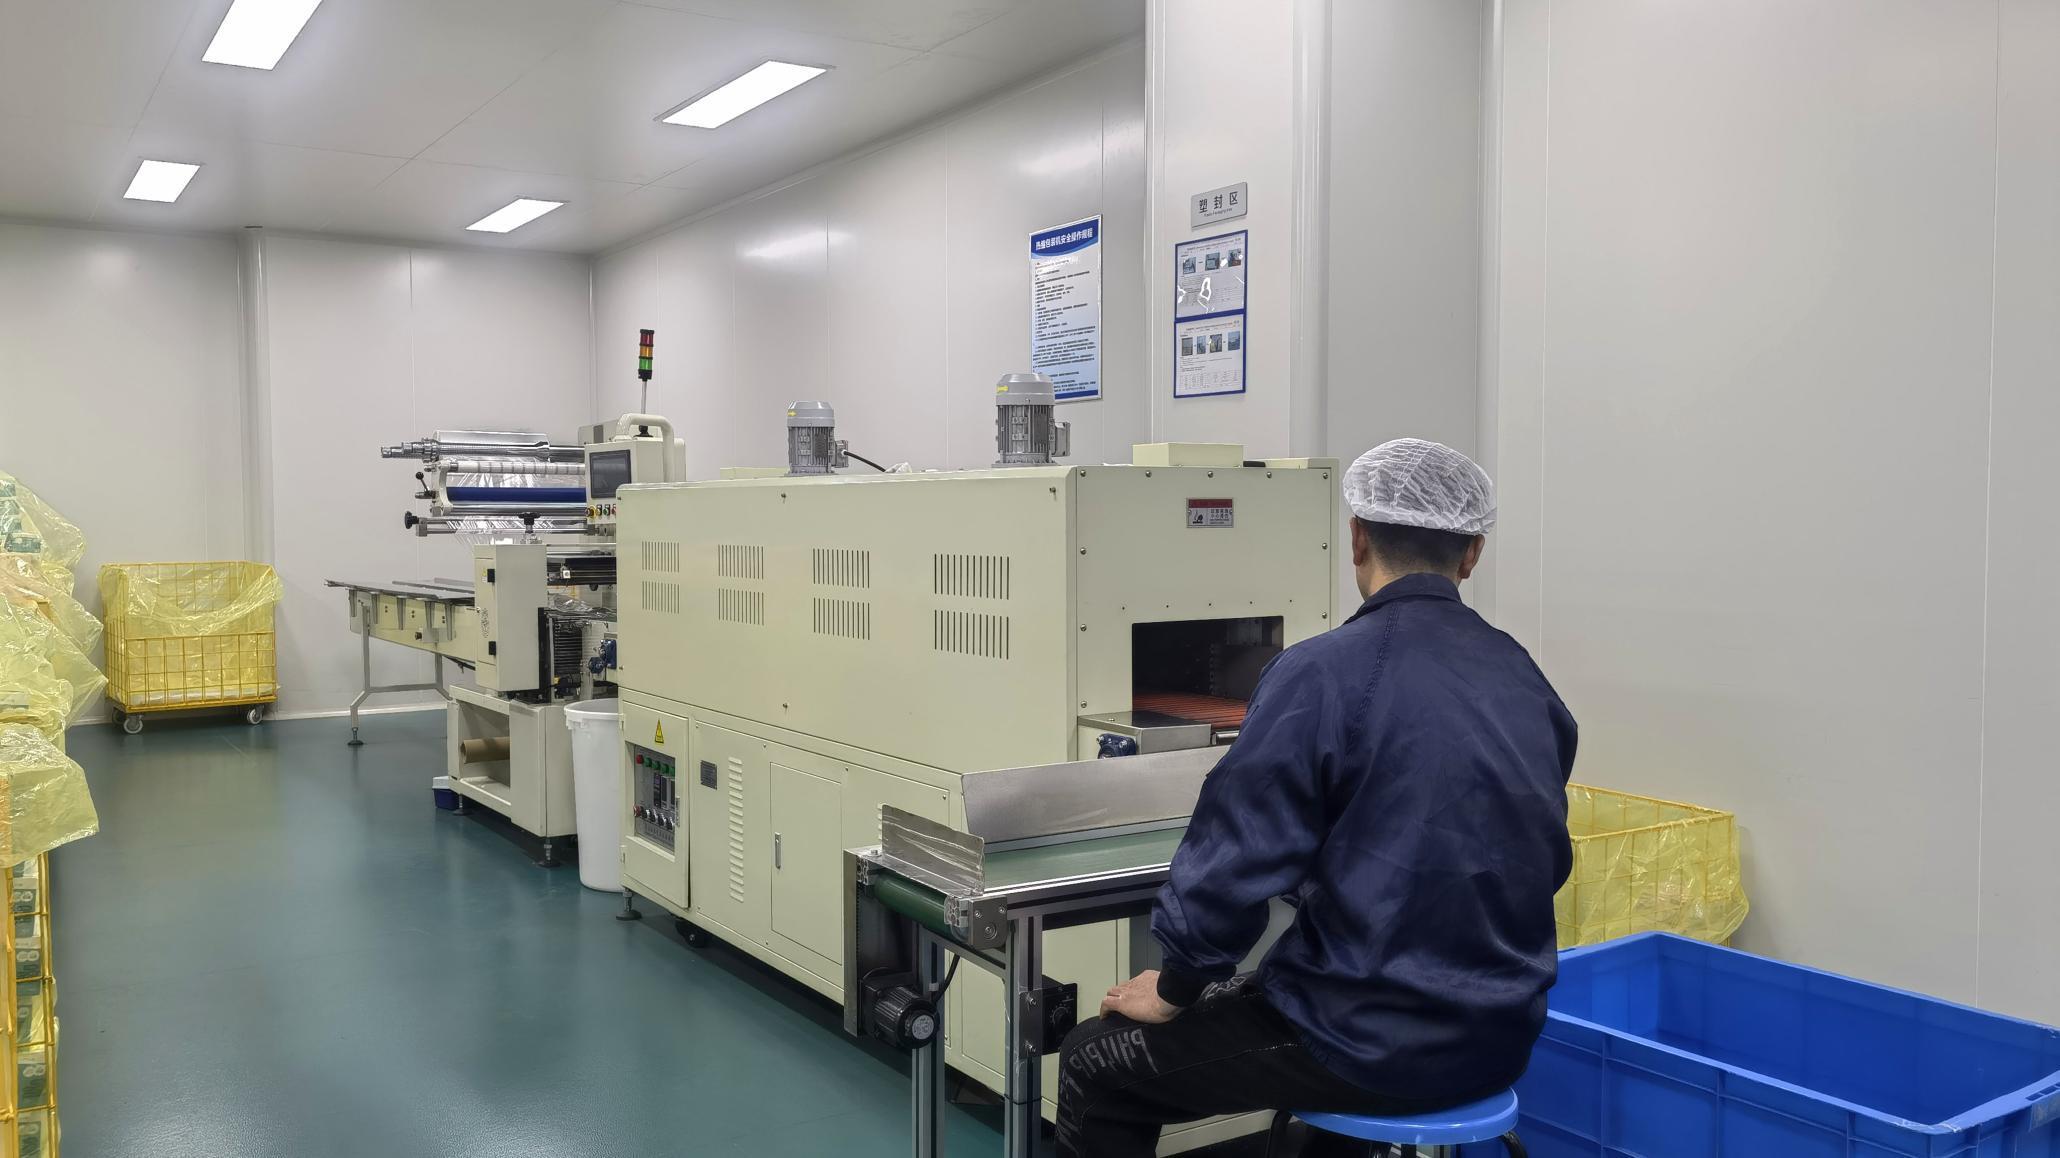
DrSharpe has built a reputation for reliable product quality and outstanding supply continuity. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to international markets, including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
Our state-of-the-art factory is equipped with 5 fully automatic mask production machines and 12 semi-automatic mask production machines, supported by an experienced production and service team. Using advanced filtration materials, our products achieve up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE). Our items comply with international standards, holding certifications including CE, US FDA, and US EUA.
When sourcing industrial PPE, global procurement agents must mitigate logistics risk, verify compliance certificates, and ensure factory capacity matches long-term contract requirements. Sourcing managers should prioritize suppliers that offer full customization capabilities—including raw material weight options (e.g., 55g, 65g, or 75g SMS/microporous laminate), custom packaging designs, and robust logistics assistance.
At Zhejiang DrSharpe Health Co., Ltd., we streamline the supply process. From packaging and custom branding to customs documentation, we ensure your order reaches its port of delivery on time. Our raw materials are subjected to rigorous testing under extreme conditions, ensuring high tensile strength, anti-tearing thresholds, and fluid barriers that protect your workforce.
Our protective coveralls utilize spunbond-meltblown-spunbond (SMS) composite fabrics or microporous film-laminated nonwovens. SMS offers high breathability and standard dust particle filtration, while microporous film provides a liquid splash barrier ideal for industrial applications.
Yes. We support custom branding, tailored sizes, custom density options (gsm), and private label packaging design to meet localized distribution requirements.
Our respiratory protective products achieved CE, US FDA, and US EUA approvals. They meet rigorous testing parameters for up to 99% Bacterial Filtration Efficiency (BFE) and Particle Filtration Efficiency (PFE).
Our production features 5 fully automatic and 12 semi-automatic production machines. This machinery reduces human error, and is backed by in-line quality inspections and batch-testing procedures.
Standard orders are typically processed and shipped within 15 to 30 days, depending on custom requirements and current raw material stocks. We coordinate directly with global logistics partners to streamline customs clearance.
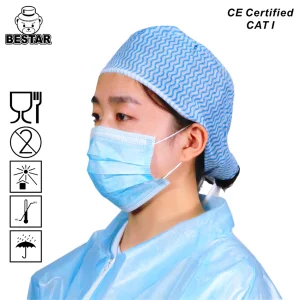
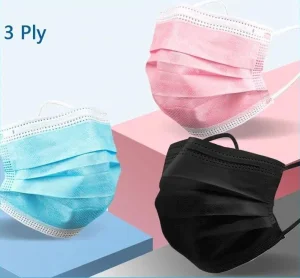
Looking for reliable bulk supply of Overoles de Protección or certified filtration masks? Partner with Zhejiang DrSharpe Health Co., Ltd. and secure your global supply chain today.