DrSharpe Health
Explore our comprehensive array of certified protective products engineered for diverse medical, civic, and industrial environments.
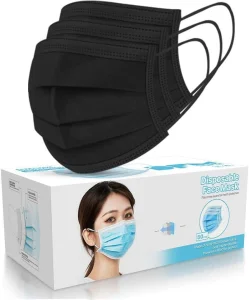
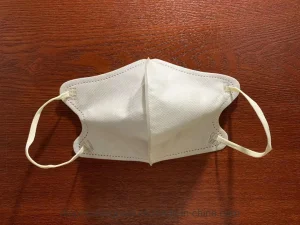
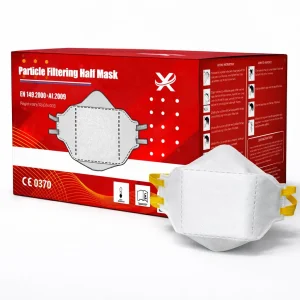
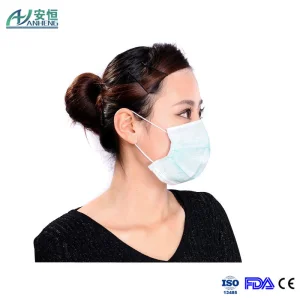
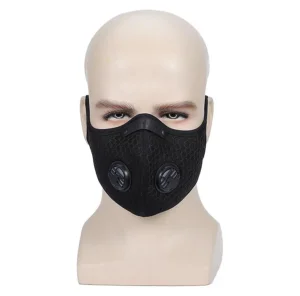
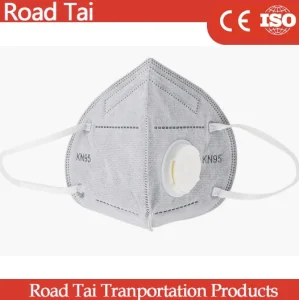
The global demand for protective wear has experienced a paradigm shift. B2B buyers, municipal authorities, and safety managers are actively transitioning from single-use plastics to advanced reusable textile solutions—commonly referred to in Spanish-speaking and international markets as Mascarillas Lavables. This evolution is driven by two main pillars: environmental sustainability (reducing millions of metric tons of microplastic waste) and long-term cost efficiency.
Today's industrial-grade washable masks are no longer simple cloth barriers. Modern manufacturing processes incorporate high-tech synthetic and natural fibers treated with active antimicrobial coatings, bringing their filtration efficiencies closer to medical standards. As global supply chain protocols tighten, working with a certified OEM manufacturer guarantees compliance with standards like ASTM F3502-21 in the United States and UNE 0065/CWA 17553 in the European Union.
The intersection of material science and artificial intelligence is reshaping how manufacturers design protective systems.
Incorporating electrospun polymer nanofibers allows filters to capture sub-micron particles. The integrated nano-mesh layer creates a physical path too complex for particulate matter to penetrate, maintaining high breathability.
Manufacturers are turning to PLA (polylactic acid) and organic bamboo blends. These materials naturally break down at the end of their multi-wash lifecycle, ensuring the circular economy remains closed.
Treating the outer fabric layer with durable water repellent (DWR) compounds ensures that liquid droplets run off immediately. This acts as the first line of defense against splashes in clinical and retail environments.
Different environments present unique protection, breathability, and customization challenges.
In manufacturing environments, workers are exposed to particulates, fine dust, and dynamic heat conditions. Washable masks designed with adjustable ear loops, nose bridges, and exhaling valves ensure comfort during extended 8-12 hour shifts, reducing replacement overheads.
Companies globally use OEM customization to print precise brand colors, corporate logos, and custom graphics on employee face masks. This integrates physical safety protocols directly with front-facing corporate branding.
Transit staff, hotel personnel, and public service agents interact daily with large groups. Standardized washable masks with active silver-ion coatings provide continuous protective barriers that require simple washing cycles to refresh.
An engineered reusable mask is defined by its material configuration. Our typical high-filtration OEM Mascarillas Lavables consist of a three-layered hybrid barrier that maintains particle arrest while lowering inhalation resistance:
1. Outer Layer (Hydrophobic Protection): 100% tightly woven polyester or polyamide treated with fluid-resistant coatings, shielding the user from liquid-borne droplets.
2. Middle Layer (Micro-Filtration Filter): High-density Melt-blown non-woven fabrics or PTFE membranes that act as an electrostatic barrier, trapping PM2.5 particles and micro-bacteria.
3. Inner Layer (Hypoallergenic Comfort): Ultra-soft organic cotton or moisture-wicking bamboo fibers that manage heat, prevent skin irritation, and allow continuous wear.
Our material engineering ensures that our products retain up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE) even after extensive laundering cycles under industrial guidelines.
Performance analysis compared across multiple washing iterations at 60°C.
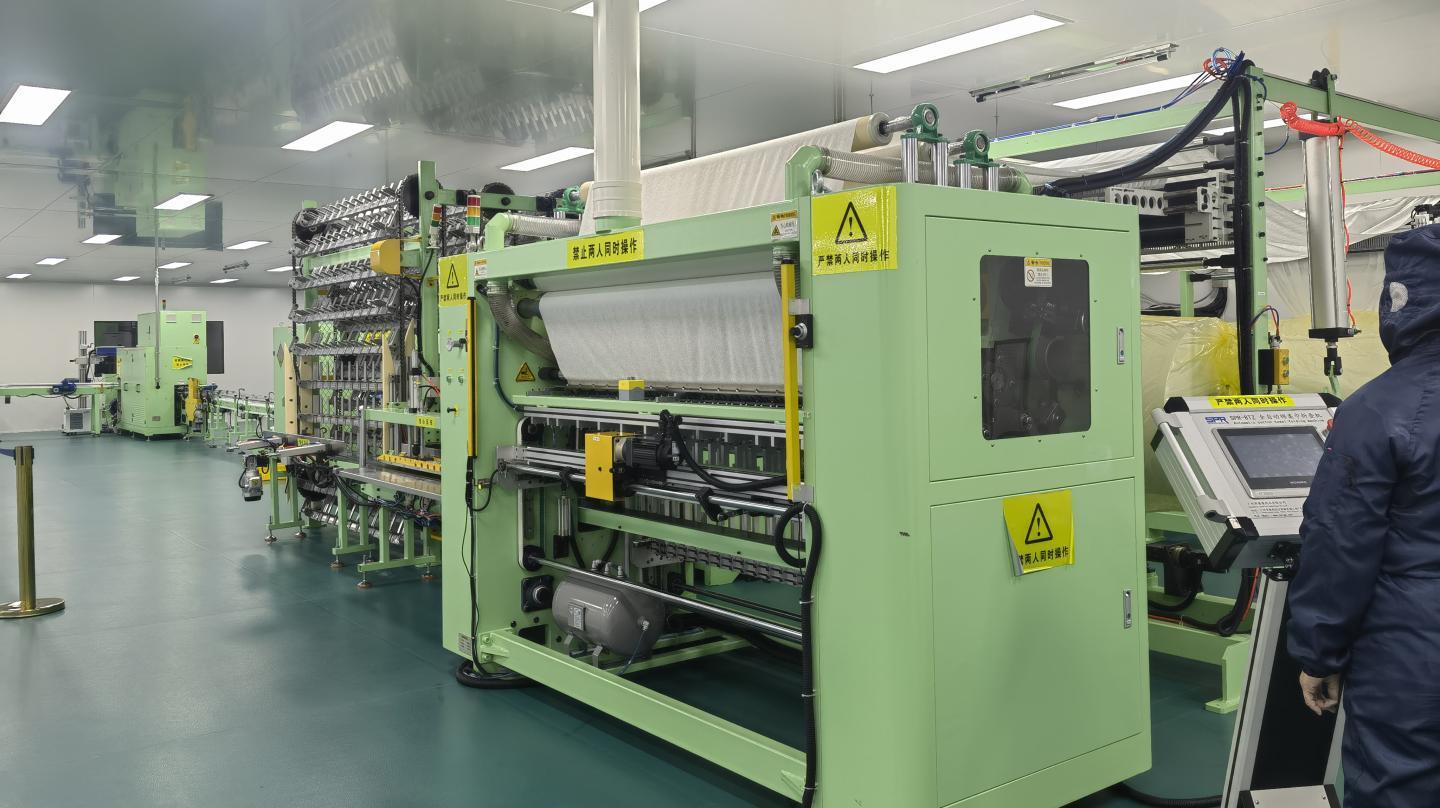
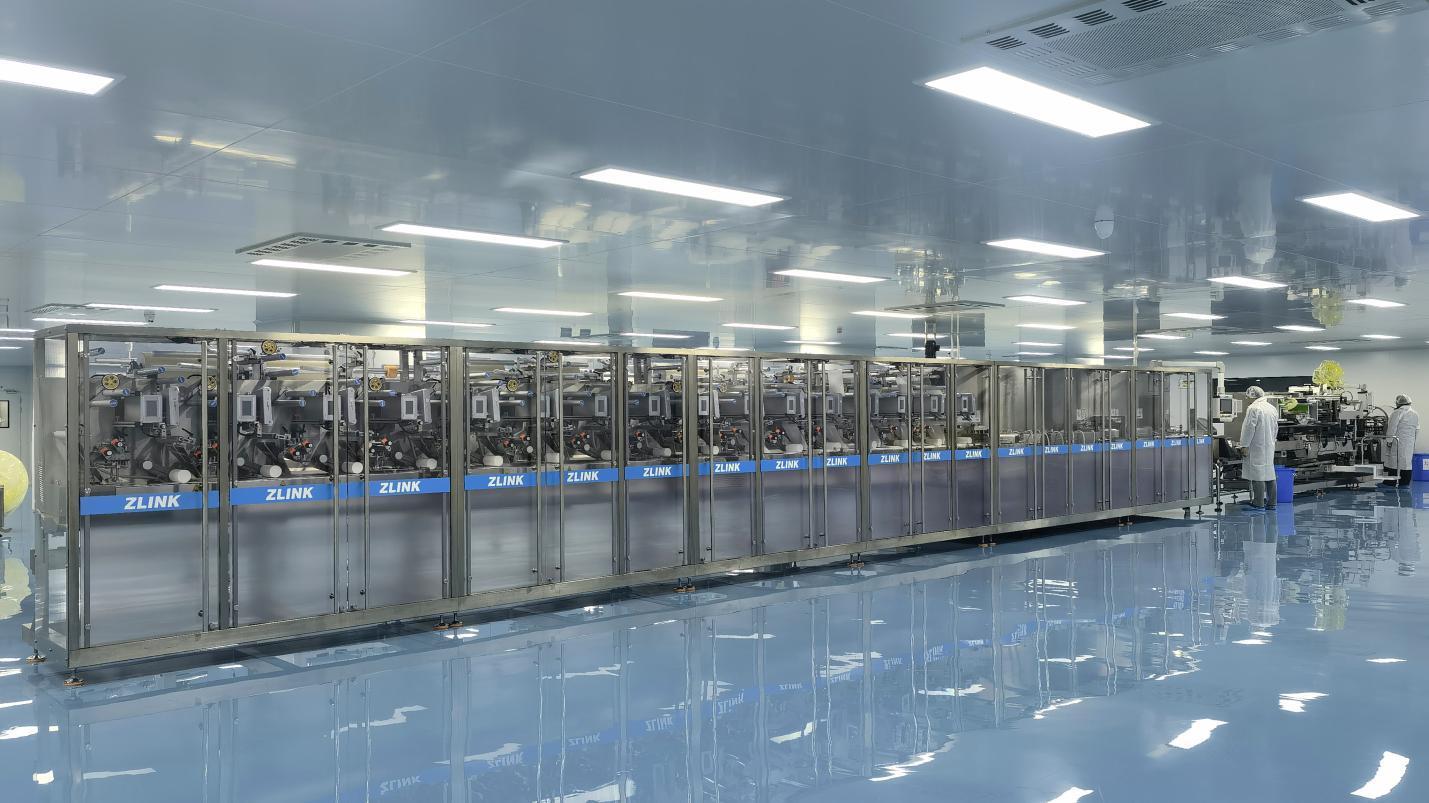
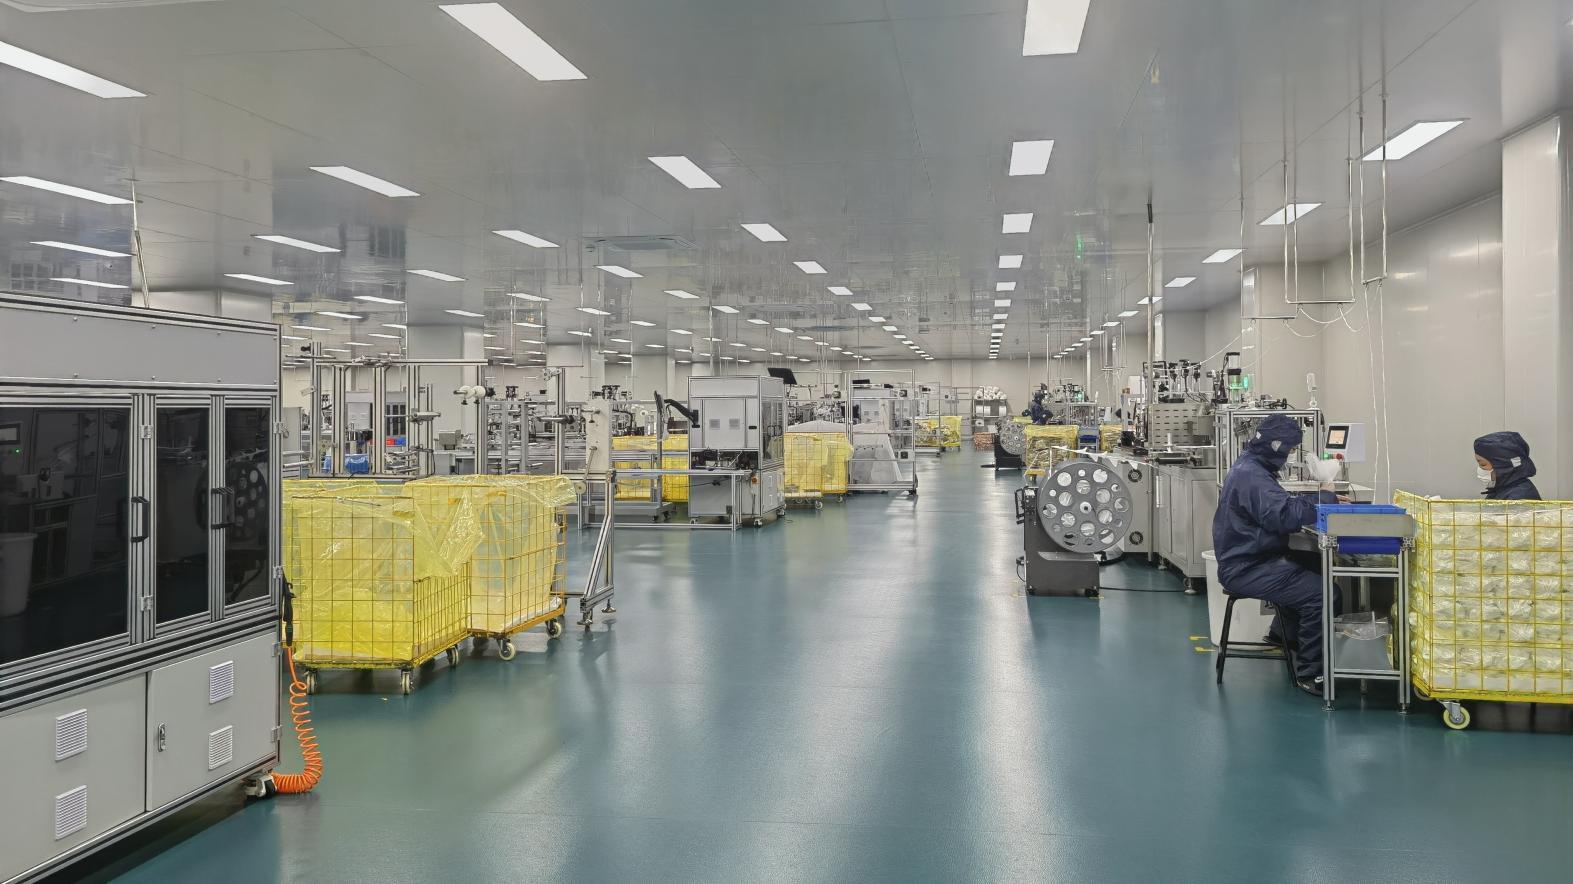
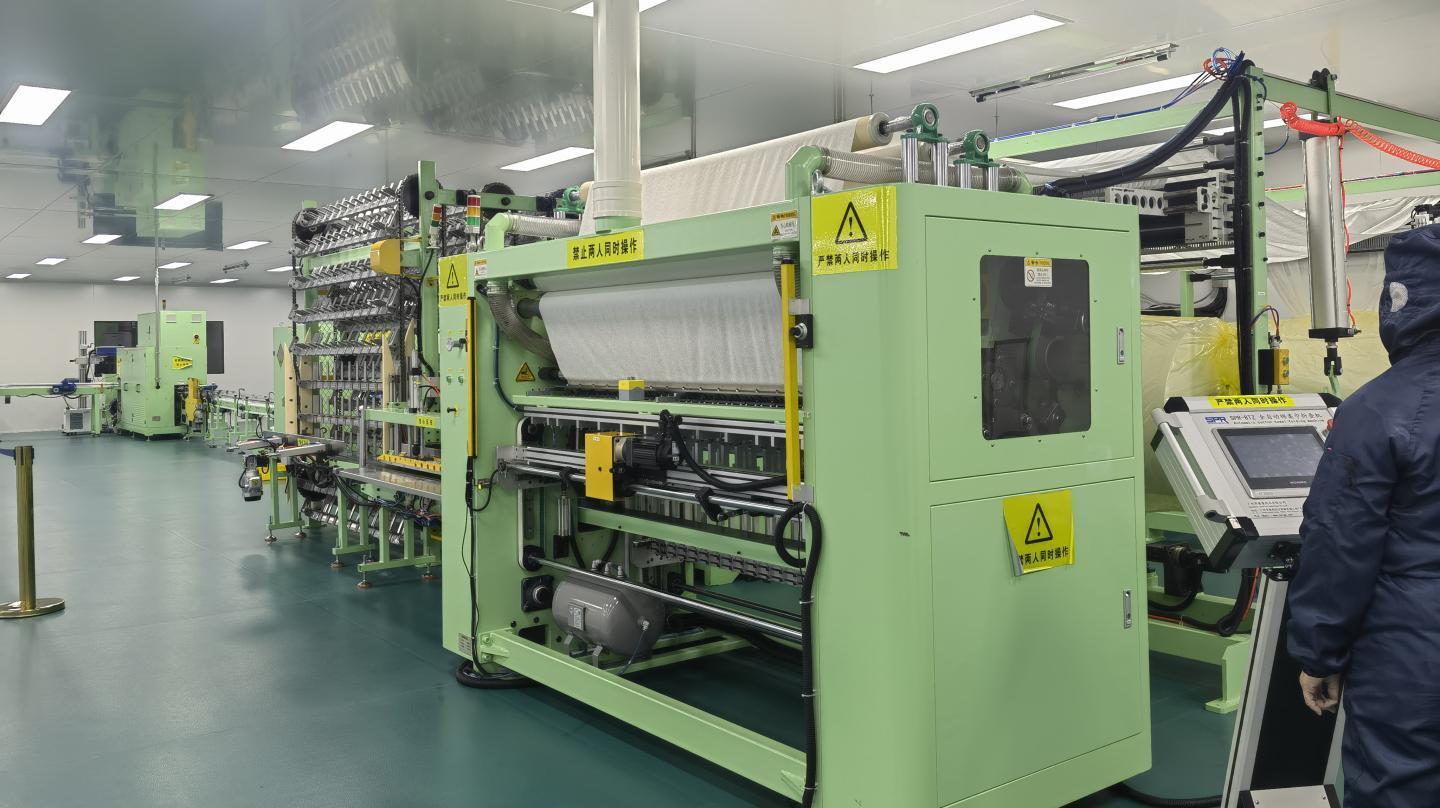
Our state-of-the-art facility integrates automated technology to scale up production demands rapidly while ensuring tight quality control on every single batch.
Zhejiang DrSharpe Health Co., Ltd. is a professional manufacturer and global supplier specializing in disposable medical and healthcare products, especially high-quality face masks and protective solutions.
With strong manufacturing capabilities, advanced production technology, and strict quality management, DrSharpe is committed to providing safe, reliable, and comfortable healthcare products for customers worldwide. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to markets including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
Using advanced filtration materials, our masks achieve up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE), offering excellent protection and wearing comfort.
High-precision machinery, dust-free manufacturing environments, and systematic inspection protocols shape our standard operating procedures.
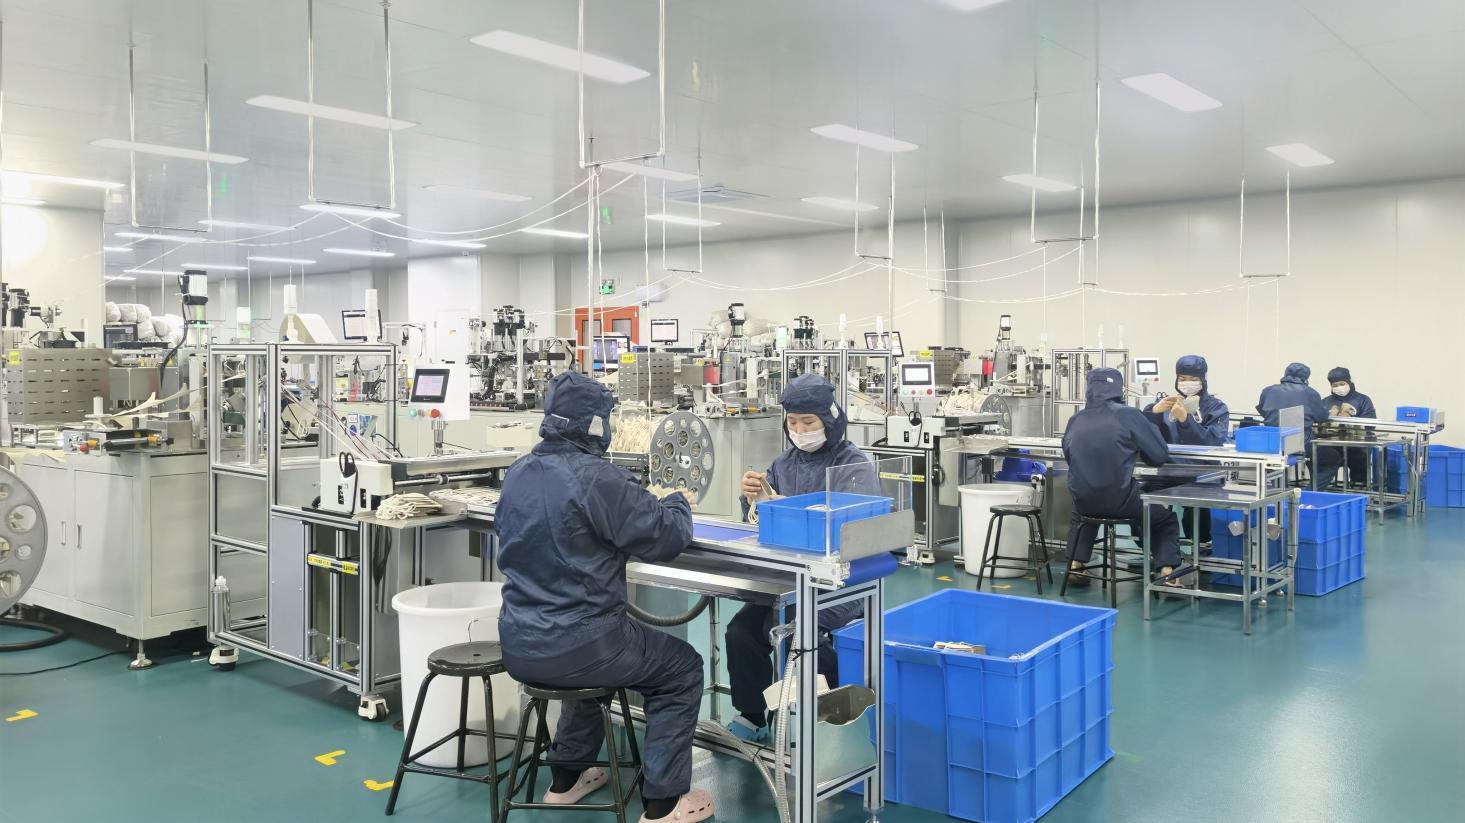
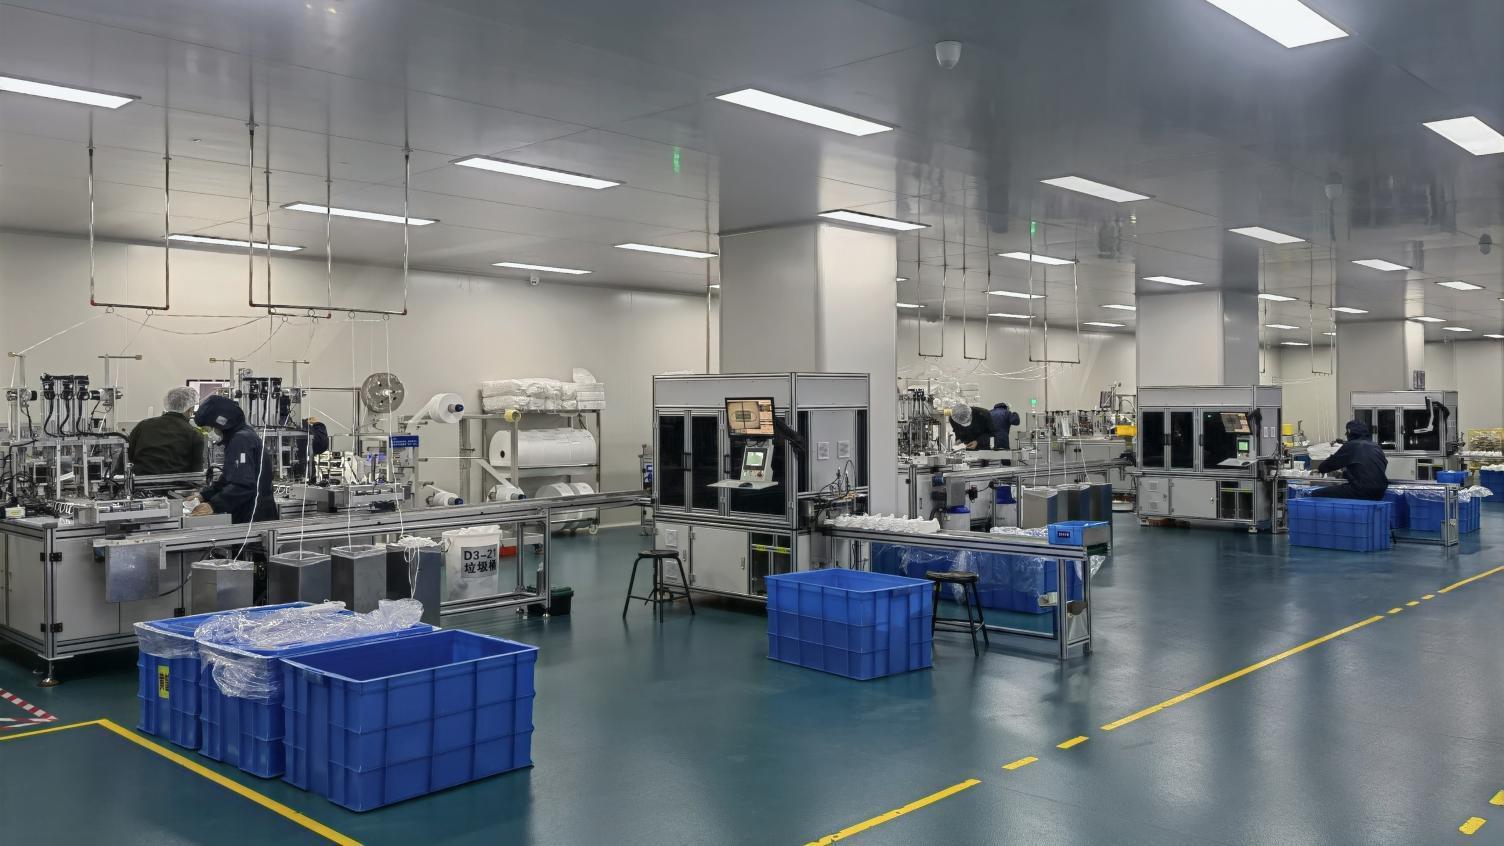
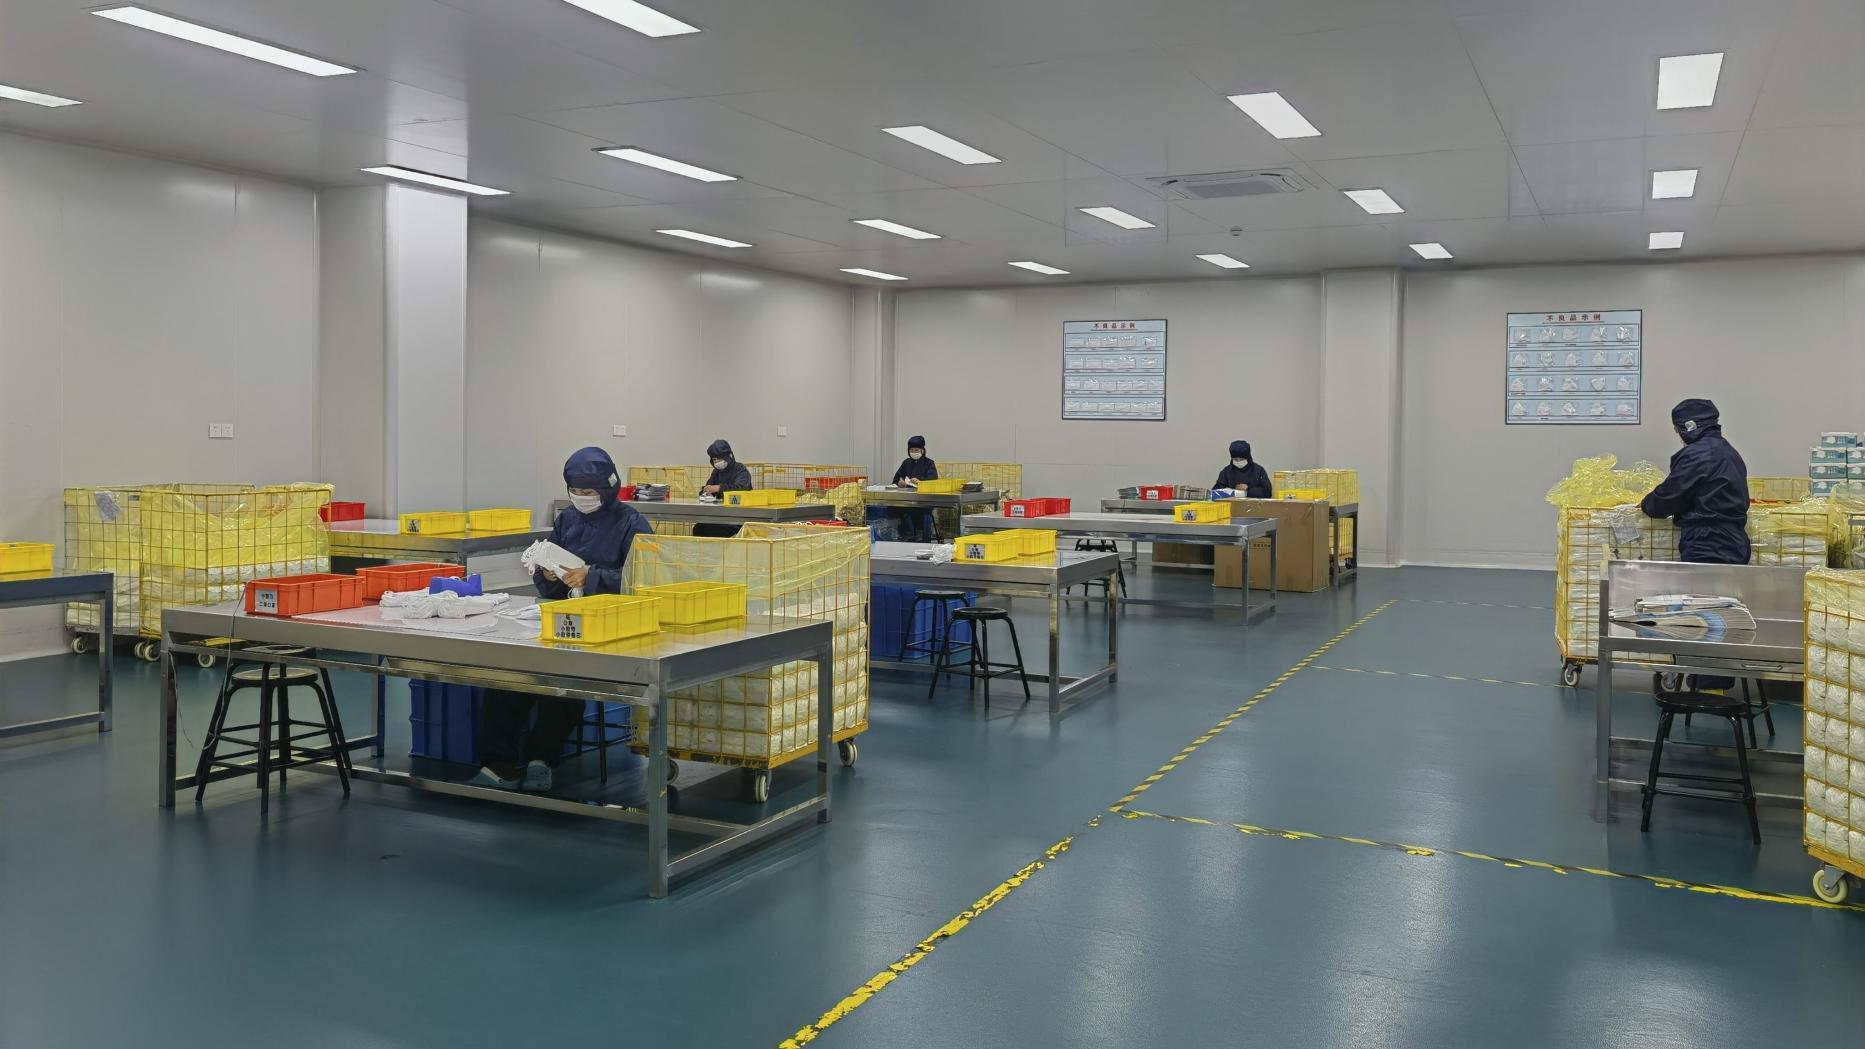
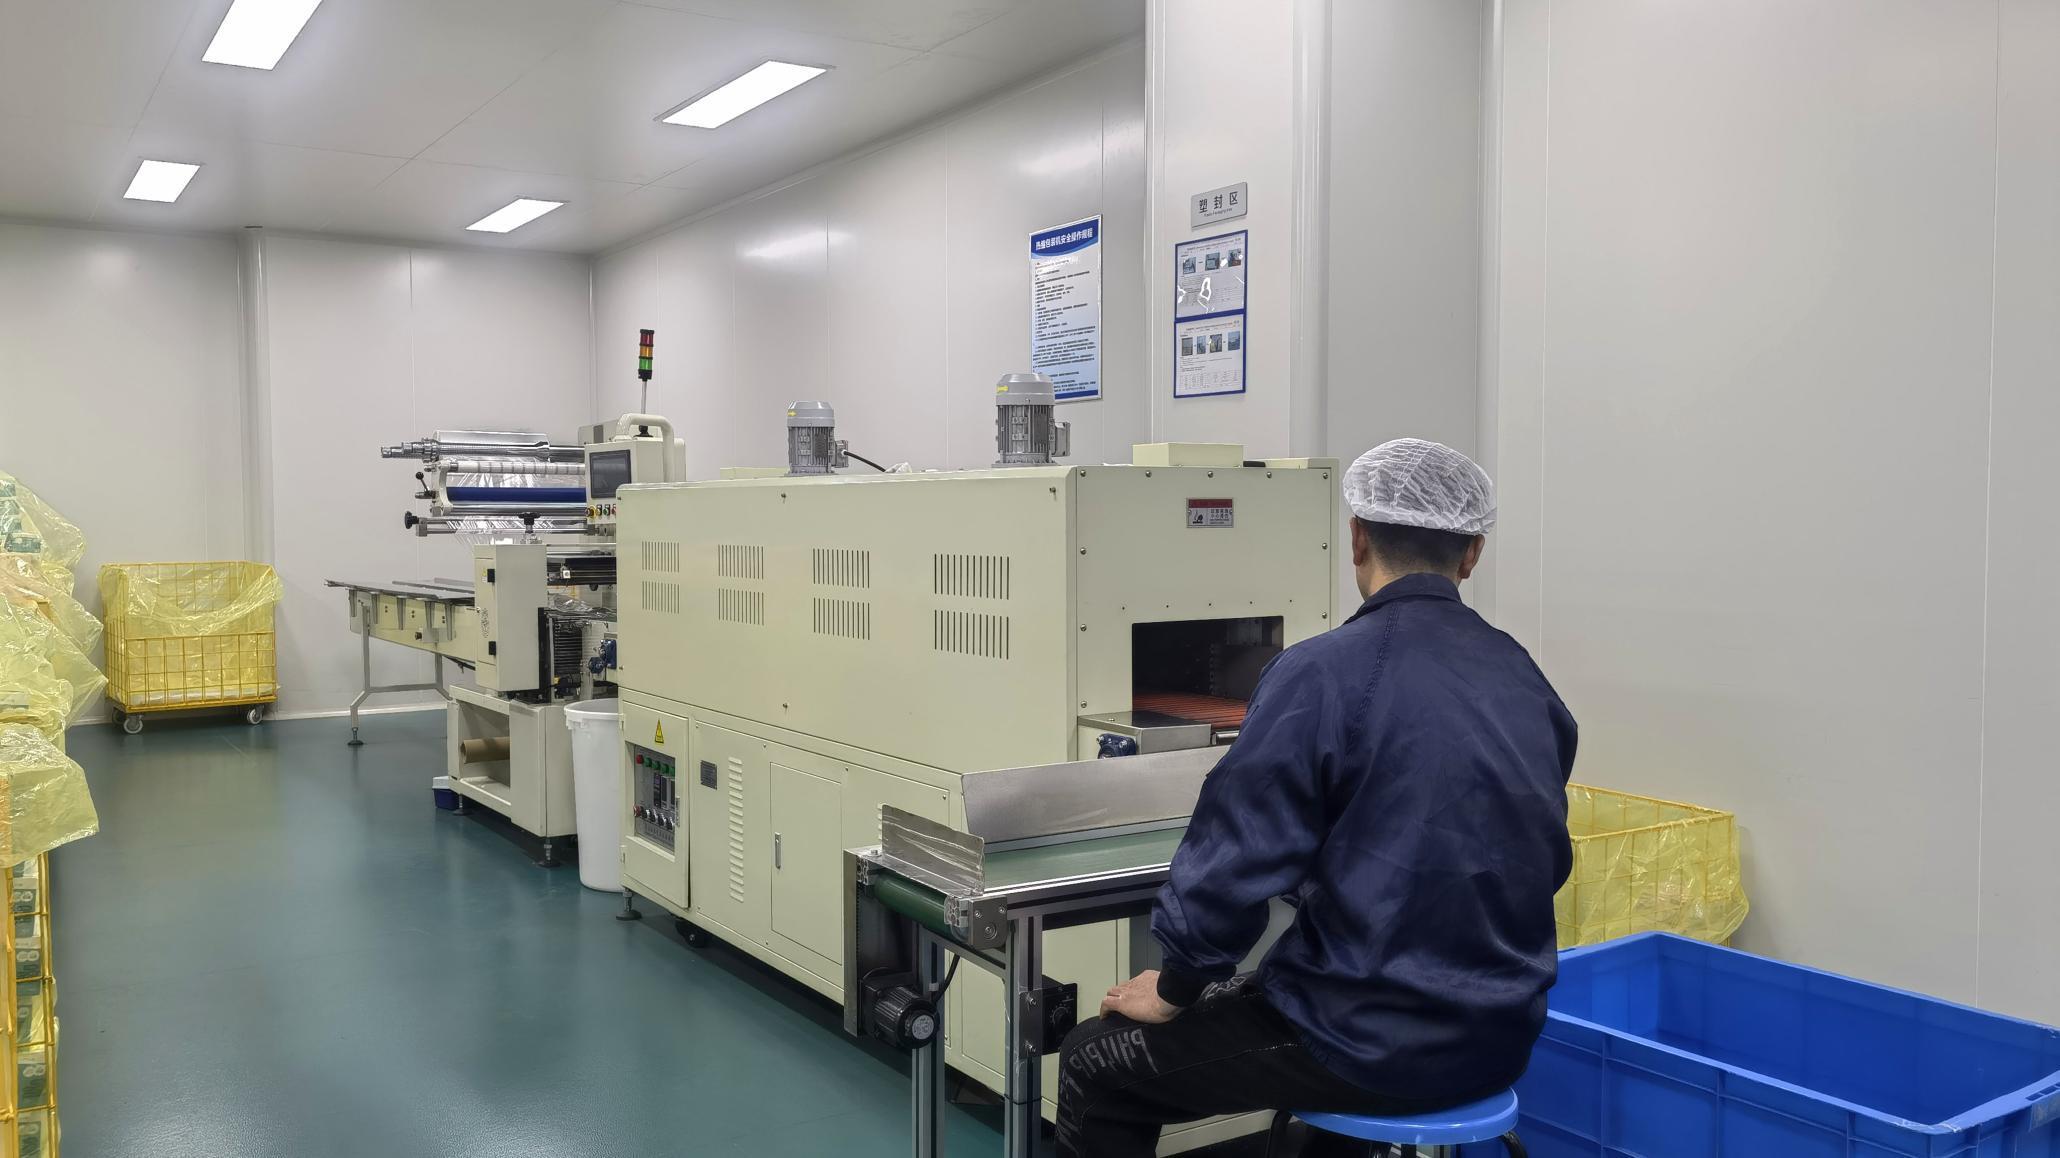
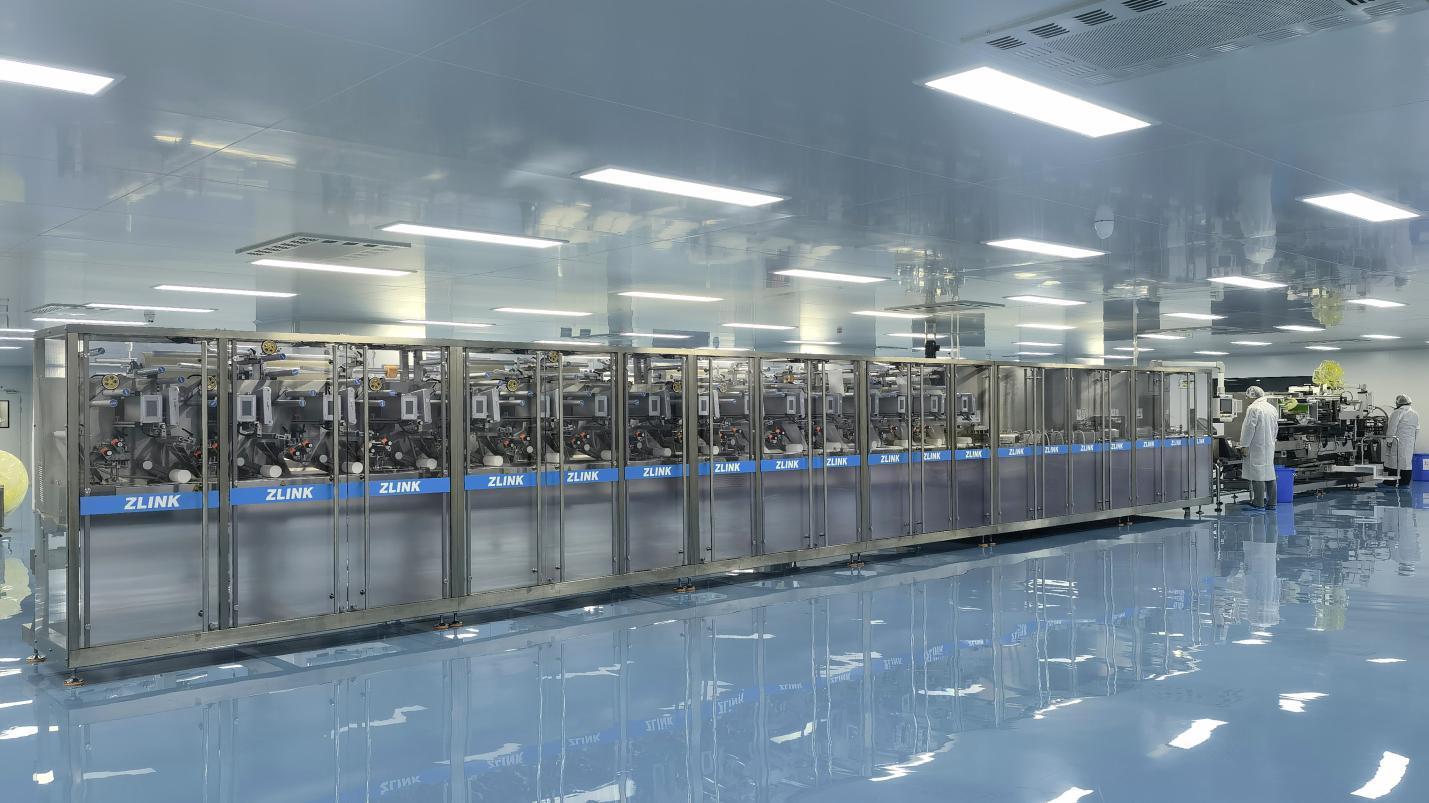
Working with DrSharpe guarantees a streamlined path from concept design to high-volume cargo delivery.
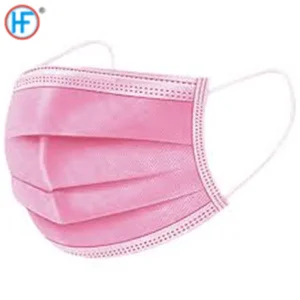
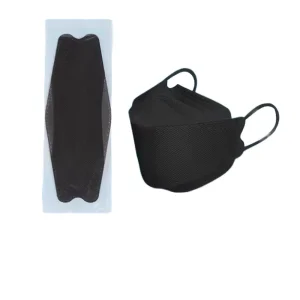
Clients specify target certifications (e.g., UNE 0065 or local equivalents), fabric densities, structural styles (3D folded, KF94 shape, or flat pleated), and logo placements. Sample prototypes are finalized in days.
Once samples are approved, mass production begins utilizing our 5 fully-automated mask production machines. This limits human touchpoints to preserve cleanliness and ensure stability in fiber tension.
Every batch undergoes automated and manual inspection testing for strap weld strength, nose wire stability, and surface inconsistencies prior to cleanroom packaging and heat-sealing.
Detailed answers regarding material properties, washing procedures, and custom OEM processes.
Continuous supply chains for high-volume orders. Premium quality and certified safety products.