 DrSharpe Health
Explore our core selection of certified medical masks, protective respirators, and daily safety face covers engineered for maximum filtration efficiency and user comfort.
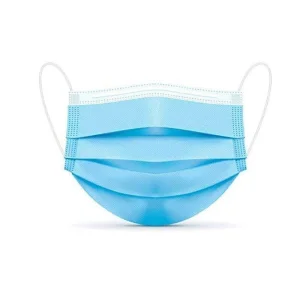
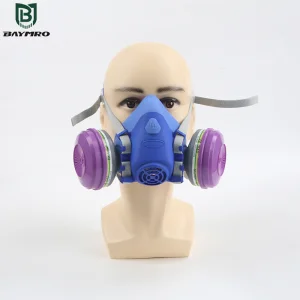
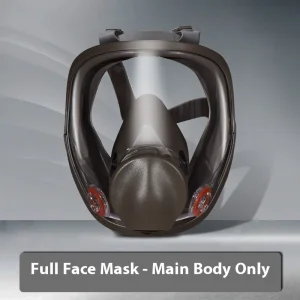
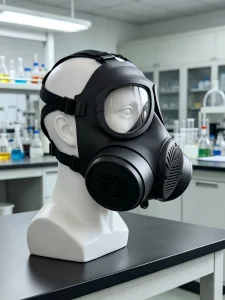
The global healthcare landscape is witnessing a paradigm shift in how Suministros Hospitalarios (hospital supplies) are procured, distributed, and utilized. In an era marked by rapid epidemiological shifts, geopolitical instabilities, and strict health regulations, medical institutions are steering away from transient, transaction-based sourcing toward deep, strategic partnerships with highly integrated manufacturers.
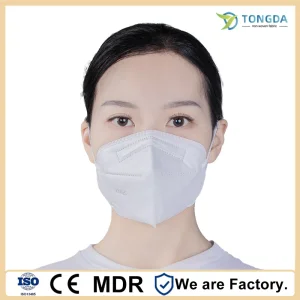
Today, the standard for medical consumables has evolved. It is no longer just about meeting basic protection requirements; it is about providing uncompromising barrier integrity, breathability, and biocompatibility. As hospitals globally implement strict protocol frameworks, the demand for certified personal protective equipment (PPE)—ranging from disposable 3-ply surgical masks to industrial-grade full-facepiece respirators—has surged exponentially.
A key trend driving the industry is the convergence of clinical-grade safety and ergonomic functionality. Hospitals now require products with optimized physical architecture: anatomical 3D contours that eliminate gaps, skin-friendly hypoallergenic non-woven fabrics, and high-tensile earloops that prevent fatigue during extended clinical shifts. Sourcing these advanced supplies requires a partner that controls the entire quality lifecycle, from polypropylene polymer synthesis to sterile packaging.
Direct factory procurement eliminates multi-tiered intermediary margins, allowing healthcare networks to reallocate budgets to critical patient-care technologies.
Adherence to global standards (CE, US FDA, US EUA) ensures smooth importation process and absolute risk mitigation against clinical contamination incidents.
Bacterial Filtration Efficiency (BFE)
Particle Filtration Efficiency (PFE)
Advanced Production Lines
Countries Exported Globally
How automation, geographical cluster advantages, and advanced raw material control guarantee uninterrupted supply for global healthcare networks.
Leveraging 5 fully automatic and 12 semi-automatic mask production machines, our manufacturing facility operates around the clock. This layout enables us to maintain a stable output, minimizing lead times even during seasonal demand spikes.
By securing direct partnerships with local premium meltblown non-woven and polypropylene manufacturers, we insulate our production schedule from raw material shortages, ensuring consistent filtration quality and stable cost structures.
Every batch of medical supplies undergoes rigorous inspection using automated optical systems integrated directly into the production lines. This is paired with manual laboratory checks to verify that every mask achieves up to 99% BFE and PFE protection.
Traditional procurement models often involve multiple layers of brokers, brokers' agents, and local distributors. This not only inflates prices but also dilutes the traceability of critical medical assets. When a hospital buys supplies, they must know the exact origin of the non-woven fabric, the filtration efficiency test parameters, and the compliance certificates associated with that specific production lot.
At Zhejiang DrSharpe Health Co., Ltd., we operate as a dedicated manufacturer and global exporter, establishing direct technical communication with procurement offices. This eliminates communication lag, facilitates custom OEM/ODM packaging requests, and ensures that all technical documentation—such as CE certification, US FDA registrations, and TUV test data—is transmitted directly from our quality assurance department to your compliance team.
Zhejiang DrSharpe Health Co., Ltd. is a professional manufacturer and global supplier specializing in disposable medical and healthcare products, especially high-quality face masks and protective solutions.
With strong manufacturing capabilities, advanced production technology, and strict quality management, DrSharpe is committed to providing safe, reliable, and comfortable healthcare products for customers worldwide.
Our manufacturing plant is equipped with 5 fully automatic mask production machines and 12 semi-automatic mask production machines, supported by an experienced production and service team. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to markets including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
A transparent look inside our state-of-the-art cleanrooms and automated packaging lines in Zhejiang, China.
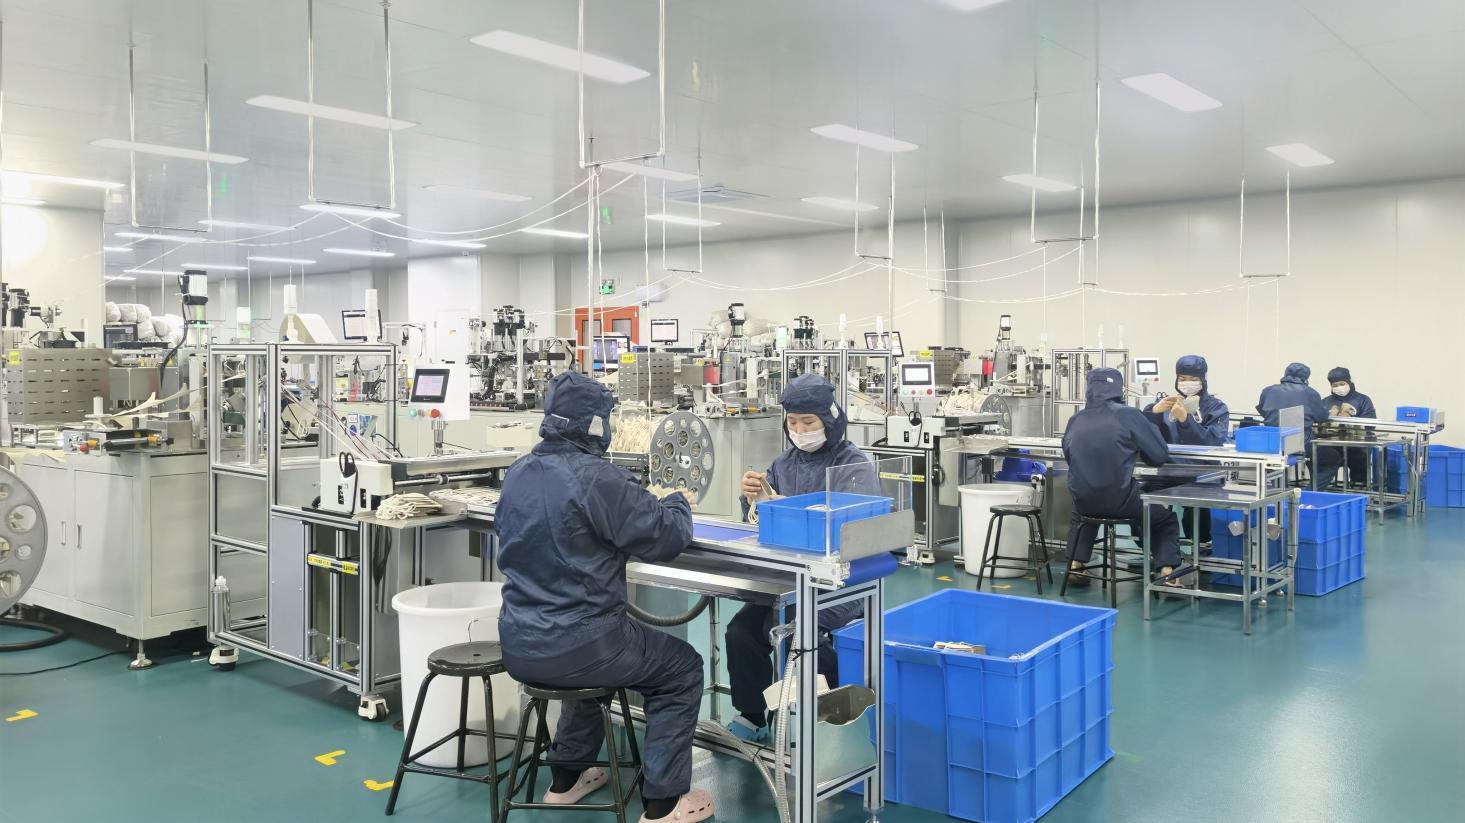
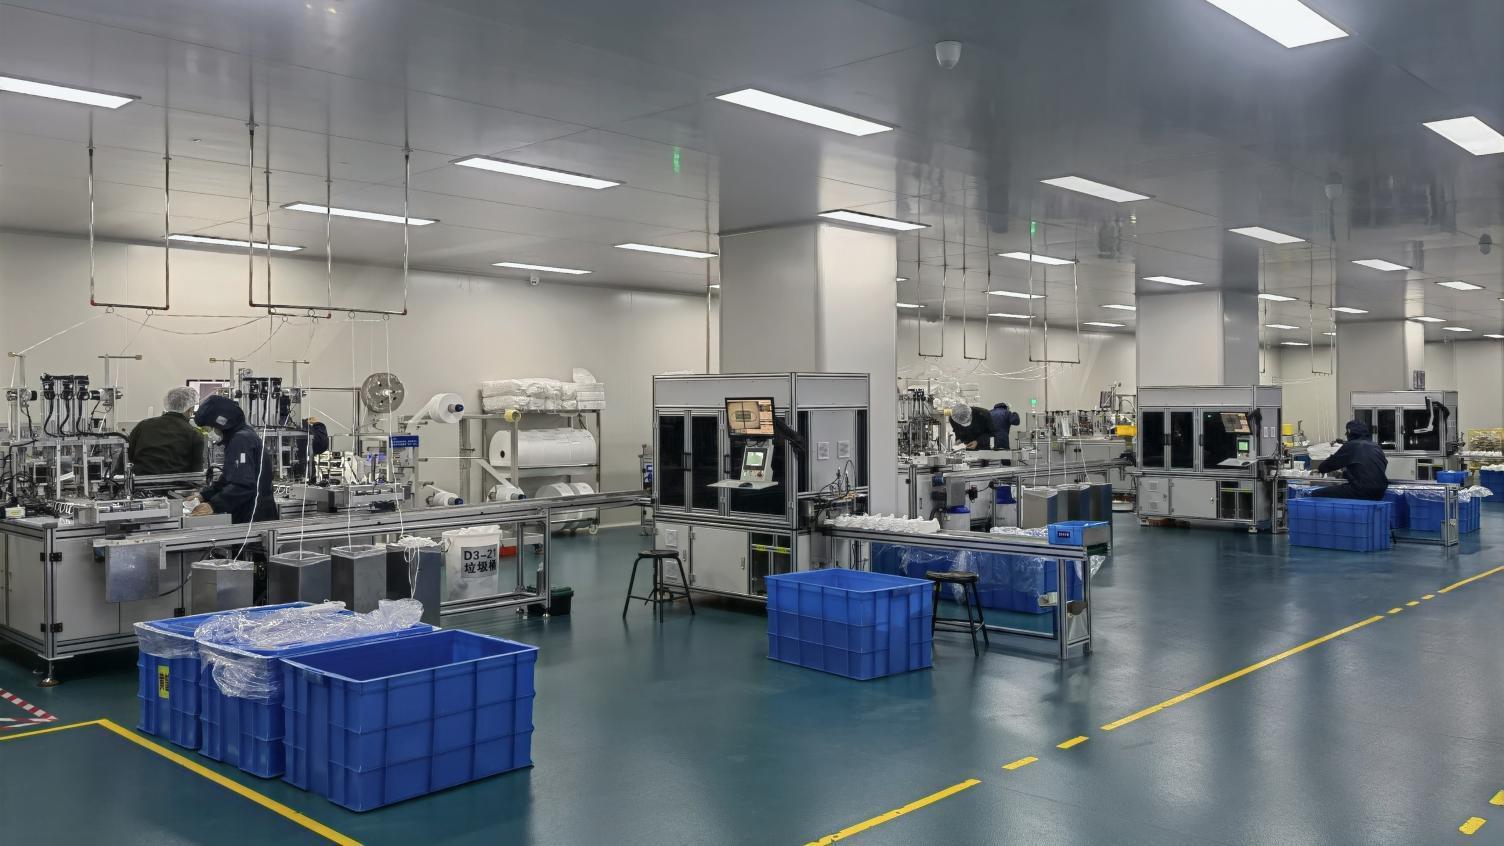
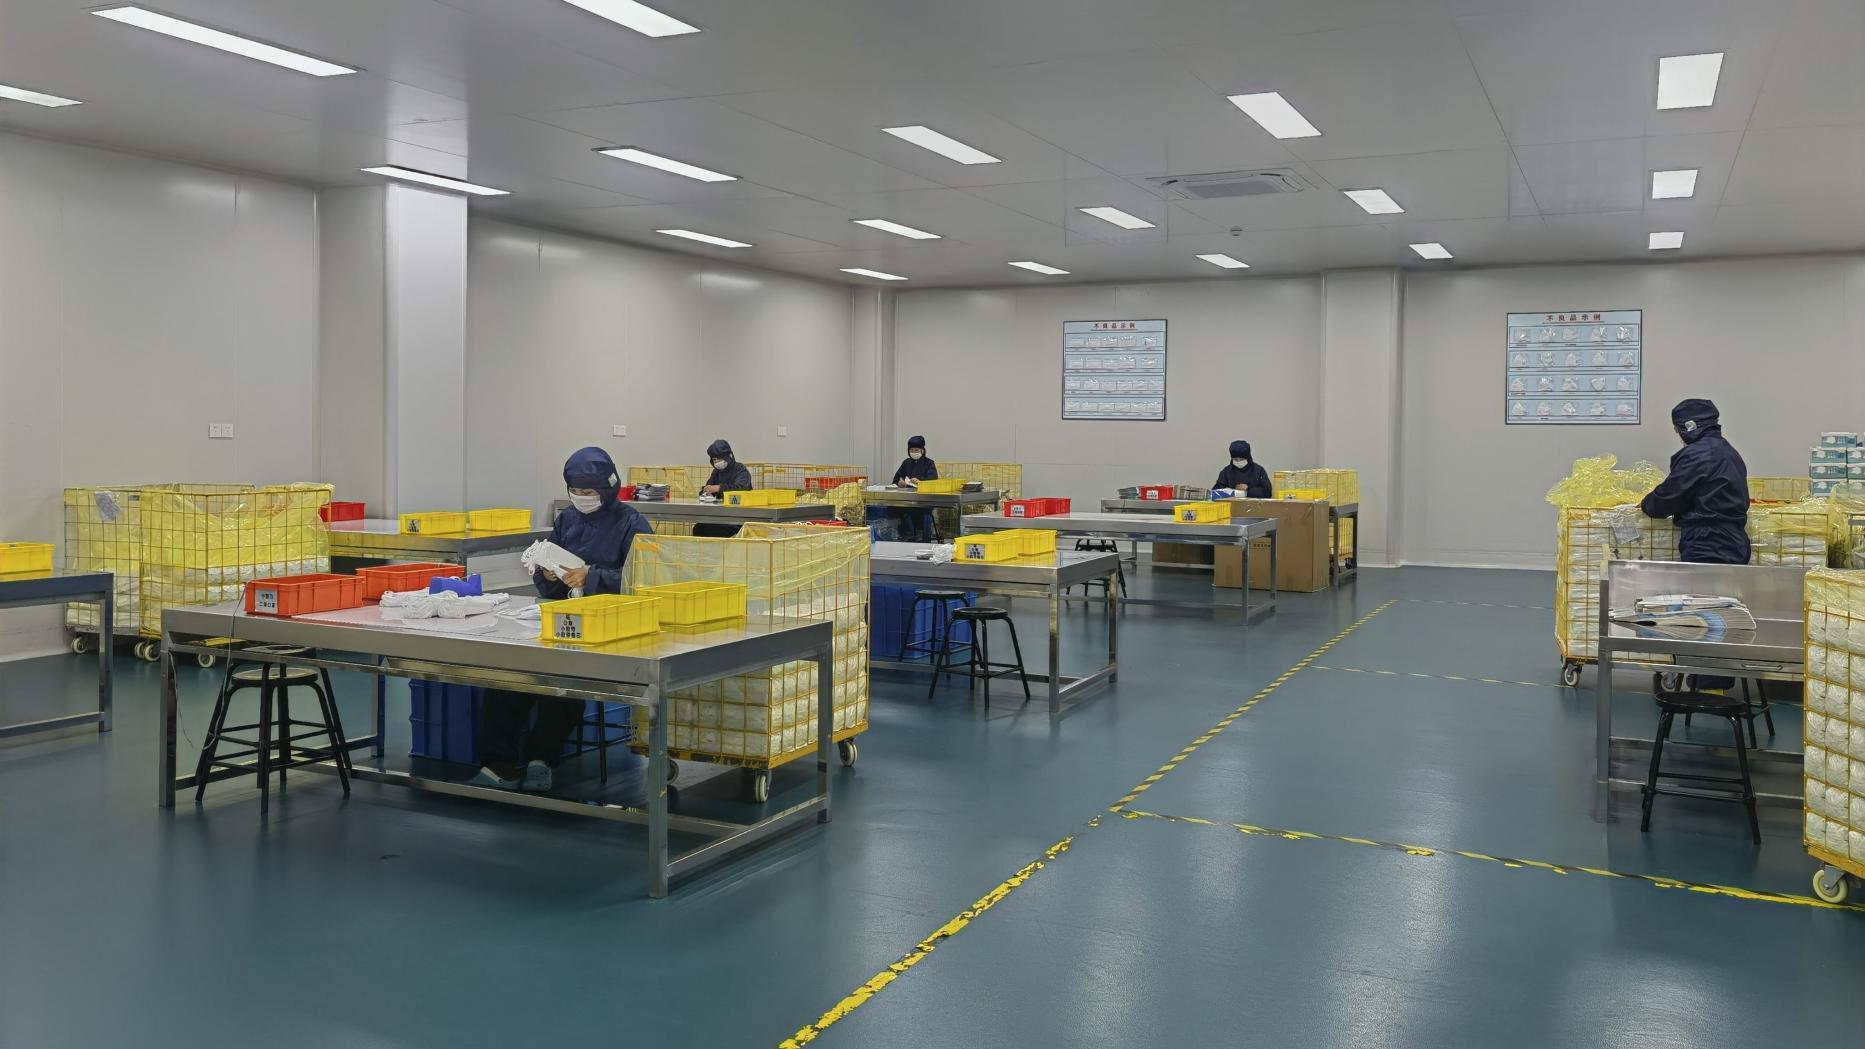
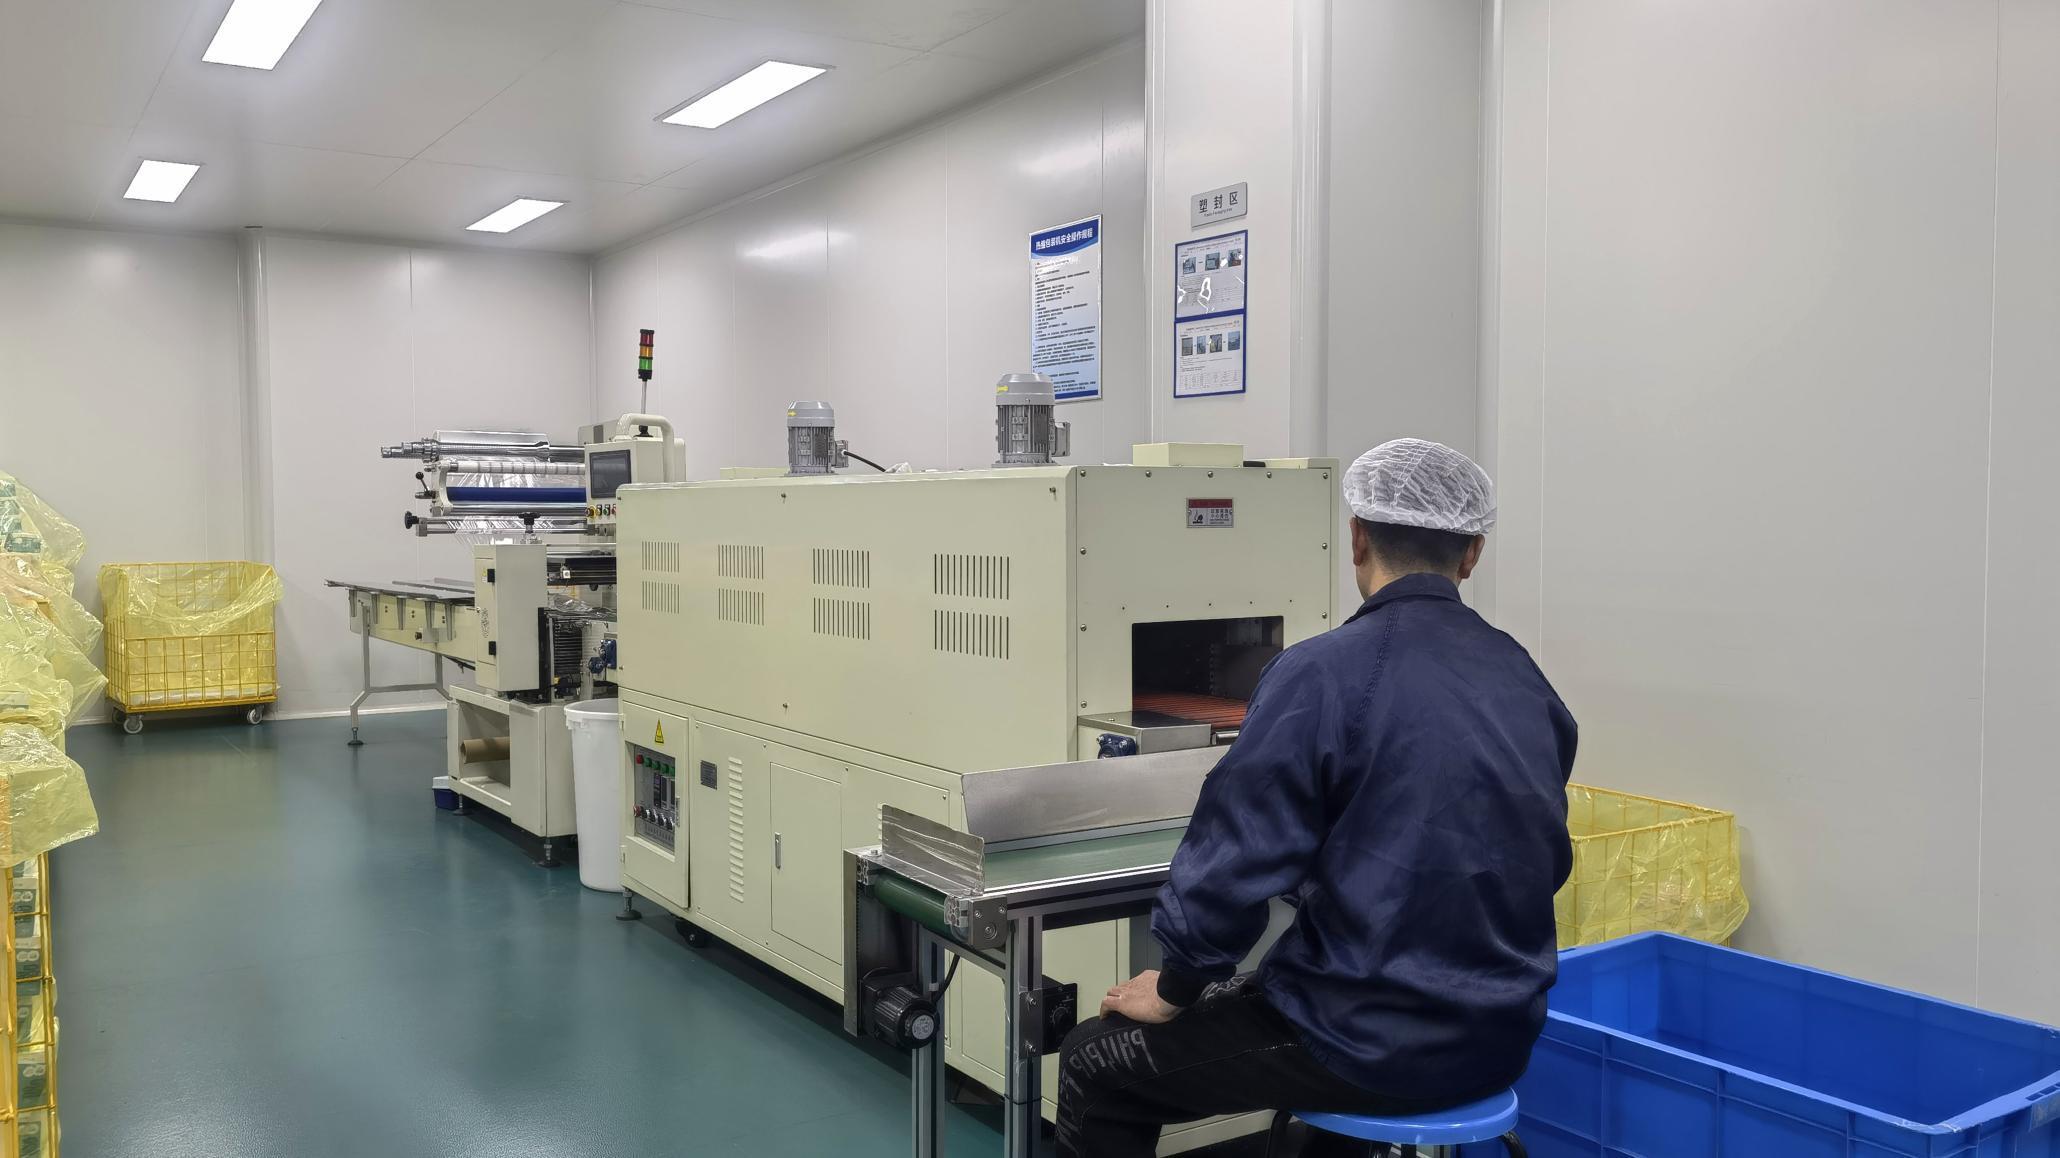
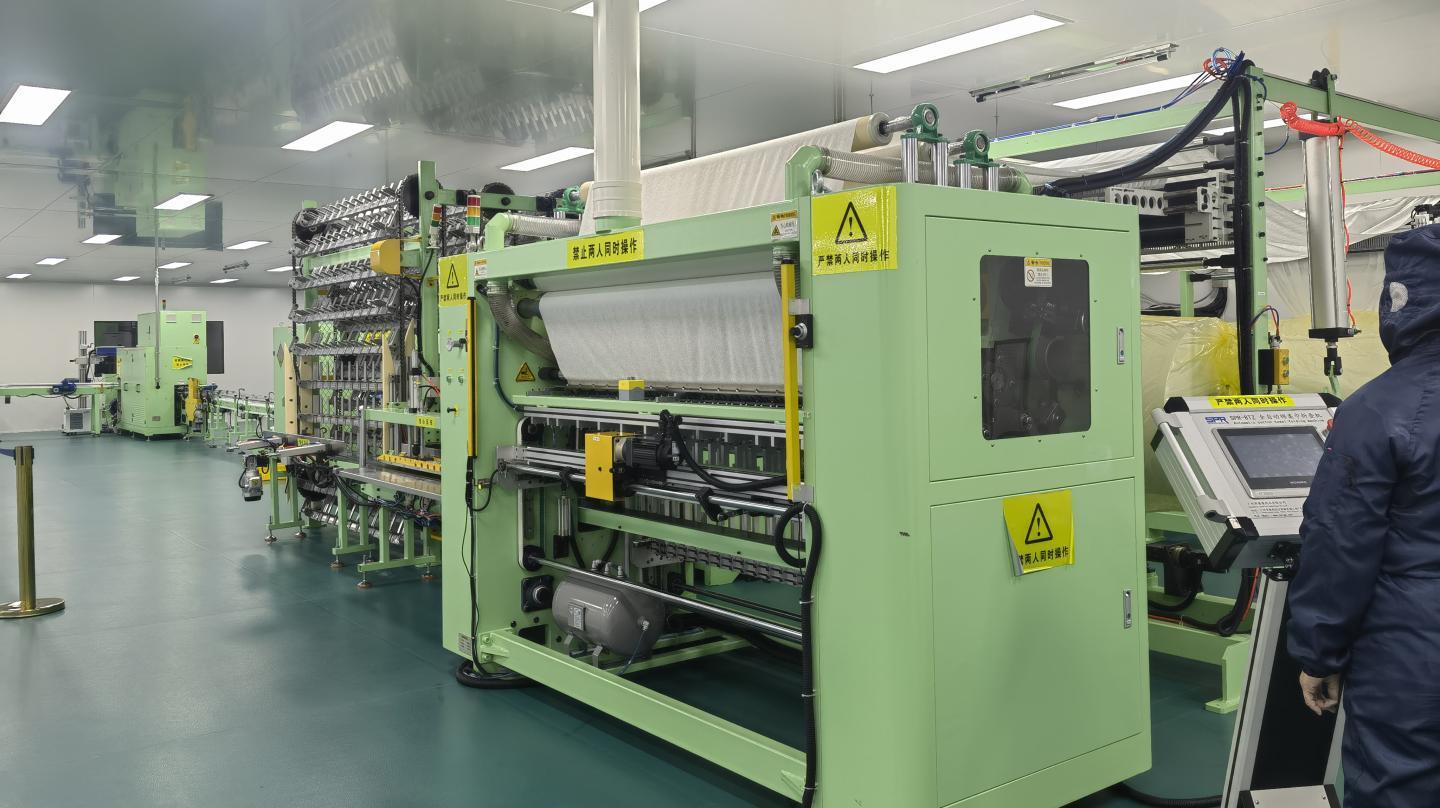
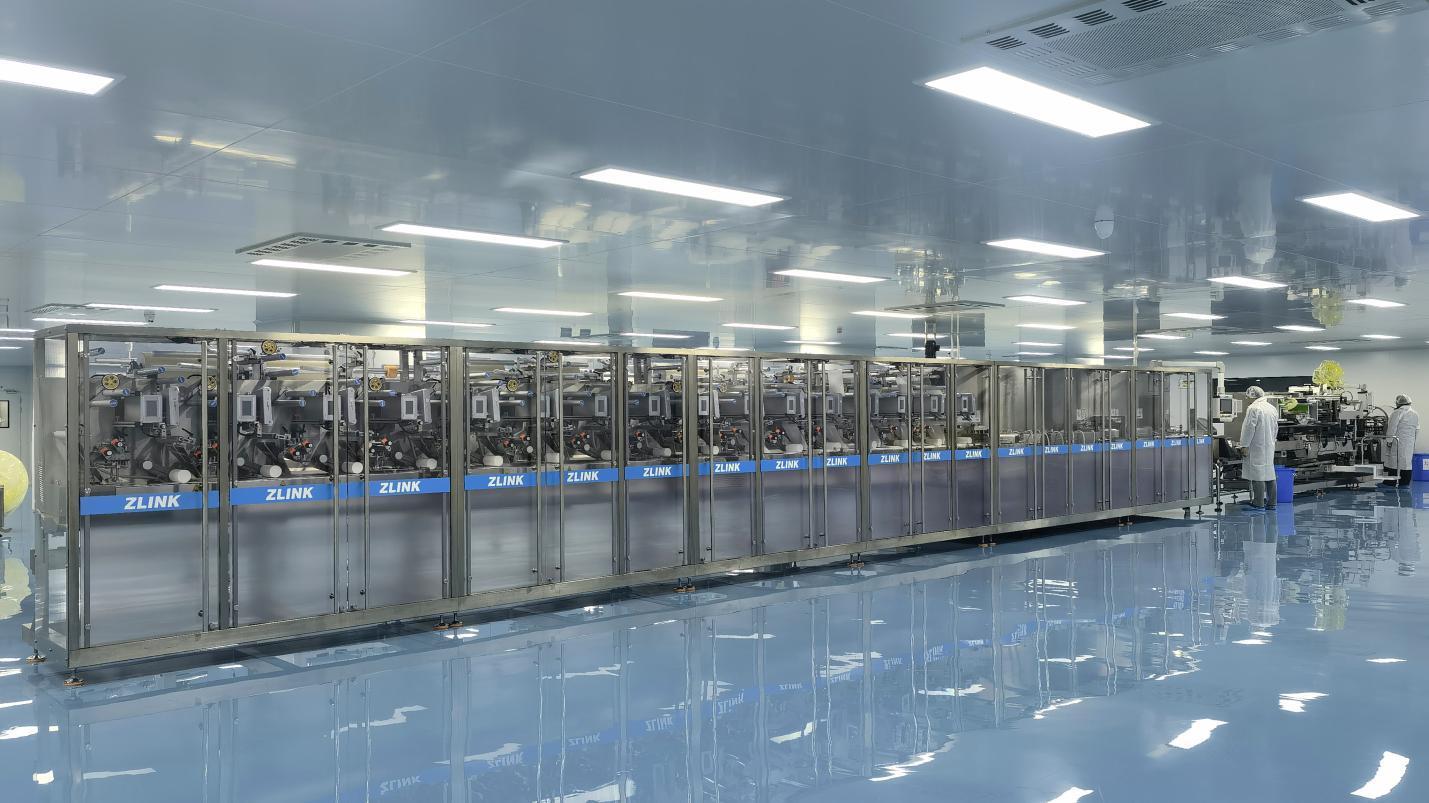
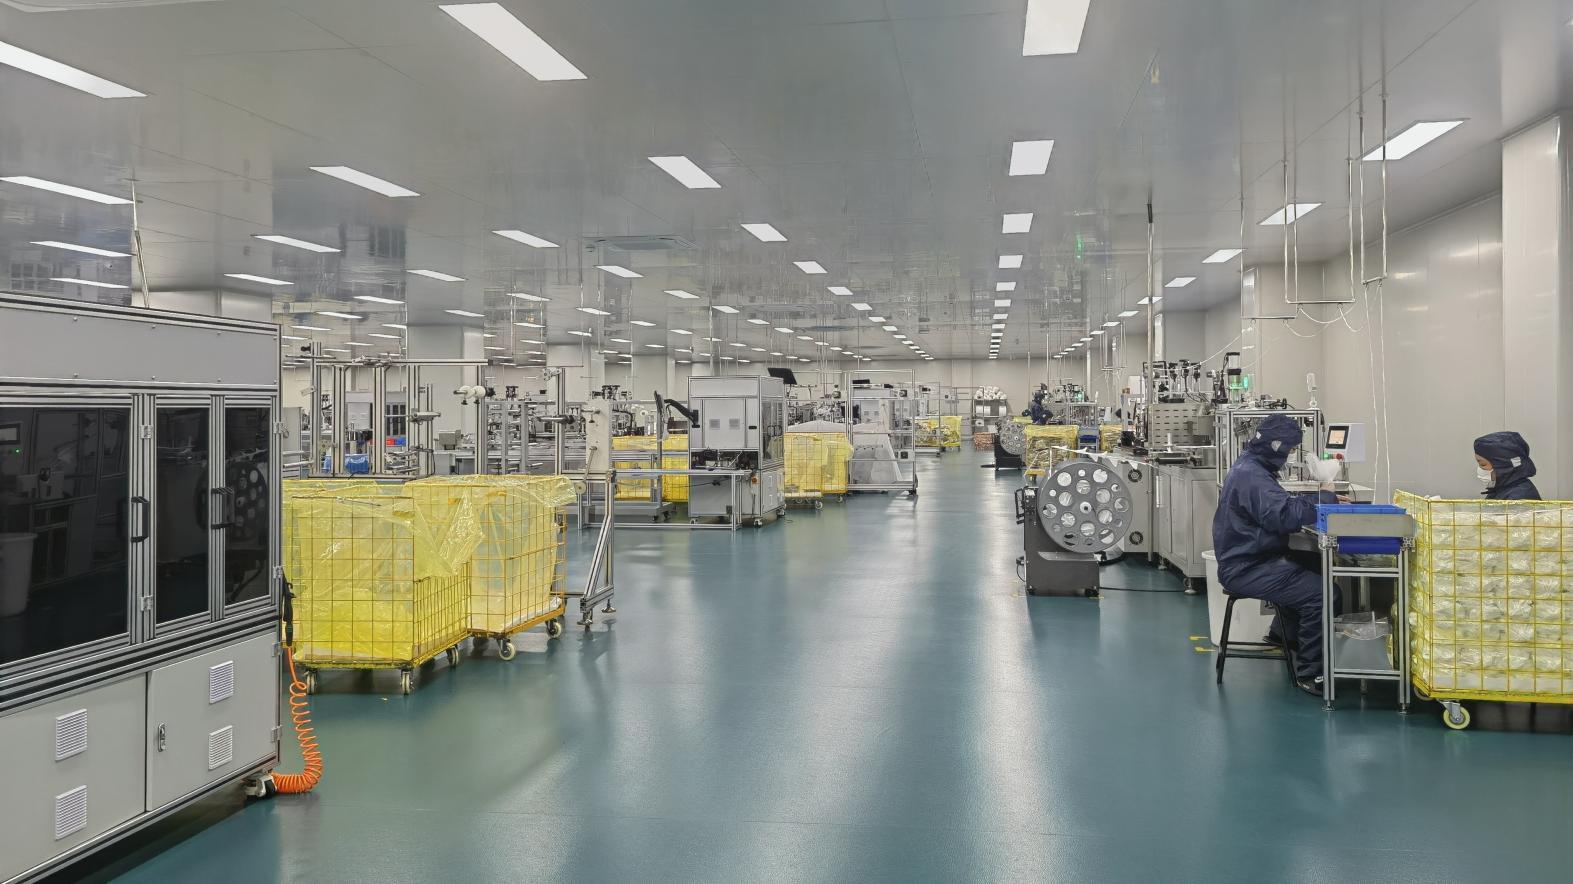
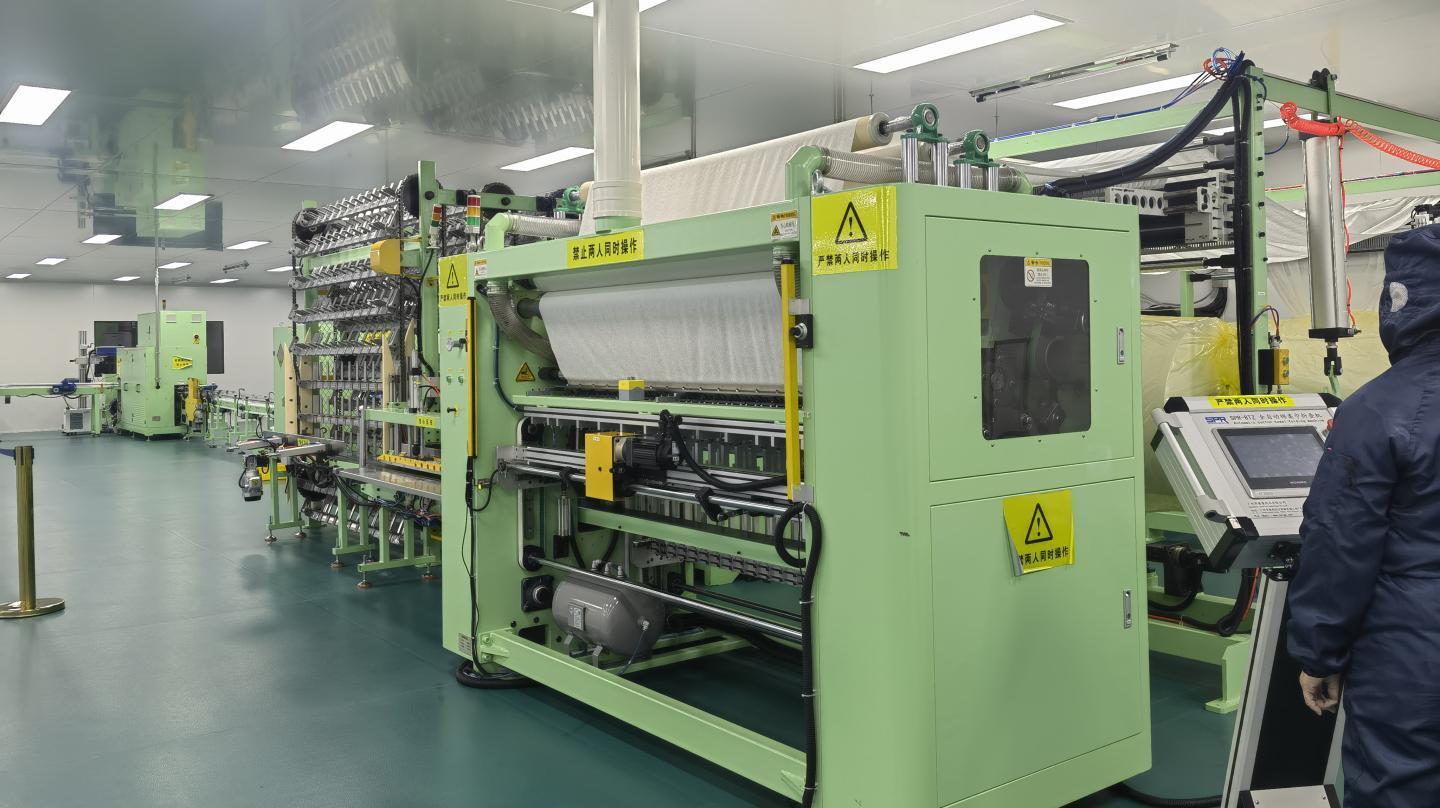
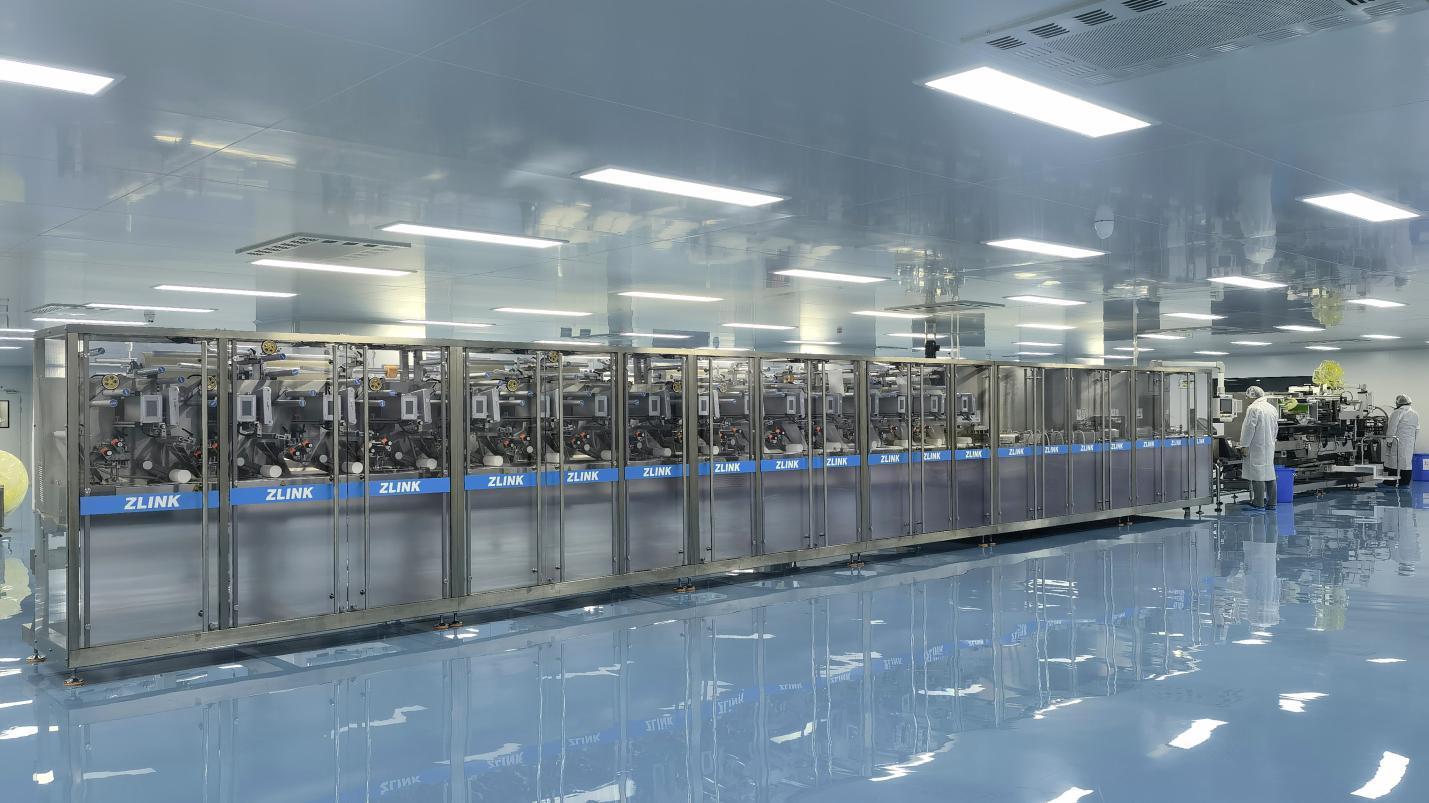
Procuring Suministros Hospitalarios for markets like Mexico, Brazil, Colombia, Germany, and the UK requires a granular understanding of regional regulatory landscapes. For Spanish-speaking regions, B2B buyers must navigate complex import regulations enforced by authorities such as COFEPRIS in Mexico, ANVISA in Brazil, or ISP in Chile. Our regulatory affairs team at Zhejiang DrSharpe Health Co., Ltd. coordinates direct verification files, localized packaging text, and certificate authentications to guarantee smooth customs clearances.
A medical face mask is not simply pieces of fabric stitched together. It is a highly engineered, three-layer barrier system designed to prevent fluid cross-contamination while preserving normal gas exchange (breathability). Here is a breakdown of the materials utilized in our facility:
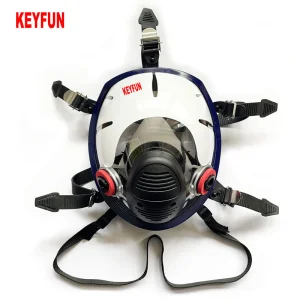
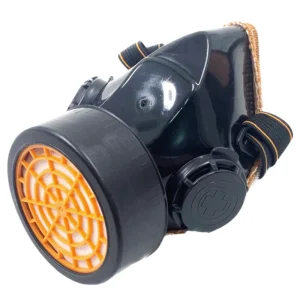
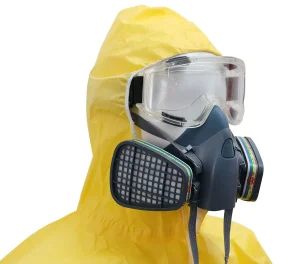
Understanding that hospital staff, first responders, and laboratory technicians face diverse occupational hazards, we have expanded our manufacturing catalog. Beyond typical 3-ply surgical masks, we manufacture high-performance safety gear, including gas masks with activated carbon filters, silicone half-face respirators, and full-facepiece shields. These solutions comply with rigid industrial standards such as EN 140 and EN 14387, offering protection against toxic vapors, chemical paint fumes, and hazardous airborne particulates in clinical laboratories and sanitization environments.
Discover our specialized protective respirators, pediatric face masks, and clinical-grade breathing supplies built to meet global industrial and healthcare specifications.
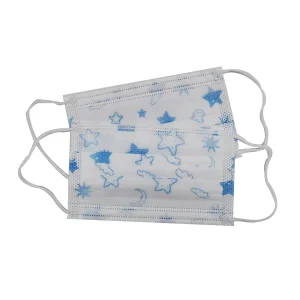
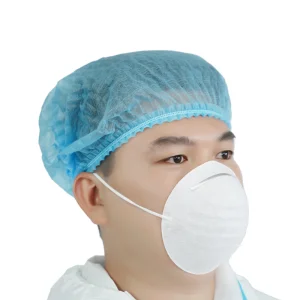
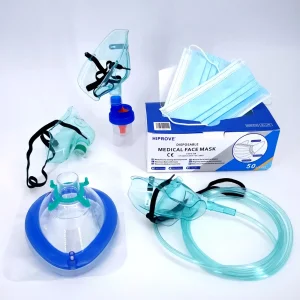
Detailed explanations regarding global medical standards, factory capabilities, and regulatory compliance to assist B2B purchasing managers.