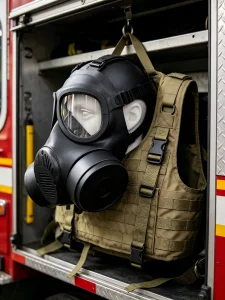
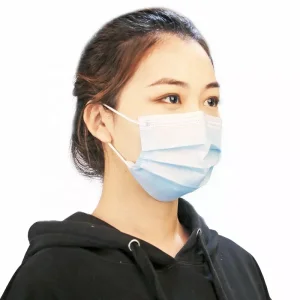
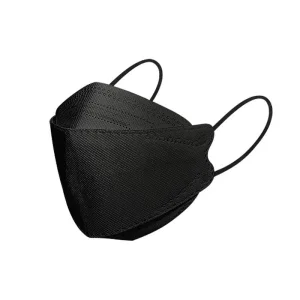
DrSharpe Health
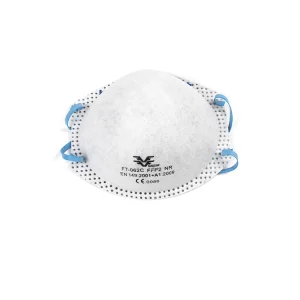
Explore our top-tier surgical supplies, specialized respirators, and respiratory therapy materials designed under strict compliance protocols.
Pioneering standard-compliant personal protection equipment and sanitization materials for healthcare operators.
Zhejiang DrSharpe Health Co., Ltd. stands as an authoritative force, functioning as a premier manufacturer and global supplier specializing in premium medical, surgical, and therapeutic health materials. With deep domain knowledge, we bridge the gap between heavy industrial output and strict hospital hygiene regulations. By addressing complex challenges in global health procurement, we ensure our global distributors receive top-tier, compliant solutions.
Through active research and development, we formulate material configurations that target particle barrier performance while keeping breathing resistance to a minimum. Our output is anchored in a highly organized production cycle that integrates rigorous quality management and technological evolution to deliver stable health products worldwide.
We source raw components under rigorous auditing systems to construct multi-layered defensive materials, utilizing hydrophobic spunbond layers, high-dust-holding meltblown membranes, and soft, non-irritant inner layers. Through this structured method, our masks and filtration systems achieve a Bacterial Filtration Efficiency (BFE) exceeding 99% and a Particle Filtration Efficiency (PFE) exceeding 99%.
Our commitment to quality extends from simple protective structures to complex devices. Every run undergoes particle testing, physical stress inspections, and bio-burden evaluation. This rigorous process allows us to proudly serve markets including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
Unpacking the rapid shifts in regulatory frameworks, bio-materials science, and microfiltration demands.
Modern healthcare systems are demanding higher performance from non-woven medical textiles. Traditional filtration relies heavily on basic physical trapping, which often increases breathing resistance and tires healthcare workers out. The industry is rapidly shifting toward corona-charging technology. This process embeds stable electrostatic charges deep inside the polypropylene meltblown matrix. As a result, sub-micron viral and bacterial particulates are actively pulled out of the air stream and trapped, maintaining 99% filtration efficiency without compromising breathability.
Single-use masks and medical protective supplies generate substantial plastic waste. Forward-thinking manufacturers are actively researching and implementing bio-based polymers like Polylactic Acid (PLA) and PBS co-polyester blends. By developing medical-grade PLA fibers that degrade under standard industrial composting parameters, factories are addressing ecological concerns while maintaining the strict bio-safety levels required in clinical settings.
Ensuring consistent supply streams, navigating import tariffs, and mitigating logistics risks.
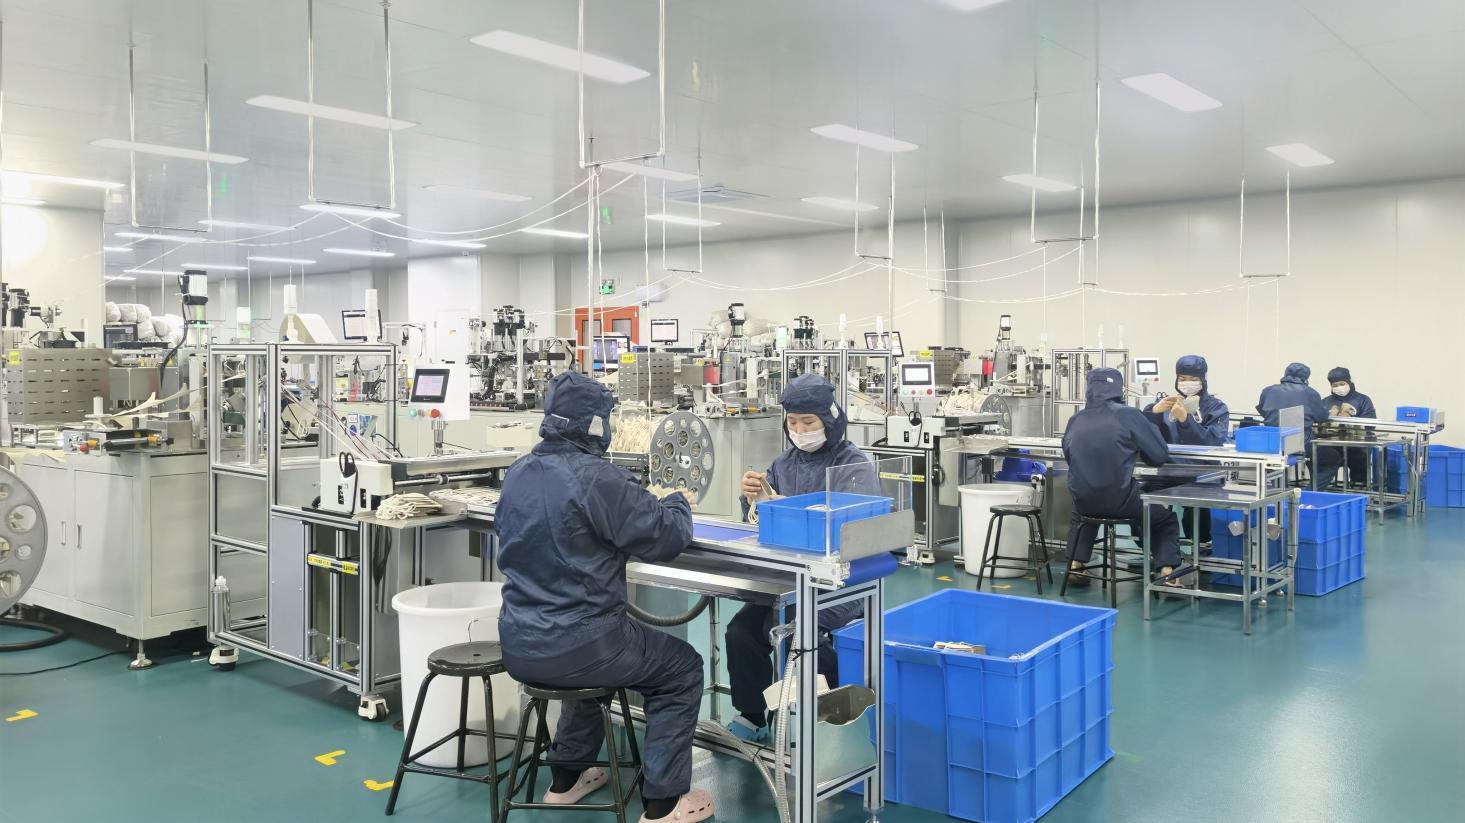
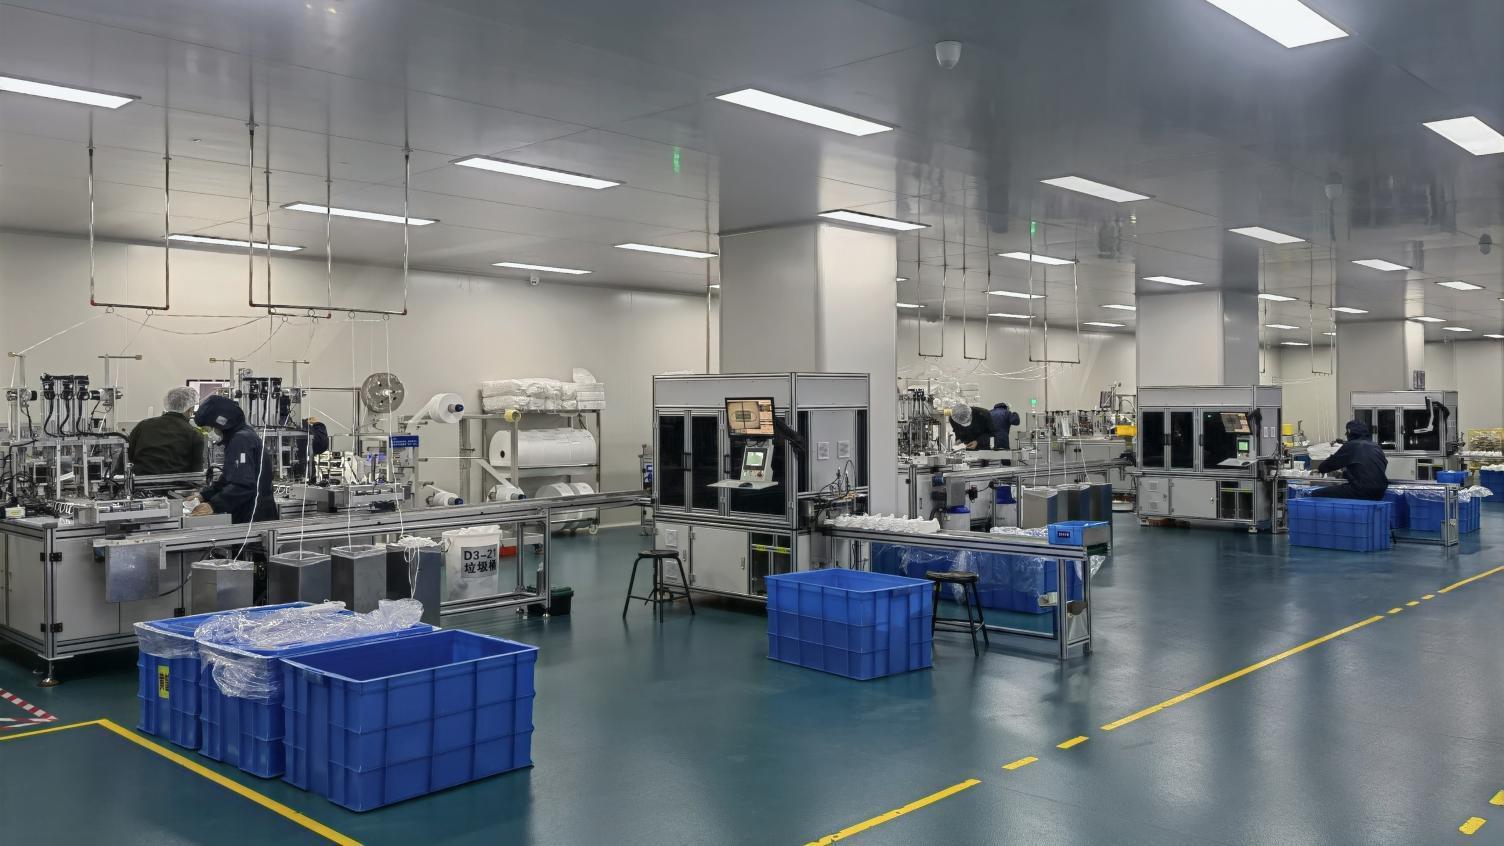
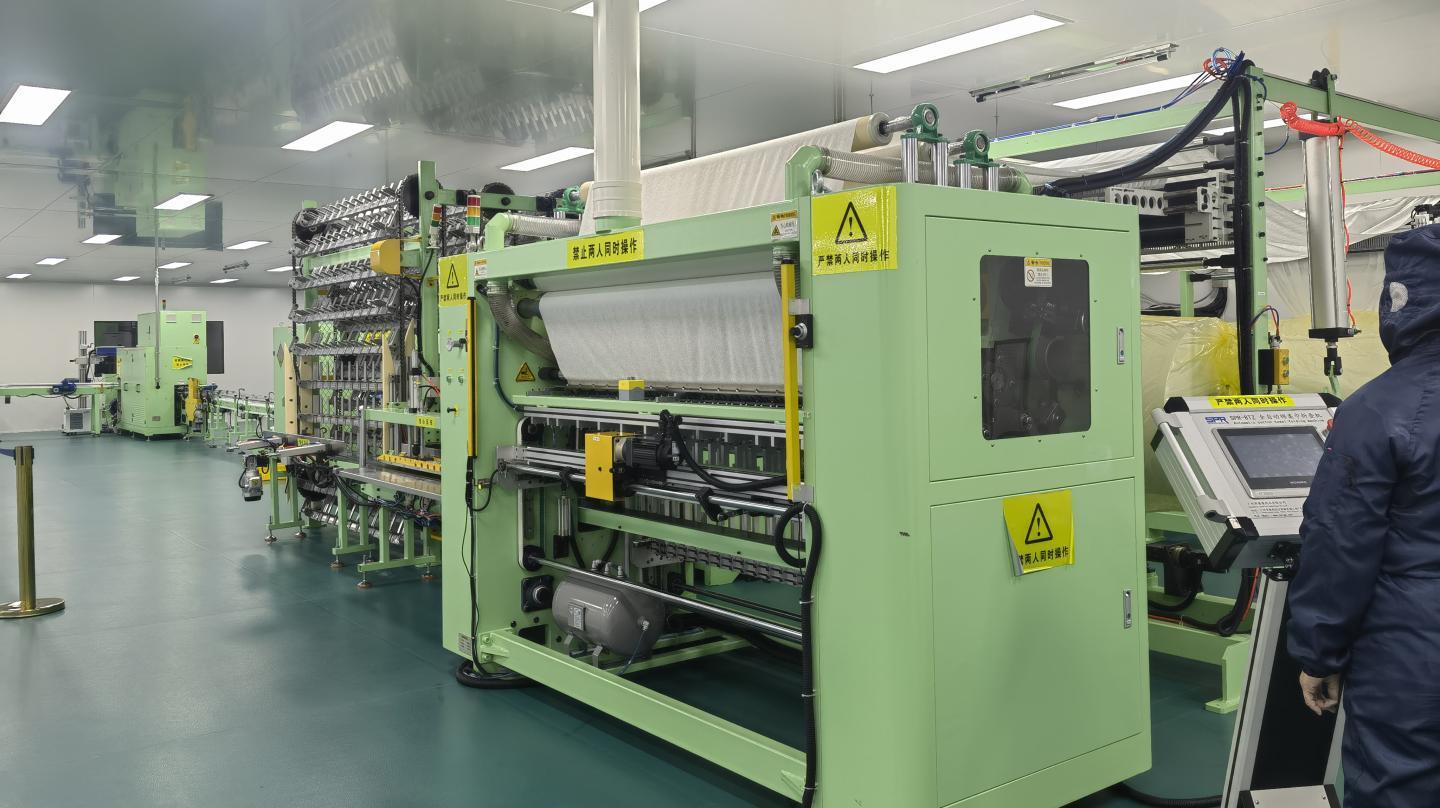
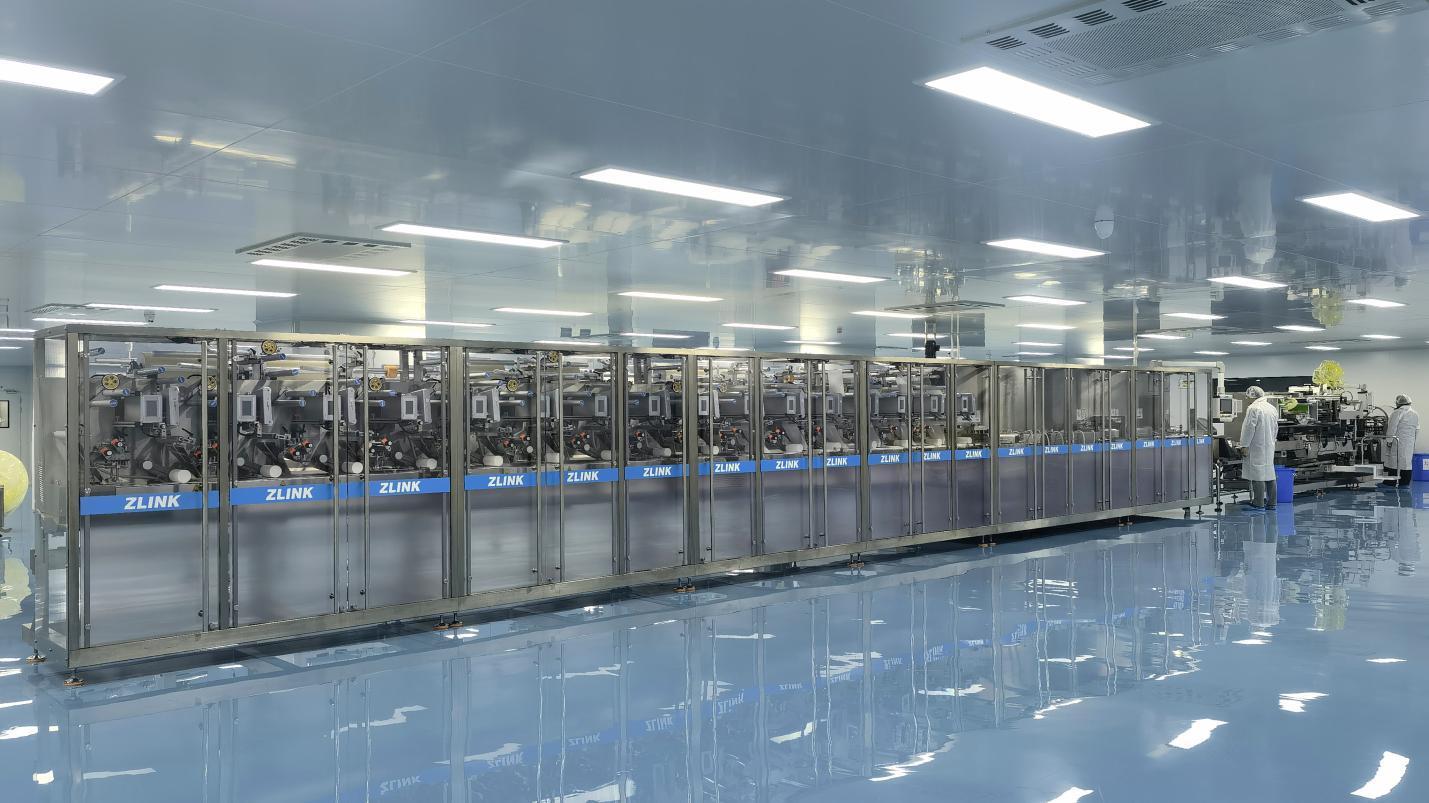
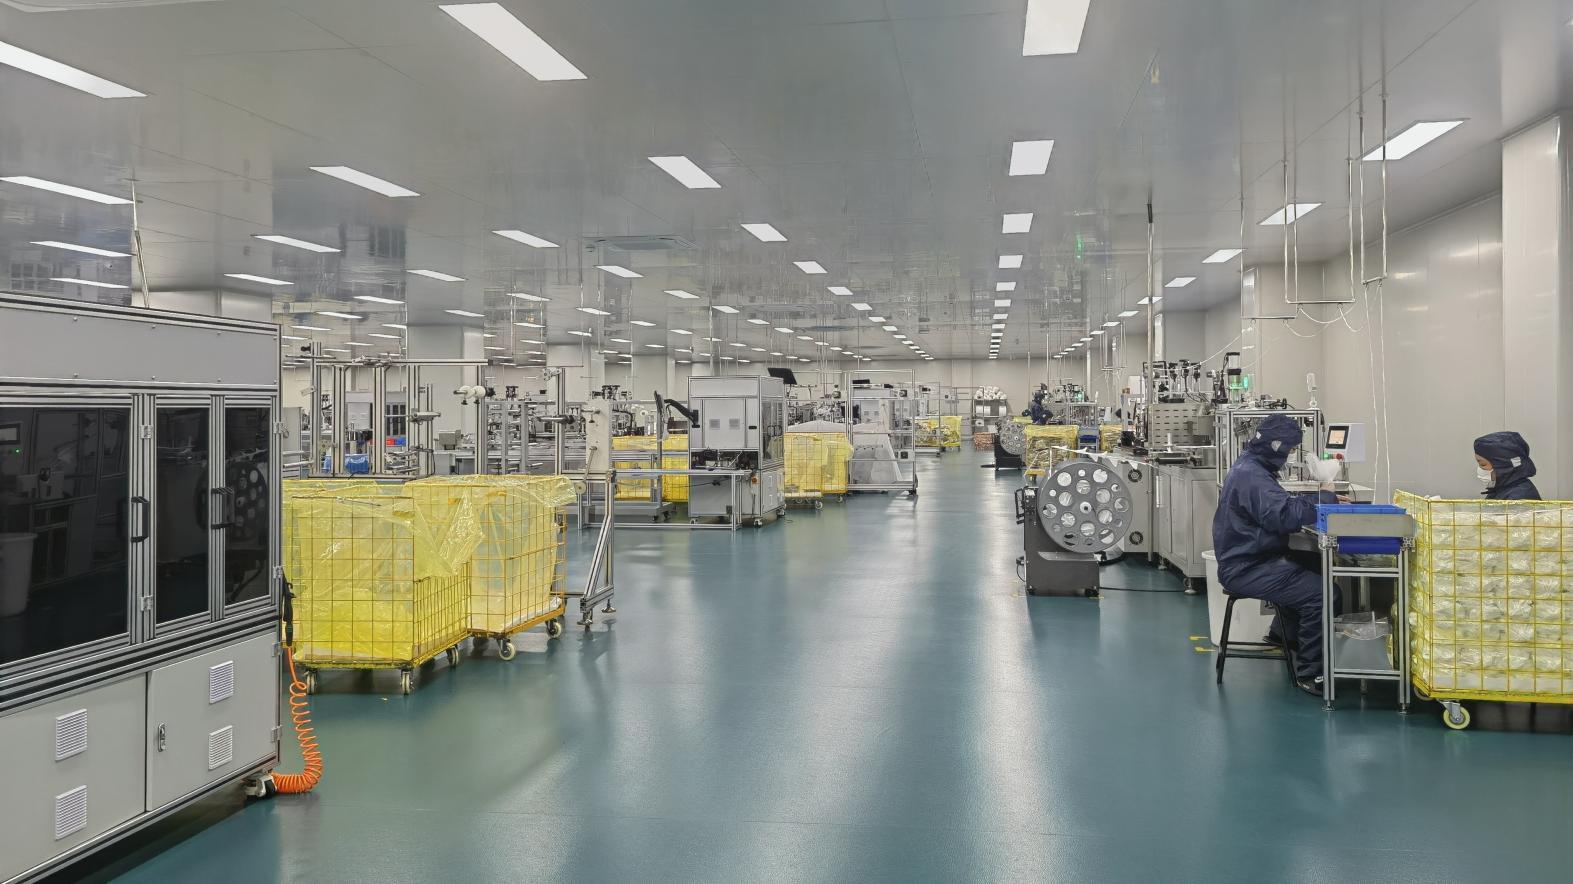
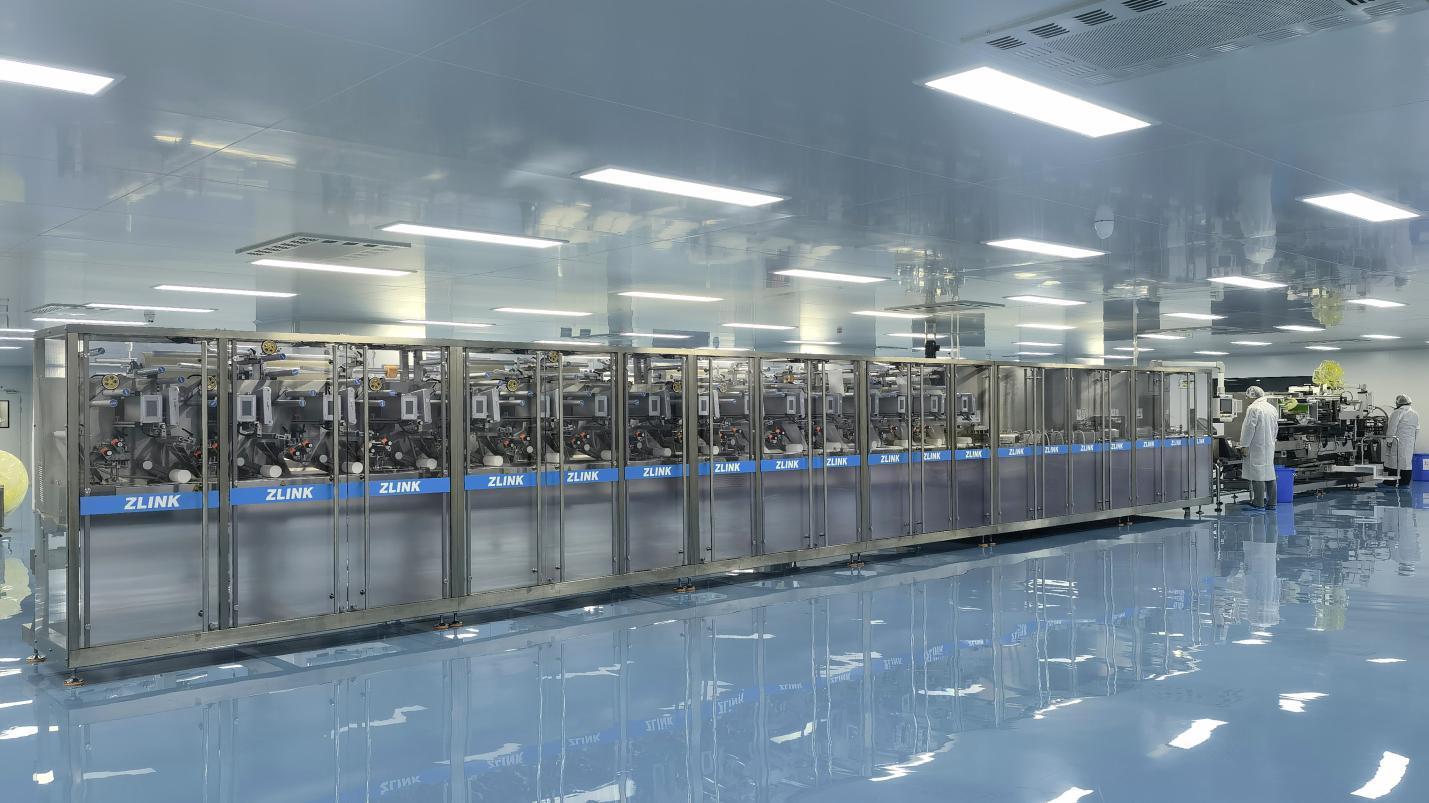
Global distributors cannot afford supply chain interruptions. Working directly with an enterprise-grade factory like Zhejiang DrSharpe Health Co., Ltd.—which houses 5 fully automatic and 12 semi-automatic production machines—guarantees consistent volume scaling. Our manufacturing setup allows us to quickly pivot production schedules to meet sudden surges in demand without lowering quality thresholds.
Shipping healthcare materials requires rigorous cargo security and proper customs clearance documentation. A solid manufacturing partner must provide complete visibility, using standardized packing lists, certificates of origin, and transparent transport routing. This structured handling helps avoid customs delays at major ports of entry in Europe and North America.
From operating theatres to heavy chemical filtration and light therapy skincare.
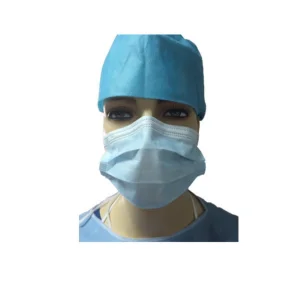
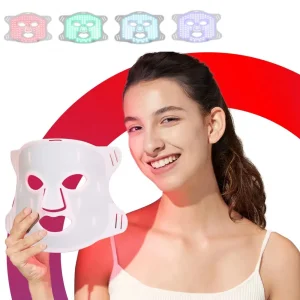
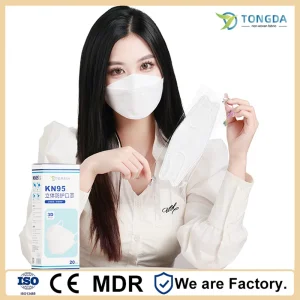
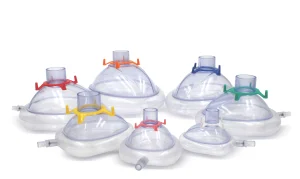
Health materials, or materiales de salud, are no longer limited to basic medical drapes and earloop masks. Modern healthcare organizations require an integrated ecosystem of protection that spans multiple distinct clinical and civil application fields:
Meeting global quality control standards to facilitate smooth customs clearance and compliant market distribution.
Compliance Matrix: Different markets enforce varying legal gateways. A product cannot be sold in the US without FDA 510K clearance or EUA status, nor in Europe without conforming to the Medical Device Regulation (MDR) and bearing a valid CE mark.
Zhejiang DrSharpe Health Co., Ltd. maintains a robust regulatory framework. Our products comply with international standards and have obtained certifications including CE, US FDA, and US EUA. In addition, our manufacturing facilities operate under ISO certification guidelines. This rigorous quality management ensures that every batch of surgical face masks, N95 respirators, and therapeutic silicone devices meets the legal and safety requirements of destination ports worldwide.
A preview of upcoming innovations in smart protective equipment and bio-compatible materials.
Integrating chemical and humidity sensors directly into the non-woven layers of respirators to alert users when a filter is saturated and needs replacement.
Shifting from traditional meltblown structures to electrospun polymeric nanofiber webs, reducing weight while offering superior filtration efficiency.
Incorporating natural, bio-active agents like zinc oxide nanoparticles directly into non-woven fibers to kill pathogens on contact.
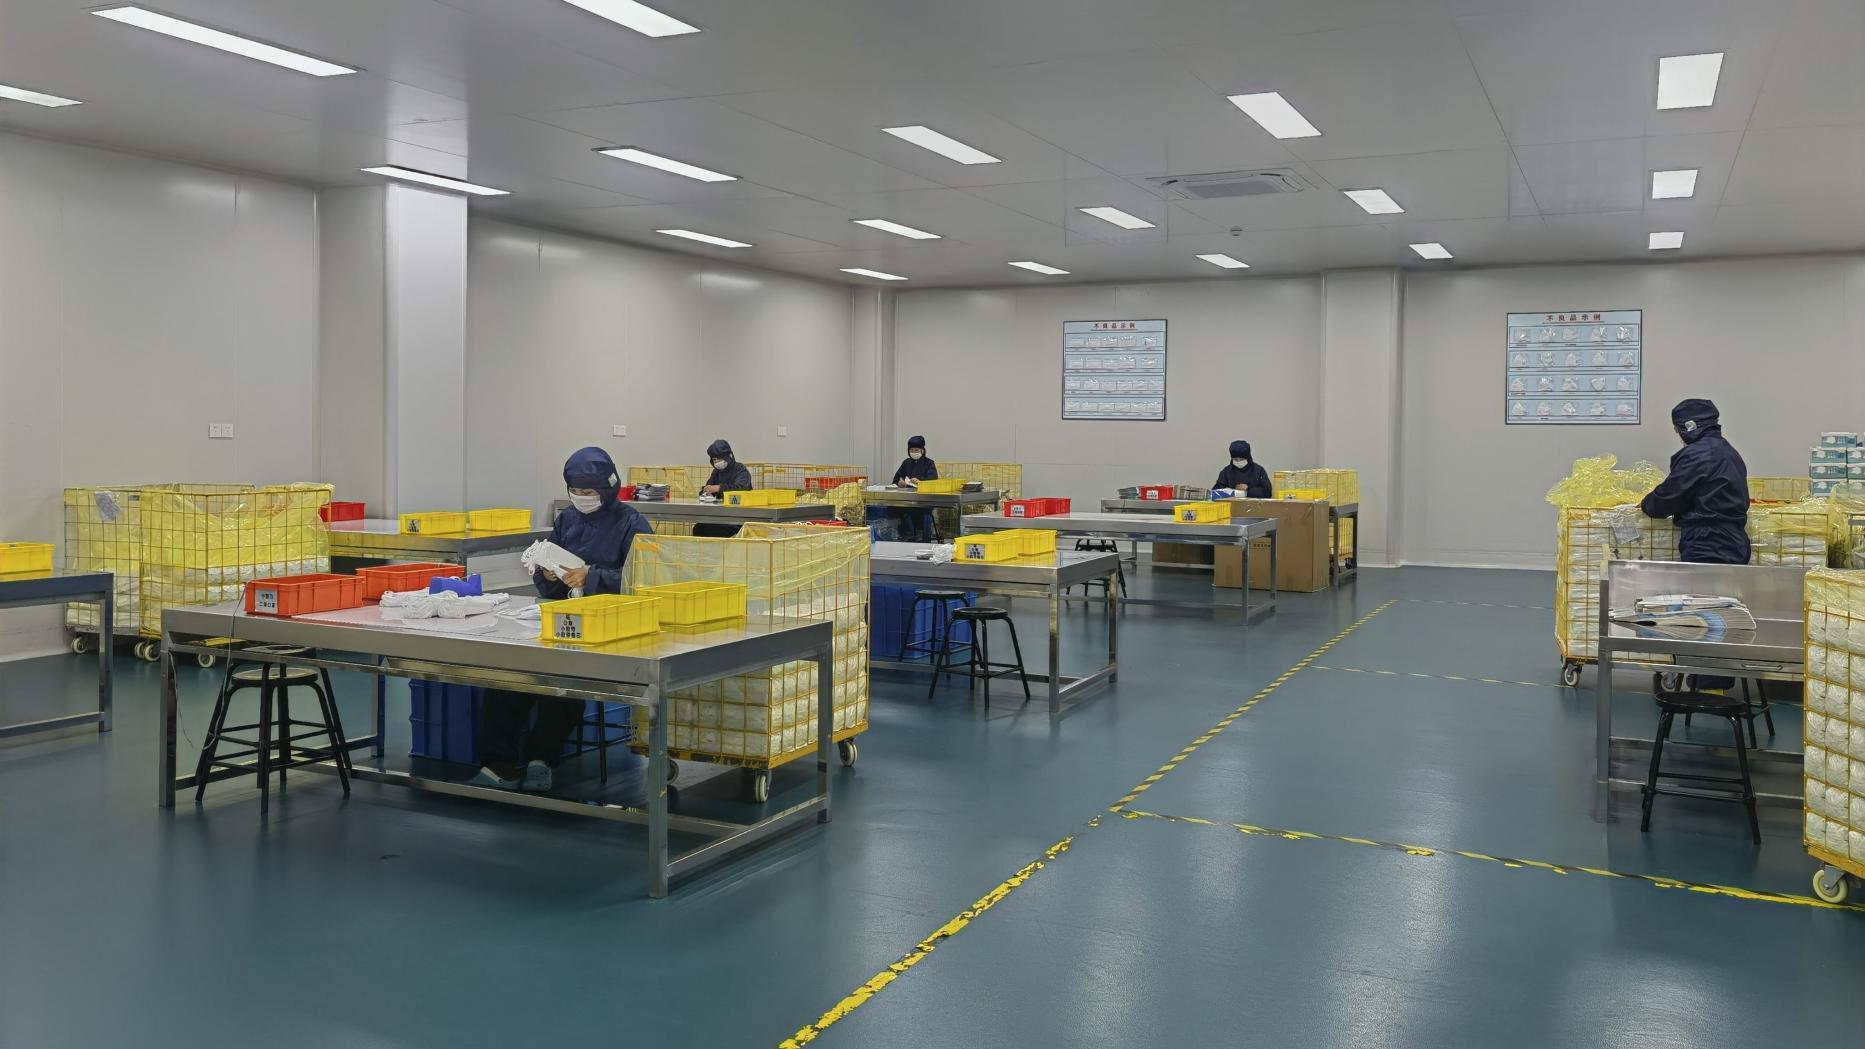
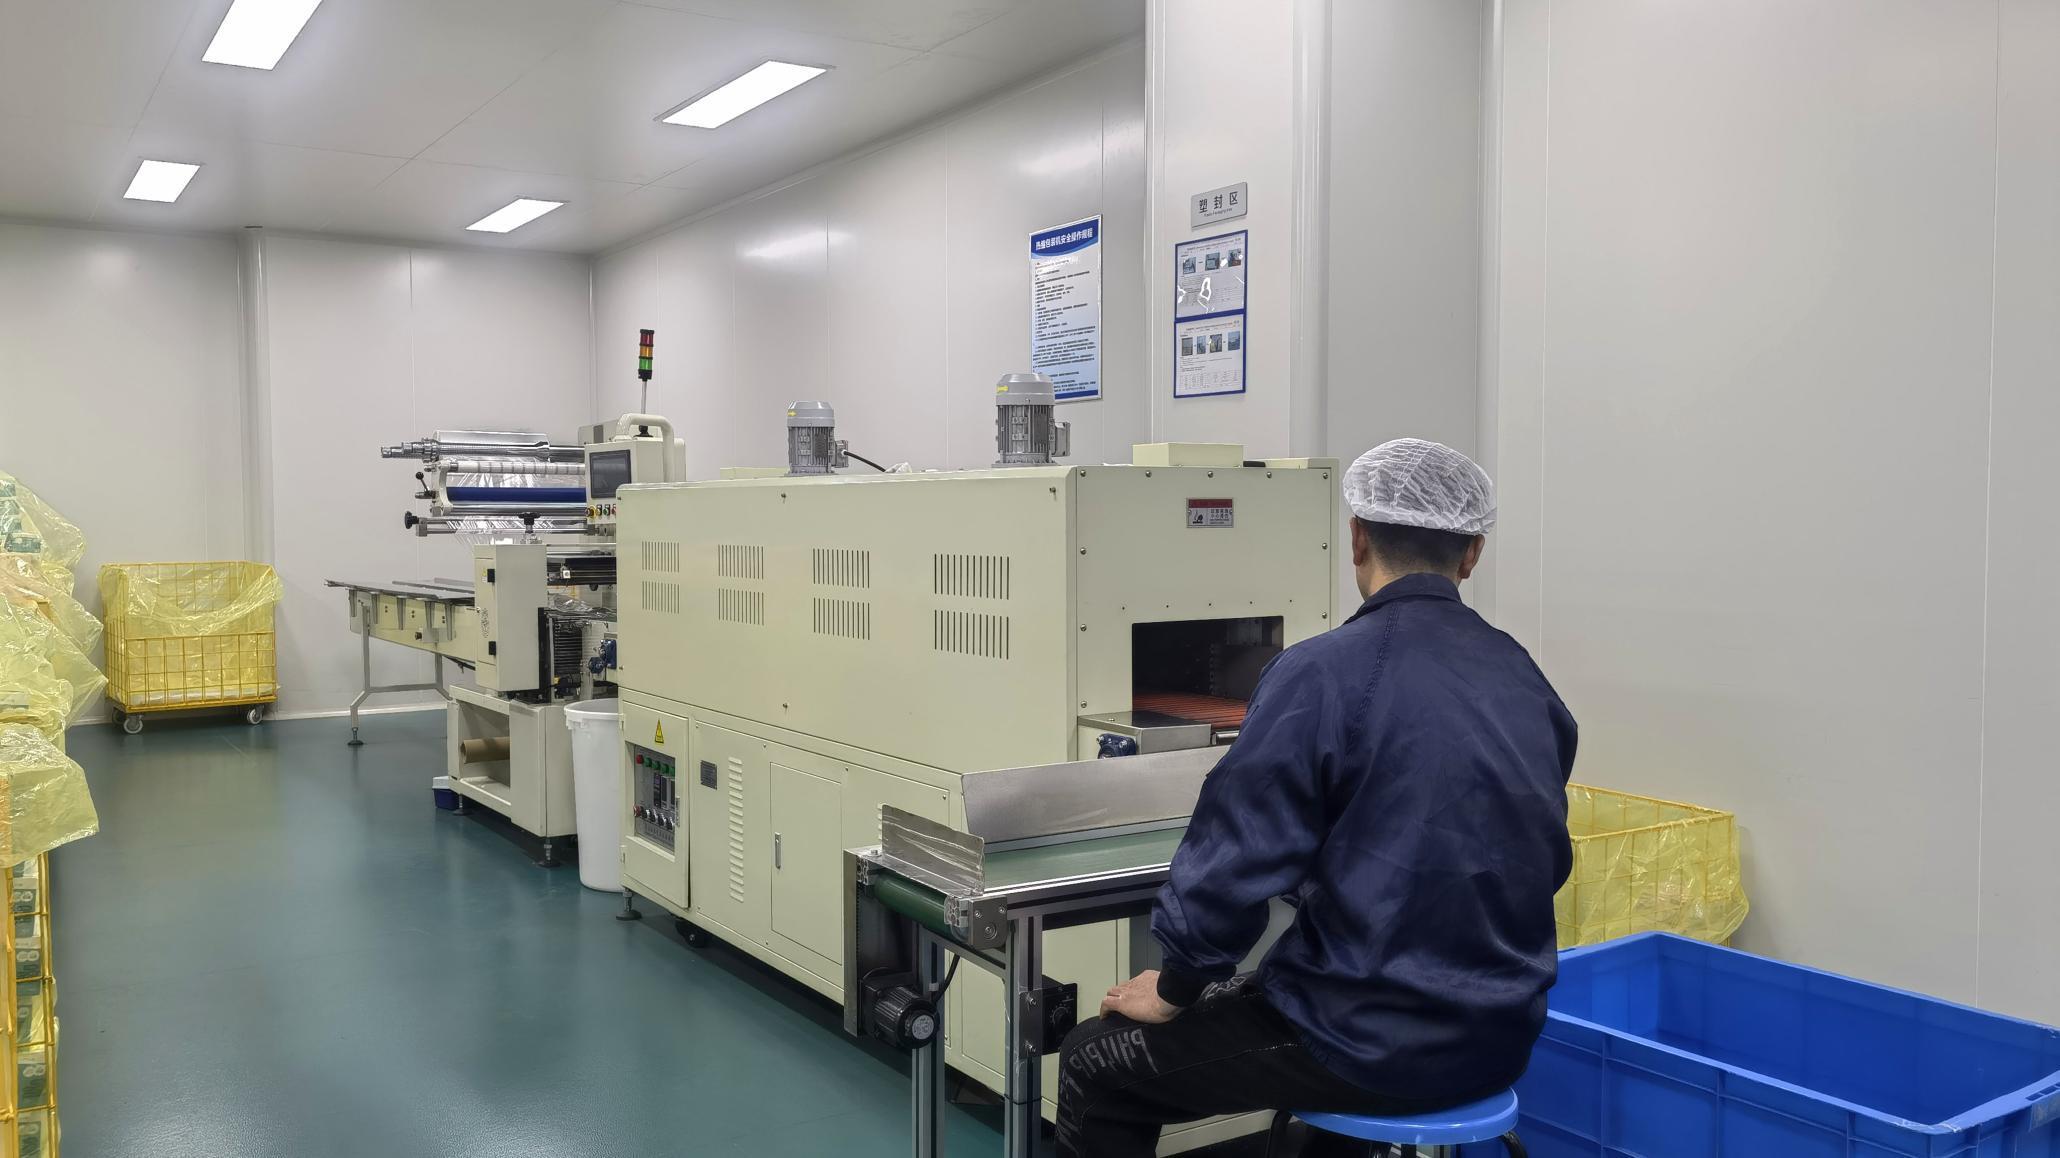
Inside our state-of-the-art production rooms. From high-speed automatic masking lines to manual inspection and sterile packing bays.
Addressing the most critical compliance, technical, and logistics questions raised by international medical device buyers.
From daily protective wear to advanced light therapy technology and high-efficiency carbon filters.