DrSharpe Health
Direct from our advanced production facilities. High-efficiency respiratory, personal protection, and clinical safety solutions complying with global regulatory standards.
How regulatory evolution and technical apparel engineering shape safety compliance across high-risk sectors.
In modern industrial operations, lower body protection is a critical element of safety protocols. Pantalones de Protección (protective trousers) have progressed from basic heavy-duty workwear to highly engineered technical apparel. Engineered to shield operators from chemical exposure, open flames, electrical arcs, and mechanical cuts, these garments play an essential role in corporate risk management and workforce safety.
The global demand for high-performance protective wear is driven by strict occupational safety directives, including the European Union's PPE Regulation (EU) 2016/425 and the United States OSHA guidelines. Safety managers recognize that lower body injuries account for a significant portion of lost-time occurrences in heavy manufacturing, petrochemical, and construction sectors. Consequently, selecting certified protective trousers is a key priority for safety officers and procurement departments worldwide.
Constructed from inherently flame-resistant (FR) fibers such as Nomex, Kevlar, or treated cotton blends. Compliance with EN ISO 11612 protects operators from convective heat, radiant exposure, and molten metal splashes.
Engineered with specialized multi-layer laminated coatings that prevent the permeation of hazardous chemicals, acids, and infectious biological fluids. Our designs offer splash resistance without sacrificing breathability.
Features integrated conductive carbon filaments woven into the fabric matrix. Certified to EN 1149-5 standards, these trousers dissipate static charges, preventing sparks in explosive ATEX environments.
Essential considerations for industrial safety buyers managing high-volume PPE sourcing campaigns.
Procuring protective apparel at an enterprise level requires balancing product performance, regulatory compliance, and total cost of ownership (TCO). Procurement teams must evaluate manufacturing partners based on their quality control processes, capacity consistency, and supply chain transparency. A secure, reliable partner is crucial in mitigating risks associated with defective safety gear.
Modern procurement operations prioritize suppliers who demonstrate rigorous traceability, from polymer selection to final garment inspection. In the safety sector, certifications must be verified by accredited third parties. Partnering with a manufacturer that possesses direct control over their raw material supply chains ensures consistent protective properties across production lots, shielding enterprises from potential liability issues.
Leveraging automated machinery and digital process management to deliver reliable protective products.
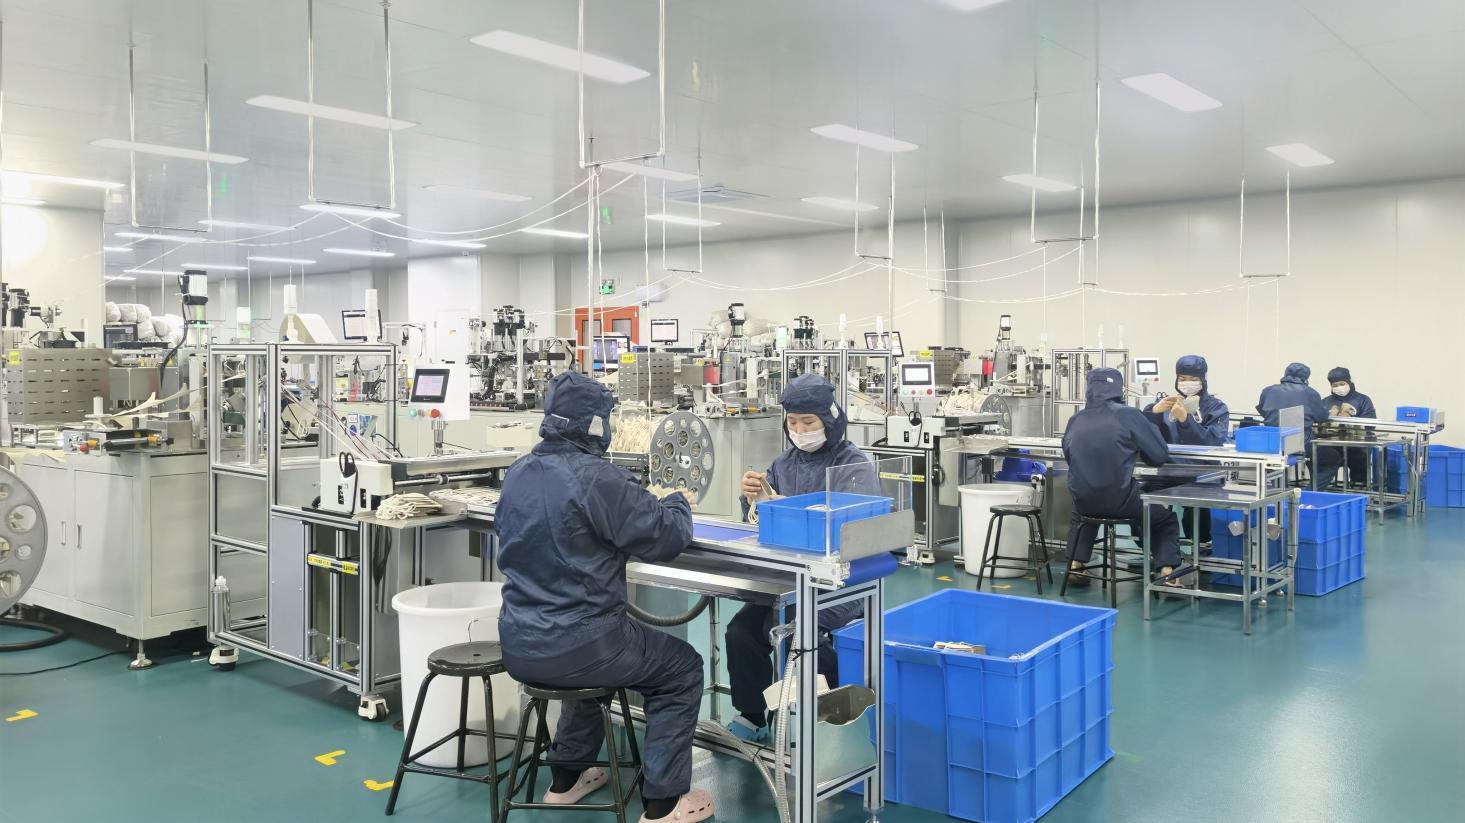
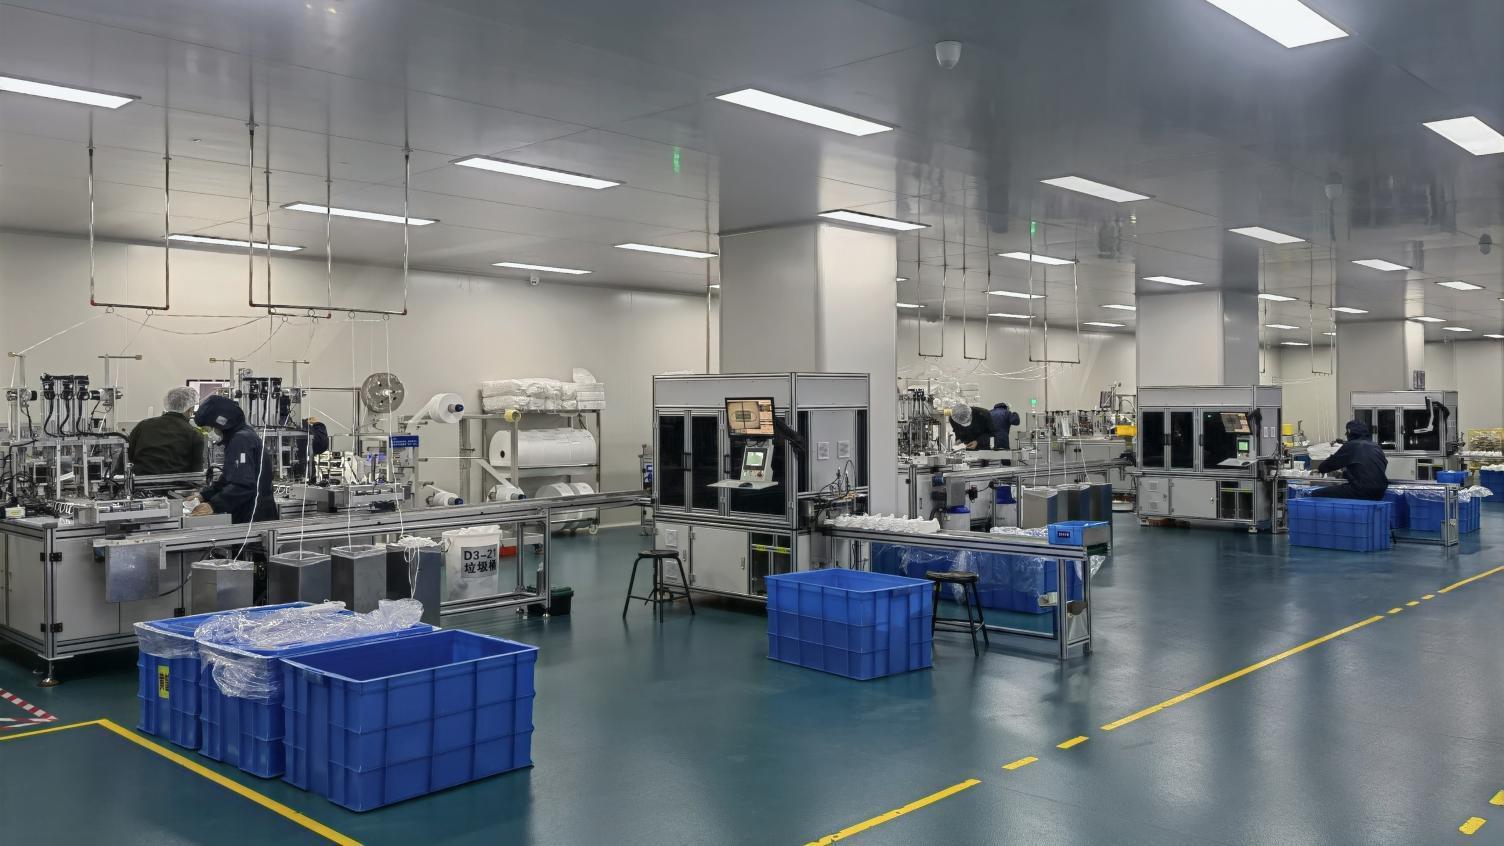
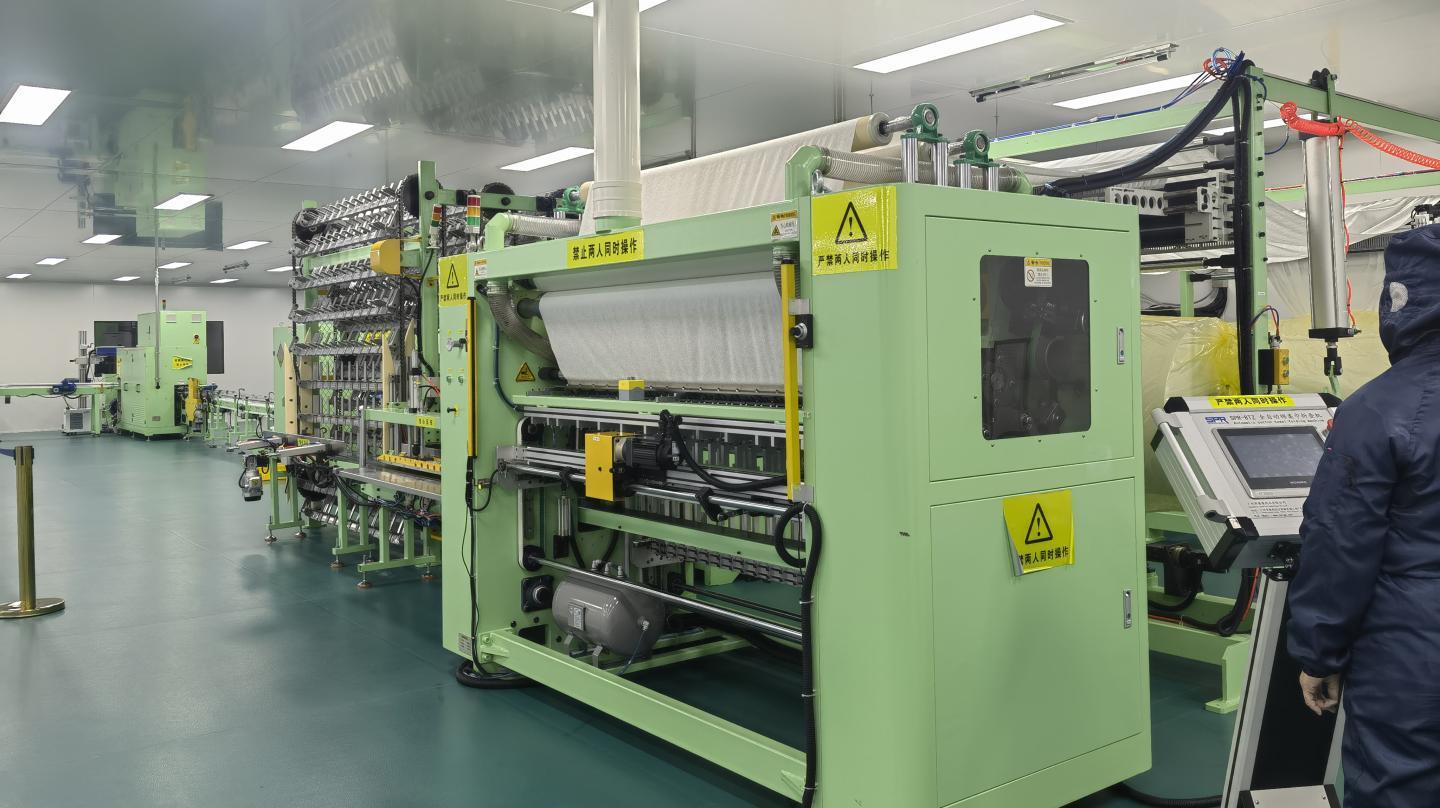
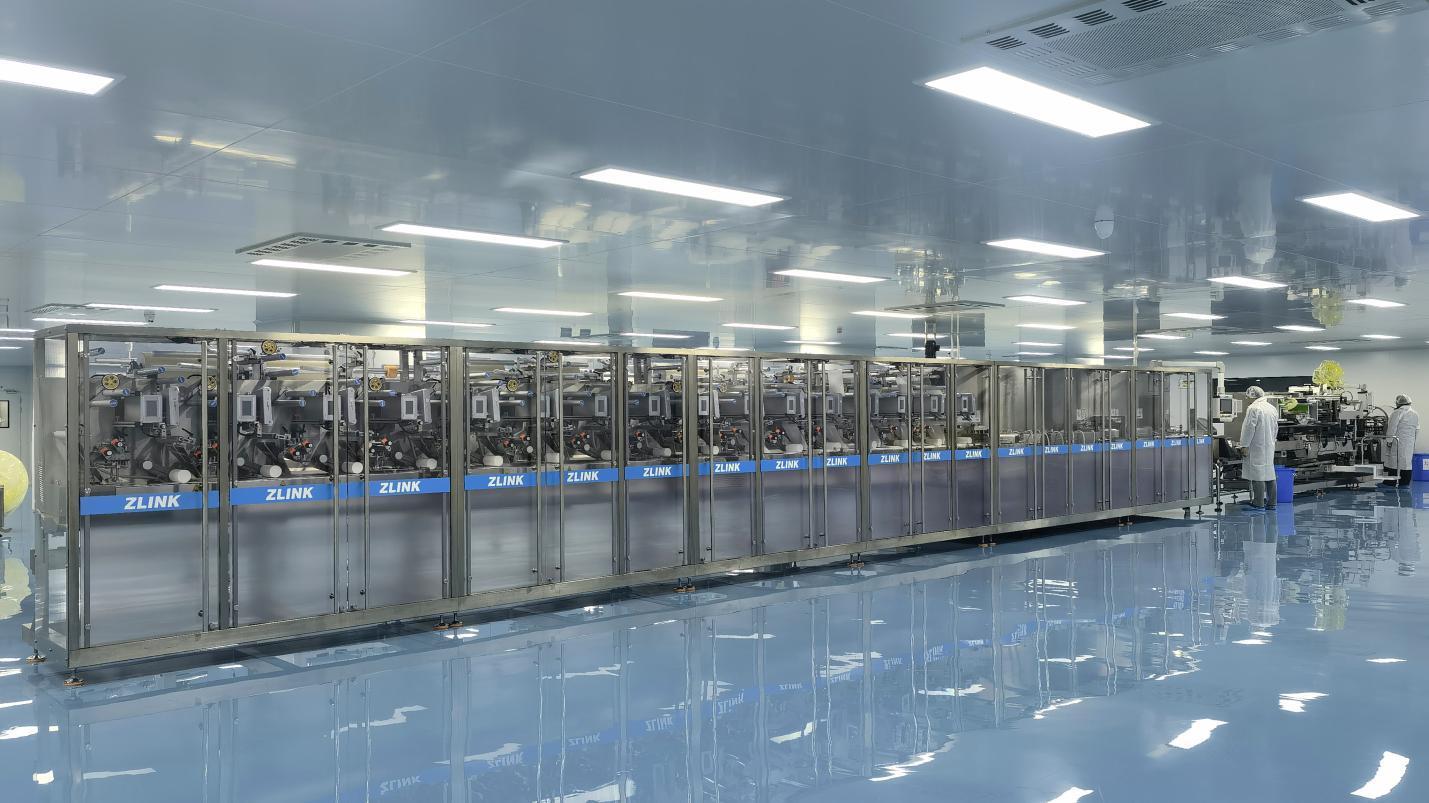
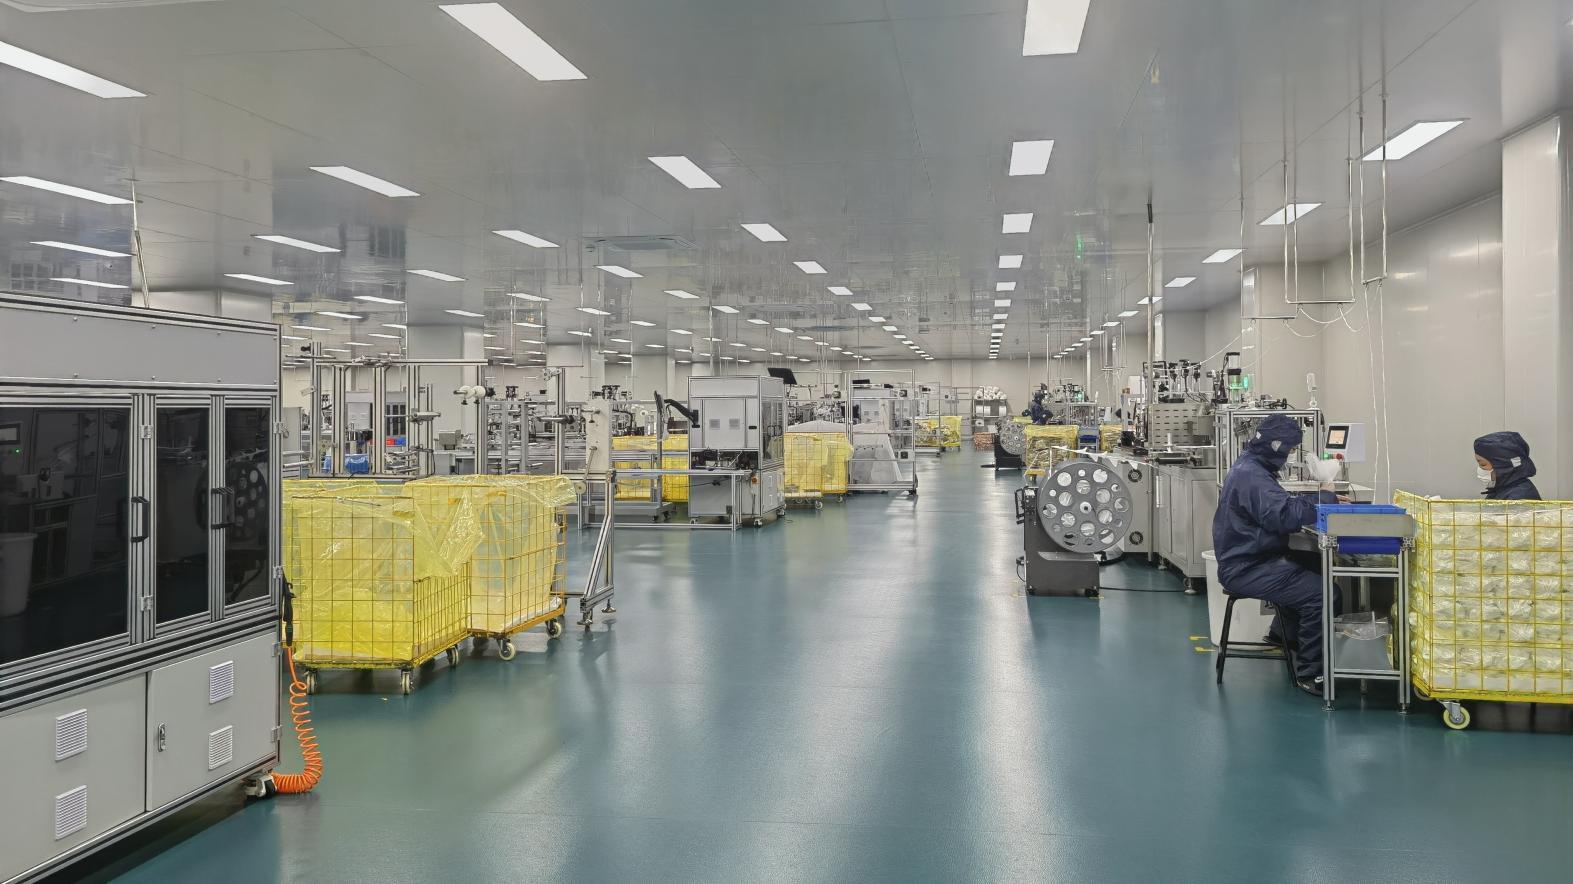
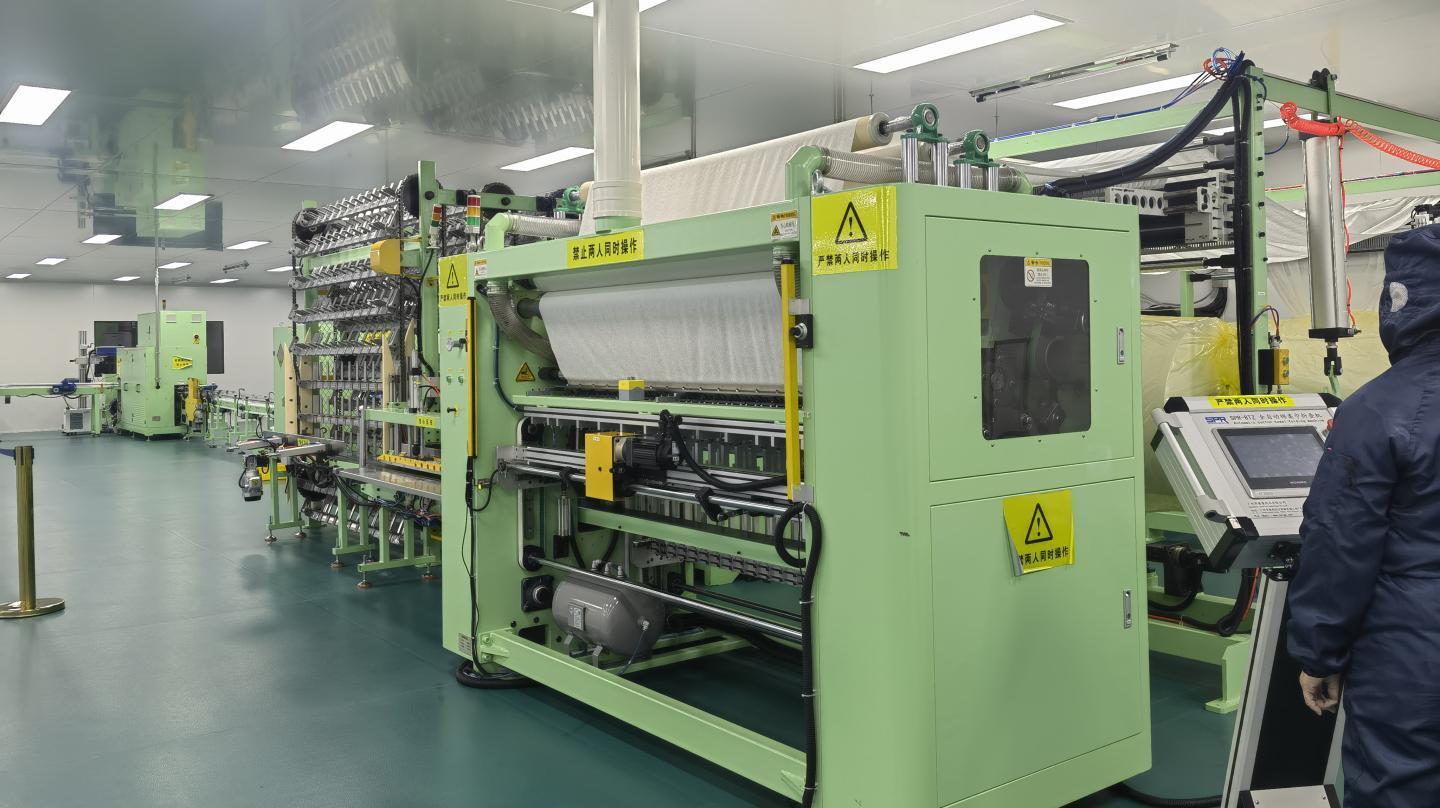
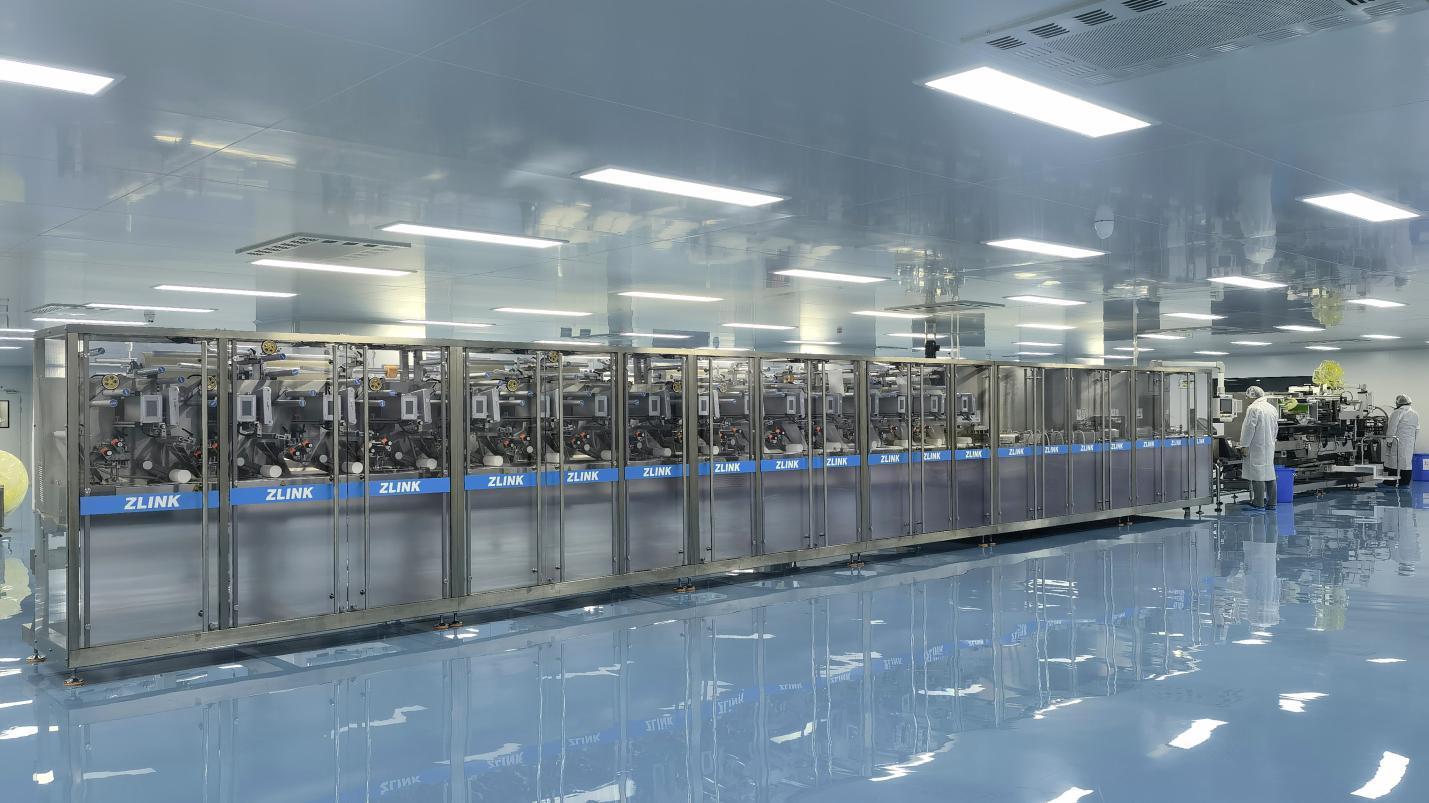
The manufacturing sector has moved beyond manual assembly lines. Leading industrial hubs in China utilize Factory 4.0 paradigms, integrating internet-of-things (IoT) diagnostics, automated laser cutters, ultrasonic welding machines, and real-time vision inspection systems. This level of automation ensures consistent build quality, tight dimensional tolerances, and optimal seam strength—key factors in protective garments.
By using automated systems for fabric handling and pattern cutting, manufacturers minimize human error, optimize material utilization, and shorten production cycles. The result is a resilient supply model capable of quickly scaling production in response to shifting global demands, while maintaining competitive costs and product quality.
Computerized manufacturing stations monitor temperature, pressure, and seam tension continuously. This data-driven approach maintains consistent protective performance throughout large-volume manufacturing runs.
Using advanced non-woven and composite textiles, our production lines match weight with protective strength, ensuring lightweight wearability that meets CE and FDA performance specifications.
Zhejiang DrSharpe Health Co., Ltd. is a professional manufacturer and global supplier specializing in disposable medical and healthcare products, especially high-quality face masks and protective solutions. With strong manufacturing capabilities, advanced production technology, and strict quality management, DrSharpe is committed to providing safe, reliable, and comfortable healthcare products for customers worldwide.
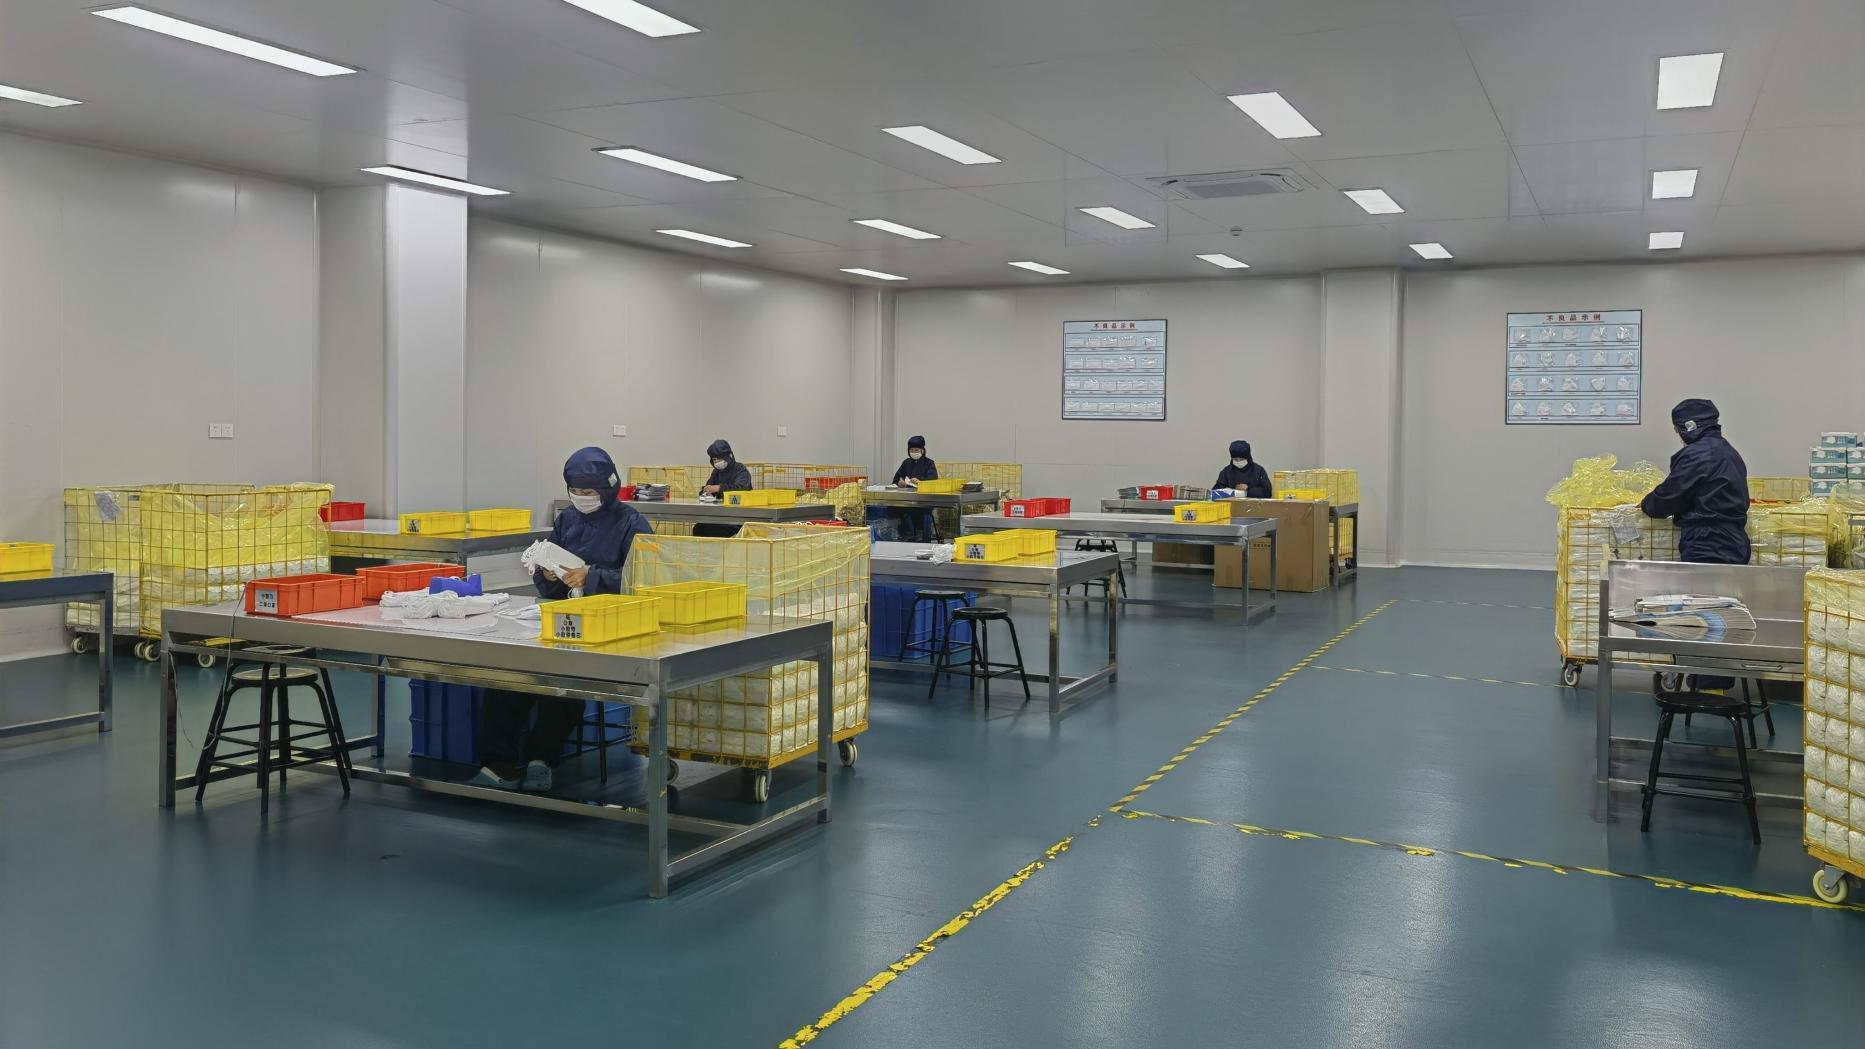
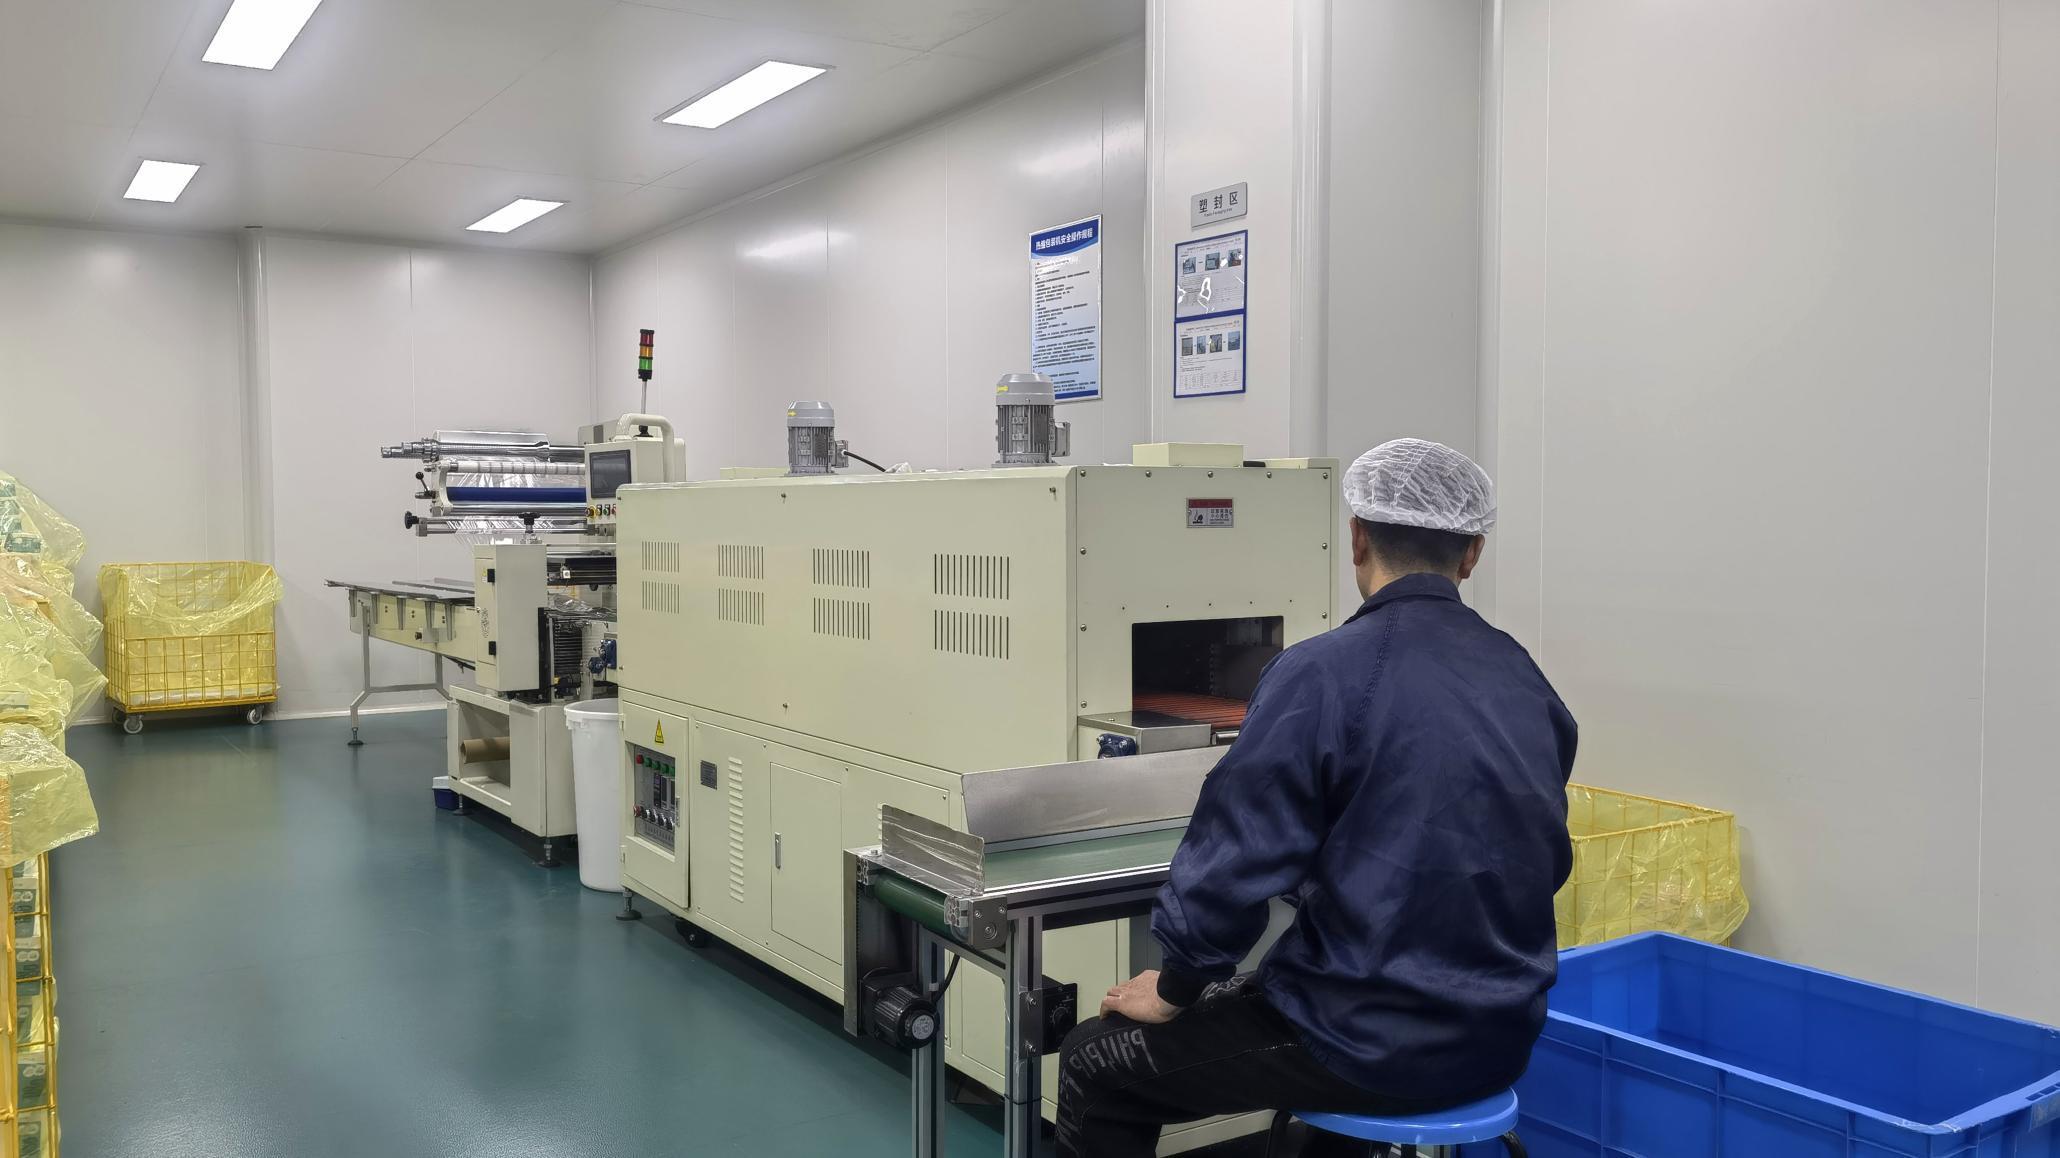
Our factory is equipped with 5 fully automatic mask production machines and 12 semi-automatic mask production machines, supported by an experienced production and service team. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to markets including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom.
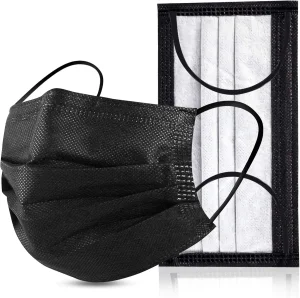
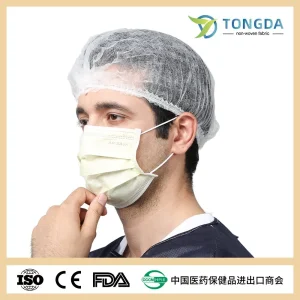
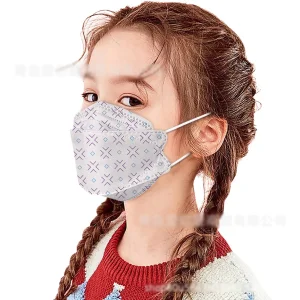
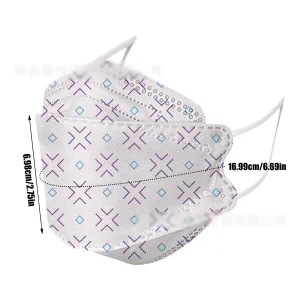
DrSharpe mainly provides disposable face masks and related healthcare products for medical, personal protection, and daily use applications. Using advanced filtration materials, our masks achieve up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE), offering excellent protection and wearing comfort. Our products comply with international standards and have obtained certifications including CE, US FDA, and US EUA.
Driven by innovation, quality, and customer satisfaction, Zhejiang DrSharpe Health Co., Ltd. continues to deliver trusted healthcare solutions and build long-term partnerships with customers around the world.
Ensuring safety compliance and hazard mitigation across diverse operational contexts.
High-risk infection zones require fluid-resistant garments that act as barriers against blood-borne pathogens and viral aerosols, keeping frontline medical personnel safe.
Environments handling corrosive reagents require protective trousers with acid splash resistance, safeguarding technicians from sudden spills.
Precision manufacturing requires lint-free, anti-static protective wear to shield delicate semiconductor wafers from dust and electrostatic discharge.
Expert insights regarding certifications, raw material selection, and procurement procedures.
Continuing our showcase of certified safety products designed for daily, medical, and specialized industrial settings.