DrSharpe Health
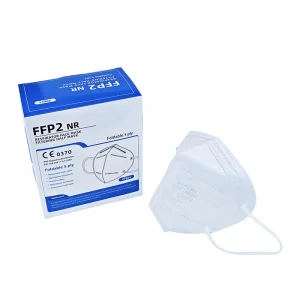
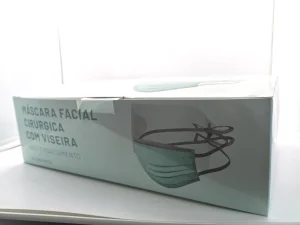
The Greater Melbourne area stands as one of Australia’s most vital hubs for infrastructure development, manufacturing, and healthcare services. With massive ongoing infrastructure programs such as the Victoria Big Build, the Metro Tunnel project, and the continuous expansion of manufacturing corridors in Dandenong, Campbellfield, and Laverton, the demand for premium-grade, reliable, and standardized respiratory protection has escalated. In heavy industrial settings, micro-particulates like crystalline silica present severe respiratory hazards, necessitating protective masks that consistently adhere to rigorous safety profiles.
Furthermore, Melbourne’s healthcare networks, spanning major organizations like Monash Health, Alfred Health, and Northern Health, rely heavily on uninterrupted supplies of high-grade surgical masks. The volatile Australian climate also presents periodic hazards, including bushfire smoke and pollen surges that trigger epidemic thunderstorm asthma. Therefore, having a direct pipeline to an agile, certified international manufacturing supplier ensures that local distributors, safety outfitters, and government procurement officers can stabilize their inventory, bypassing local supply deficits with absolute confidence in quality controls.
Our core filtration layers leverage advanced electrostatic electret charging, creating sub-micron physical and electrostatic barriers. This captures particles down to 0.3 microns without restricting airflow or driving up inhalation resistance.
Utilizing high-tensile, dermatologically tested spunbond fabrics that contact the wearer's skin. Engineered to prevent moisture buildup and avoid micro-abrasions, crucial for long-duration shifts in dry Australian conditions.
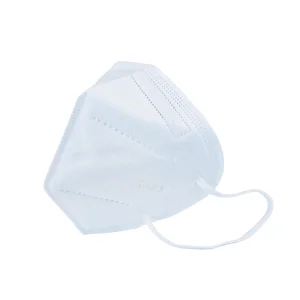
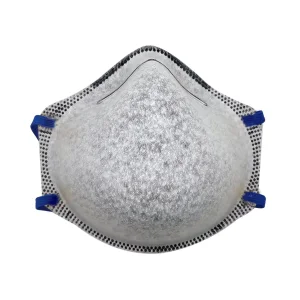
Deploying advanced 3D contour mapping across our particulate respirators to ensure flat-fold and cup-shape profiles conform securely to diverse facial features, substantially reducing peripheral leakage risks.
Our research and development pipeline is actively moving toward high-efficiency, biodegradable non-woven polymers derived from polylactic acid (PLA). Recognizing the global push for sustainability—and Victoria's Circular Economy policies—our technical roadmap prioritizes eco-conscious packaging and degradable filter layers that maintain a stable 5-year shelf life under warehouse conditions while drastically reducing the long-term ecological impact of disposable safety apparel.
Enterprise procurement in the industrial, civil, and medical spaces demands more than off-the-shelf catalog ordering. Our supply architecture is designed for institutional buyers, safety supply distributors, and government divisions across Victoria that require highly reliable batch-to-batch consistency. We offer structured Vendor-Managed Inventory (VMI) frameworks, custom safety branding options, and container-load direct logistics targeting critical Melbourne ports.
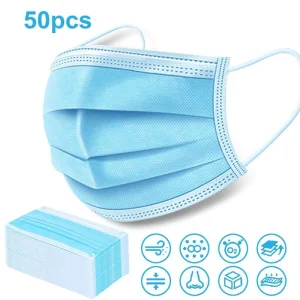
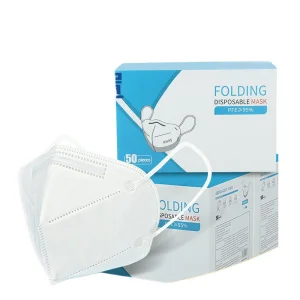
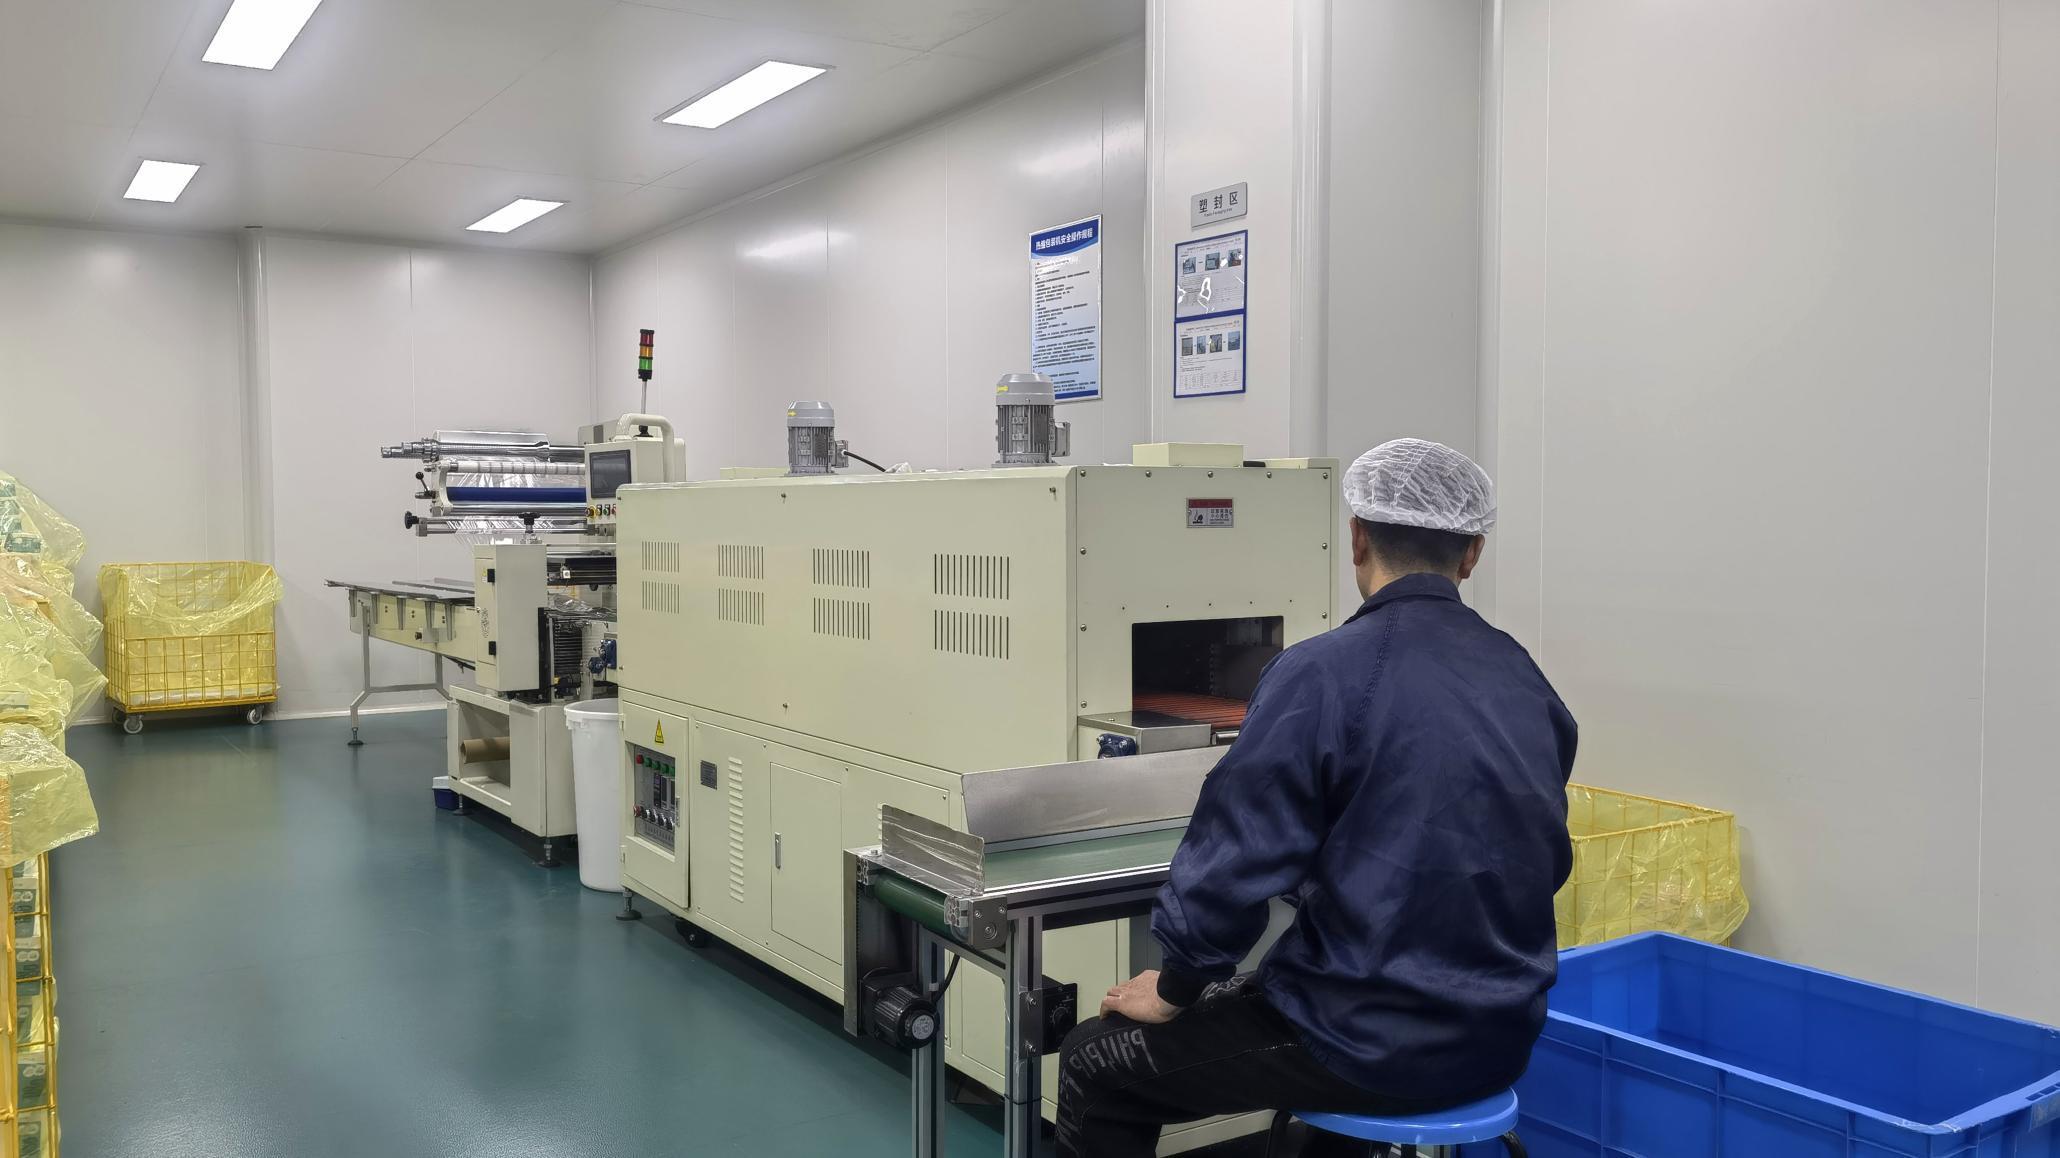
Whether supplying high-filtration civilian-grade protective masks for retail networks, anti-dust respirators for heavy construction sites in the Docklands, or sterile surgical-grade options for Victorian clinical environments, our products feature custom packaging configurations, barcodes mapped to Australian warehouse systems, and protective moisture-proof outer cartons optimized for local container transit.
Entering the Australian safety ecosystem requires strict compliance. For medical and hospital use cases, face masks must adhere to the Therapeutic Goods Administration (TGA) frameworks and align with testing standards such as AS 4381:2015 (Single-use face masks for use in health care). For industrial dust, silica, and mist exposure, products must align with AS/NZS 1716:2012 (Respiratory protective devices).
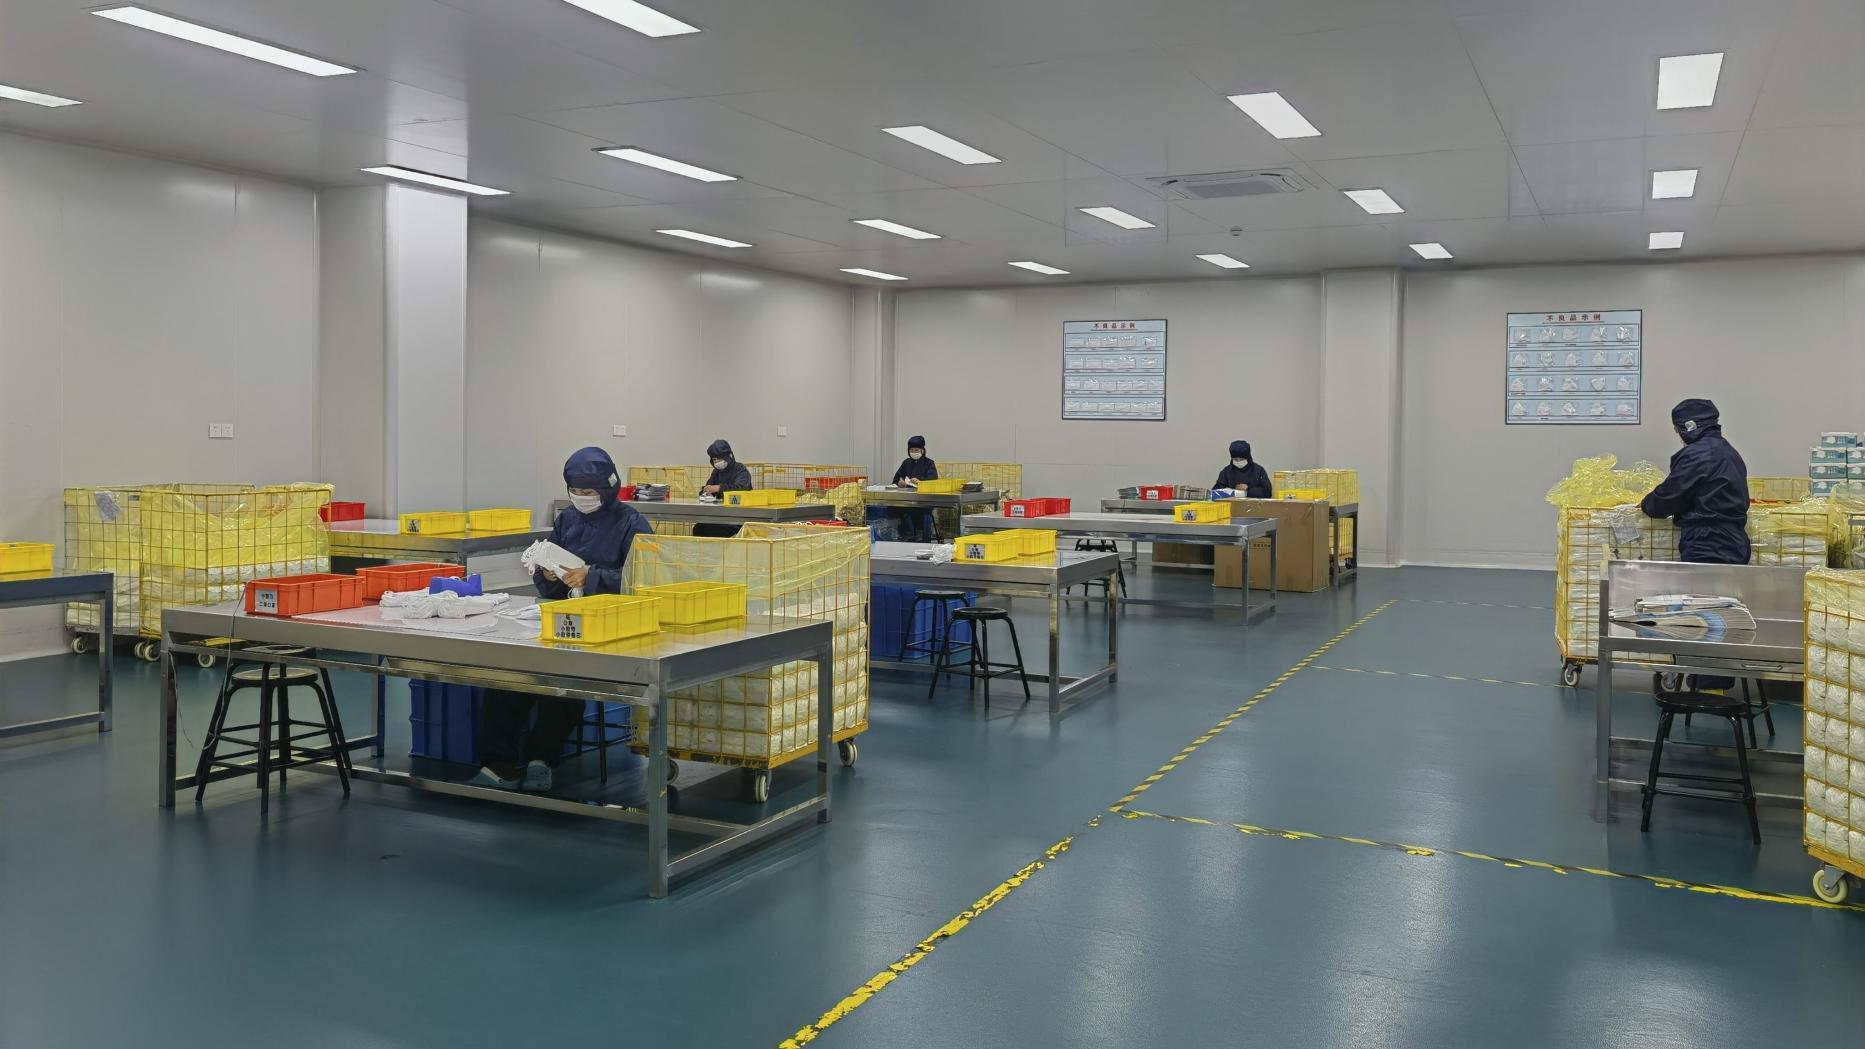
Our manufacturing plant systematically executes quality controls to ensure high ratings. In our testing protocols, we employ certified laboratory instruments to assess differential pressure (Delta P), ensuring maximum breathability alongside fluid resistance barriers. Our masks are certified to international equivalents including CE, US FDA, and US EUA, giving Melbourne safety managers peace of mind regarding the authenticity and regulatory robustness of every batch shipped.
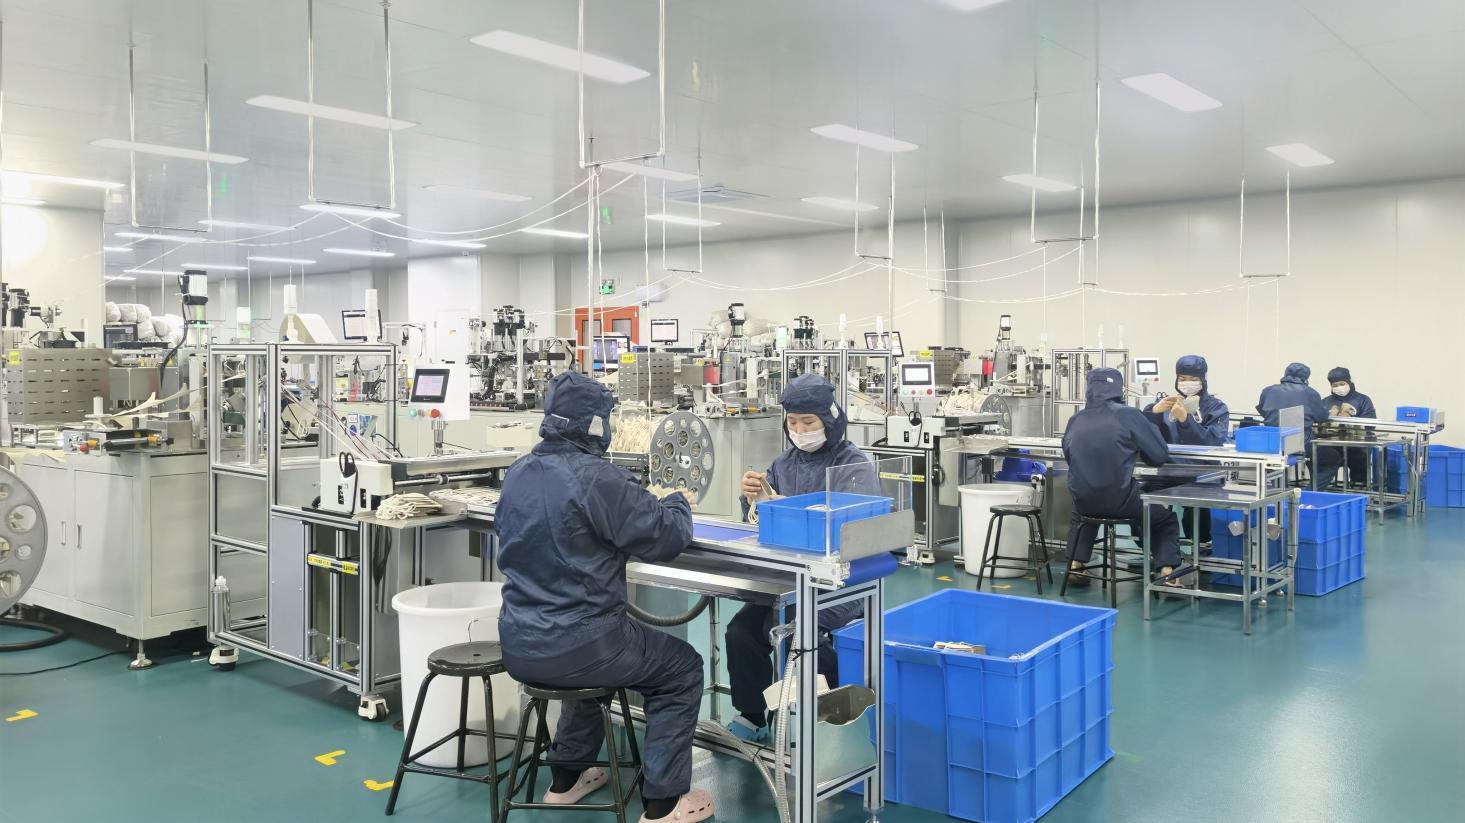
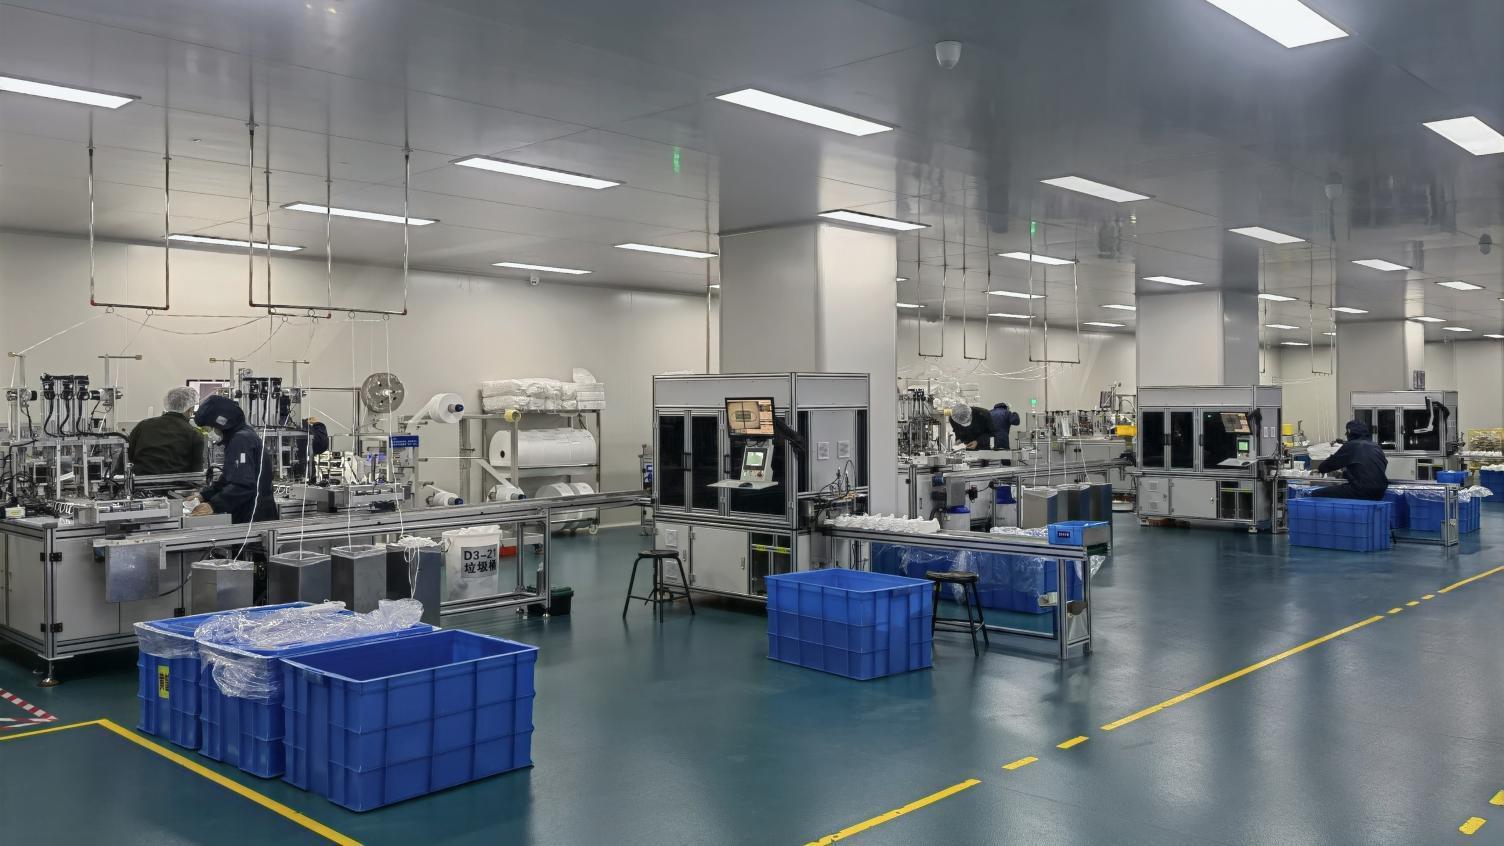
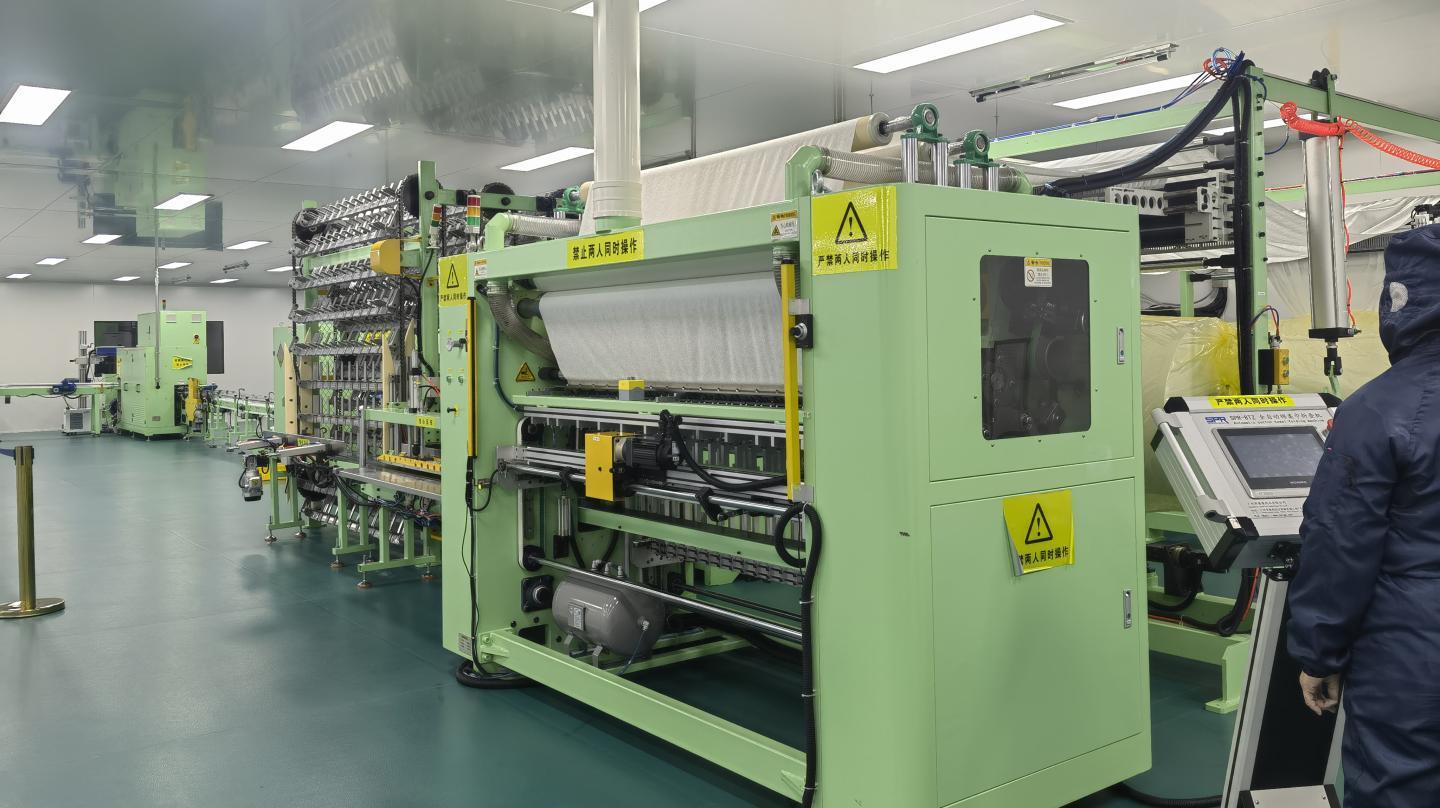
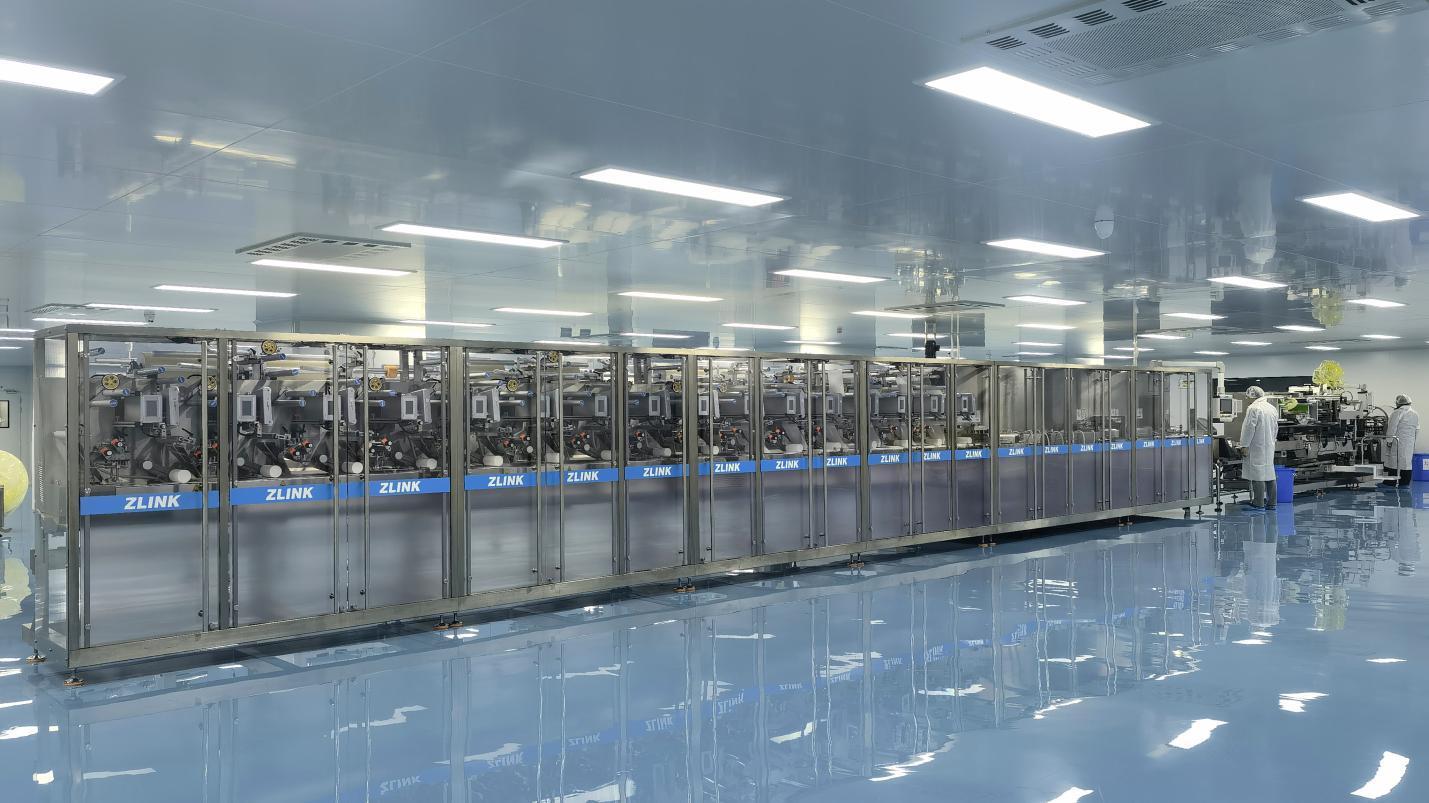
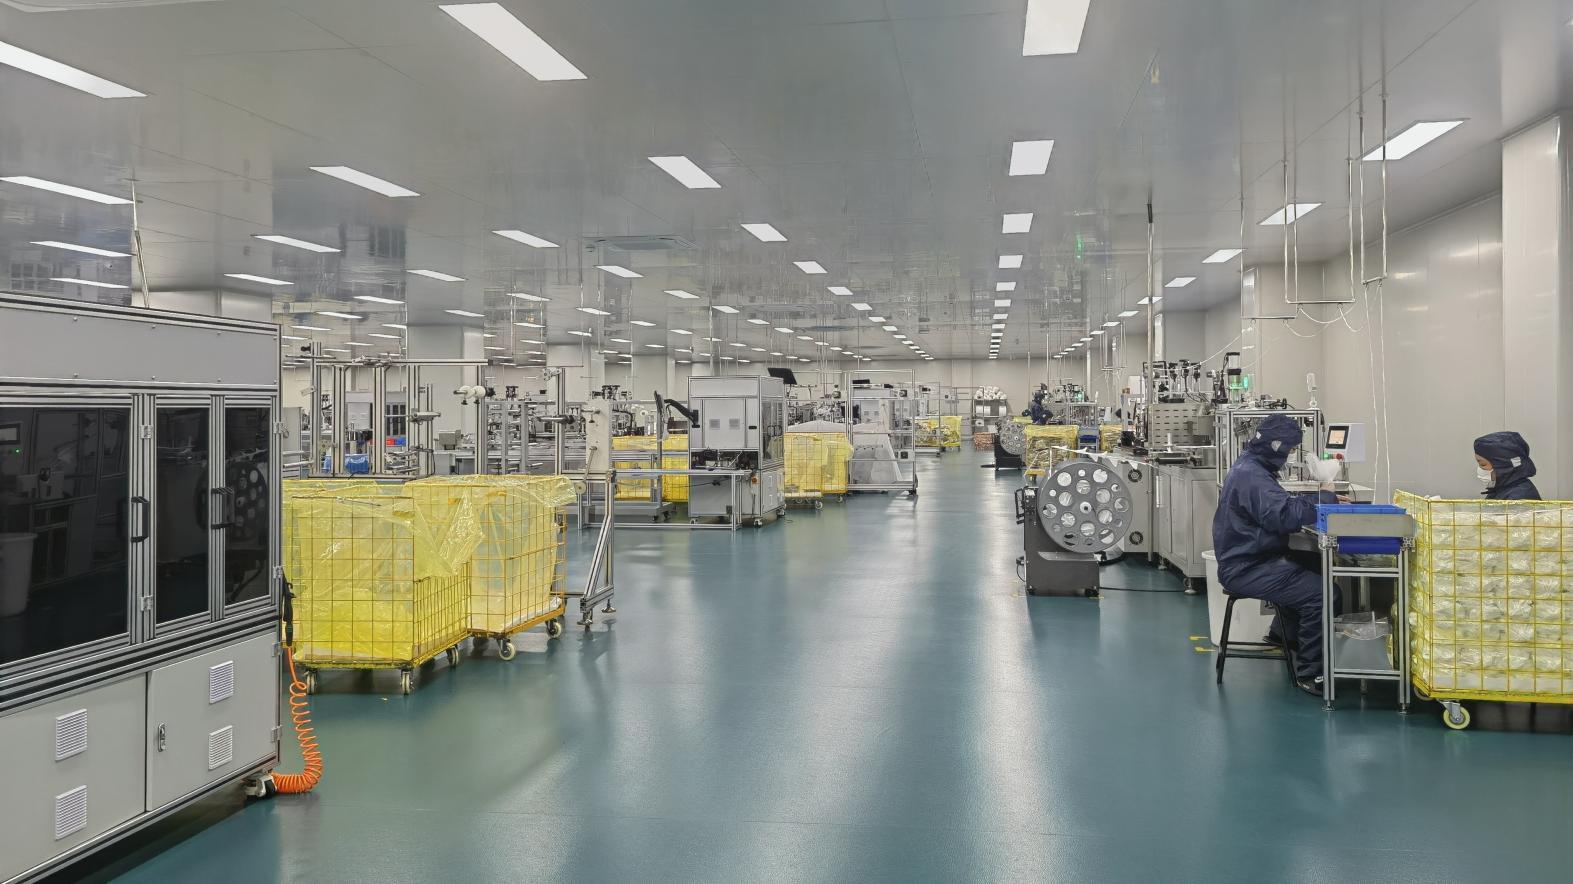
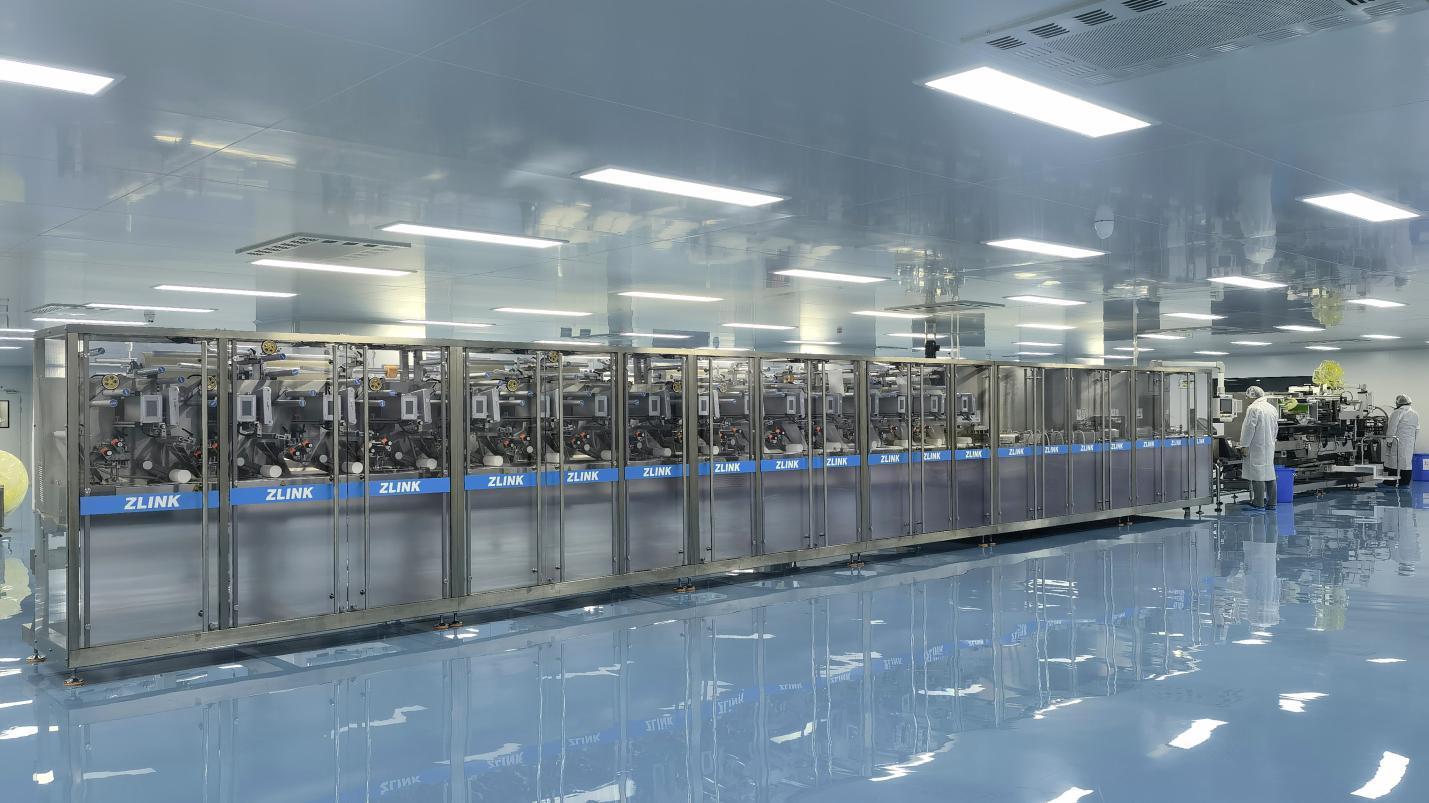
Located in the heart of China's advanced medical manufacturing zone, Zhejiang DrSharpe Health Co., Ltd. operates a high-efficiency facility equipped with 5 fully automatic and 12 semi-automatic production lines. By transitioning to fully computerized automated optical inspection (AOI) systems and ultrasonic welding structures, we significantly reduce human error rates, maintaining tight control over earloop attachment pull strength, nose bridge positioning, and pleating accuracy.
Our direct access to world-class non-woven polymer and melt-blown raw material manufacturers in eastern China guarantees production stability even during unpredictable global demand spikes. Leveraging our proximity to major shipping hubs in Ningbo and Shanghai, we facilitate seamless sea freight corridors to the Port of Melbourne, achieving predictable transit timelines, lower landed costs, and resilient supply pipelines for enterprise accounts.
Zhejiang DrSharpe Health Co., Ltd. is a professional manufacturer and global supplier specializing in disposable medical and healthcare products, especially high-quality face masks and protective solutions. With strong manufacturing capabilities, advanced production technology, and strict quality management, DrSharpe is committed to providing safe, reliable, and comfortable healthcare products for customers worldwide.
Our factory is equipped with 5 fully automatic mask production machines and 12 semi-automatic mask production machines, supported by an experienced production and service team. From raw material selection to final packaging, we strictly control every production process to ensure stable quality and reliable supply. Our products are widely exported to markets including the United States, Europe, Japan, Mexico, Germany, and the United Kingdom—and now actively serving major safety partners across the Greater Melbourne area.
DrSharpe mainly provides disposable face masks and related healthcare products for medical, personal protection, and daily use applications. Using advanced filtration materials, our masks achieve up to 99% Bacterial Filtration Efficiency (BFE) and 99% Particle Filtration Efficiency (PFE), offering excellent protection and wearing comfort. Our products comply with international standards and have obtained certifications including CE, US FDA, and US EUA.
Partner with a trusted, certified manufacturer to avoid stock shortages and protect your workforce with high-quality respiratory protection.
Send Inquiry Now